Ultrasonic Wire Welding Machine for 0.75–20 mm² Copper Splices WM-711
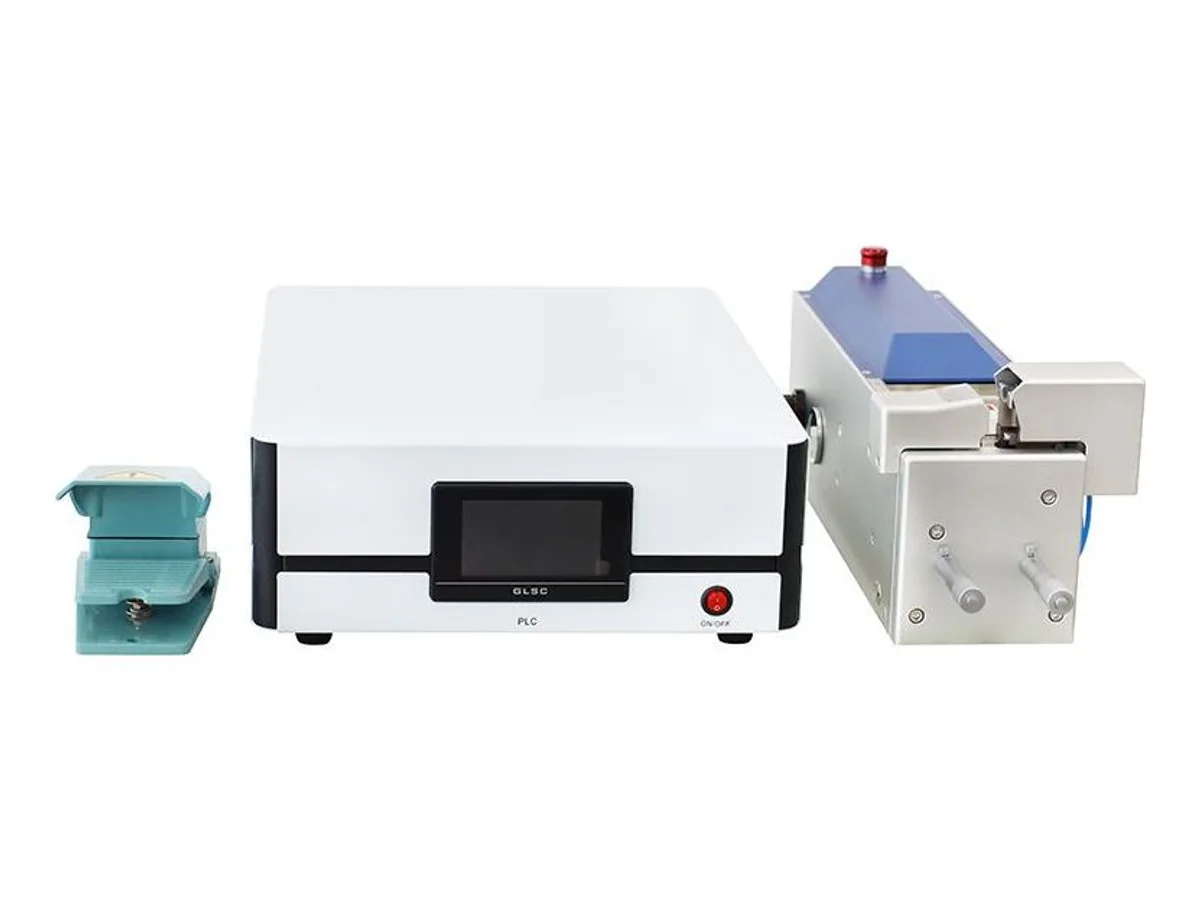
The WM-711 welds stranded copper wires into solid metallurgical splices by 20 kHz ultrasonic vibration — no solder, no flux, no splice bands. Its 3,000 W generator covers gathered cross-sections from 0.75 to 20 mm², the joint class used in automotive, EV and appliance harness splicing. Frequency tracking is fully automatic, so changing the welding horn needs no manual retuning, and the English touchscreen shows current, power, time and amplitude live for every weld. A foot pedal starts the semi-automatic cycle while the operator holds the wire gather in place.
Specifications
| Function | Ultrasonic metal welding of stranded copper wire splices |
|---|---|
| Power | 3,000 W |
| Working frequency | 20 kHz |
| Welding cross-section range | 0.75 – 20 mm² (total gathered section) |
| Operation | Semi-automatic — foot pedal start |
| Frequency tracking | Fully automatic, no retuning after horn change |
| Display | English touchscreen with live current, power, time and amplitude |
| Weld head guidance | Precision linear guides |
| Protections | Frequency and overcurrent protection, adjustable during welding |
| Generator stability | Stable output under supply-voltage fluctuation |
| Dimensions | 480 × 420 × 180 mm |
| HS Code | 8515.80 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Solid-state metallurgical bond in one press — replaces solder pots, flux fumes and crimp-band stock for wire-to-wire splices up to 20 mm² total
- Automatic frequency tracking removes manual frequency retuning after horn changes; verify the tooling setup and weld quality before restarting production
- Live readout of current, power, time and amplitude gives every splice a numeric signature for process audits
- Generator output regulation helps manage supply variation; verify weld consistency under the actual operating conditions
What it processes
- Multi-wire splice joints in automotive, EV and motorcycle wiring harnesses
- Copper gather welding in appliance looms and motor lead assemblies
- Replacing solder splices where flux residue or heat damage is unacceptable
Suited for: wire-to-wire copper splices with a total gathered section of 0.75–20 mm² — the splice work inside automotive, EV and appliance harnesses where solder and crimp bands cost time and consumables. Not suited for: terminal attachment — for that, pick the WM-713 ultrasonic terminal welding machine, the wire-to-terminal counterpart of this splicer for sections under 30 mm² — nor soldering or tinning, which live with the other wire soldering and welding machines in this category.
Send 2–3 meters of each wire in your splice combination and we weld your actual joints on video — including a peel-back of the weld nugget — before you commit. Splice quality is a core requirement on an EV wire harness line.
Engineering knowledge
Choose and troubleshoot this process
- How to Choose an Ultrasonic Wire Welding MachineChoose ultrasonic wire welding equipment by conductor material, gathered cross-section, splice geometry, weld power, tooling, recipe control and acceptance testing.
- Ultrasonic Wire Welding Defects: Causes and Corrective ActionsTroubleshoot weak wire splices, cut strands, excessive flash, incomplete bonding, unstable weld energy, tool marking and conductor contamination.
- How to Choose a Wire Twisting and Tinning MachineChoose wire twisting and tinning equipment by conductor construction, strip condition, tinning specification, flux control, finished-end geometry and automation level.
WM-711 — common questions
What splice sizes can the WM-711 weld?
Any wire combination whose total gathered cross-section falls between 0.75 and 20 mm² — for example several 0.5 mm² signal wires into a 2 mm² feed, or two 8 mm² power leads. If your joints run larger, a 32 mm² class version is available on request.
Does changing the welding horn require recalibration?
Frequency tracking is fully automatic, so the generator finds resonance without manual frequency adjustment after a horn change. This does not replace verification of tooling alignment, process settings and weld quality after a horn or anvil change. Frequency and overcurrent protection limits are adjustable during welding.
What is it not designed to do?
It welds copper to copper — it does not solder, tin or attach terminals, and plastic parts need a plastic welder instead. For tinning and solder-based joining, browse the other machines in our wire soldering and welding category.
Related machines in Tinning, Soldering & Welding
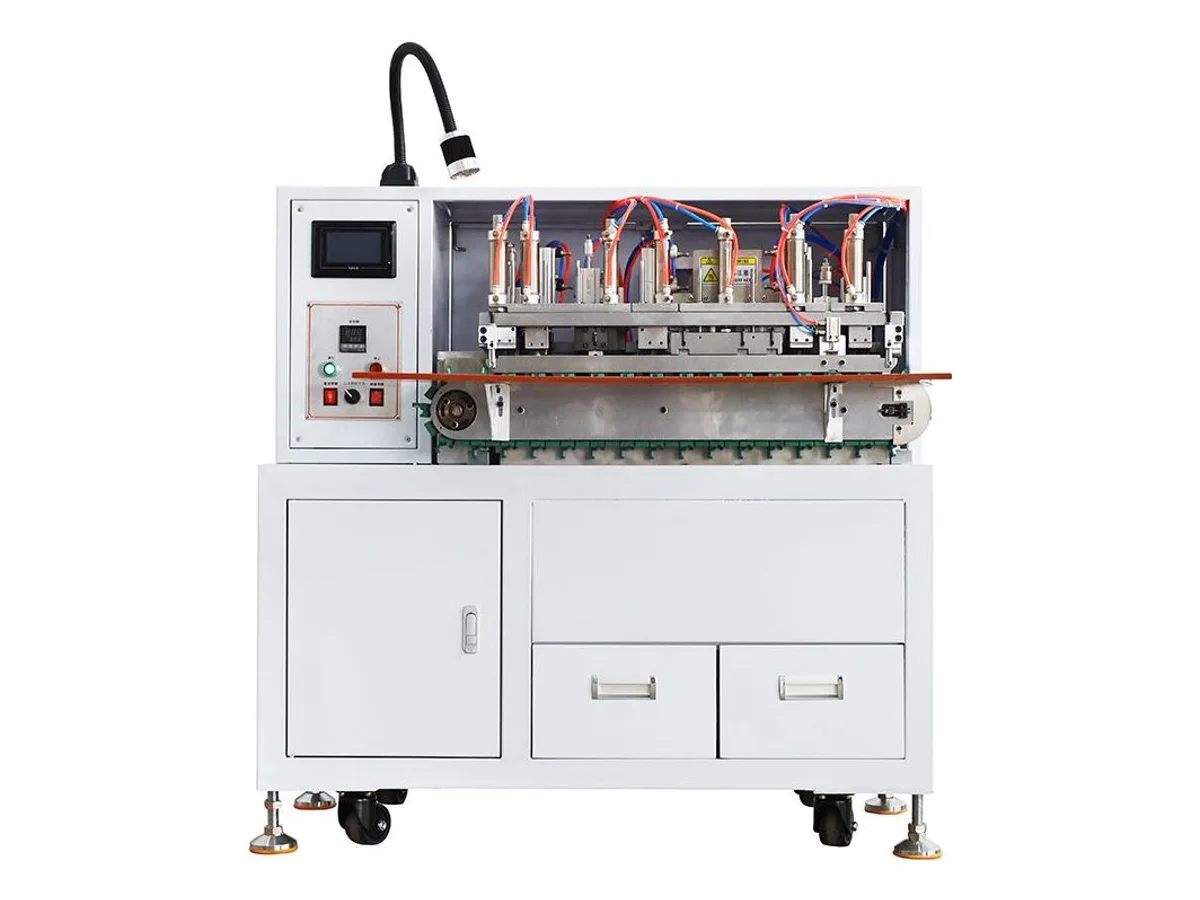
Automatic 3-Core Cable Cutting Stripping Twisting and Tinning Machine
Model WM-4710T
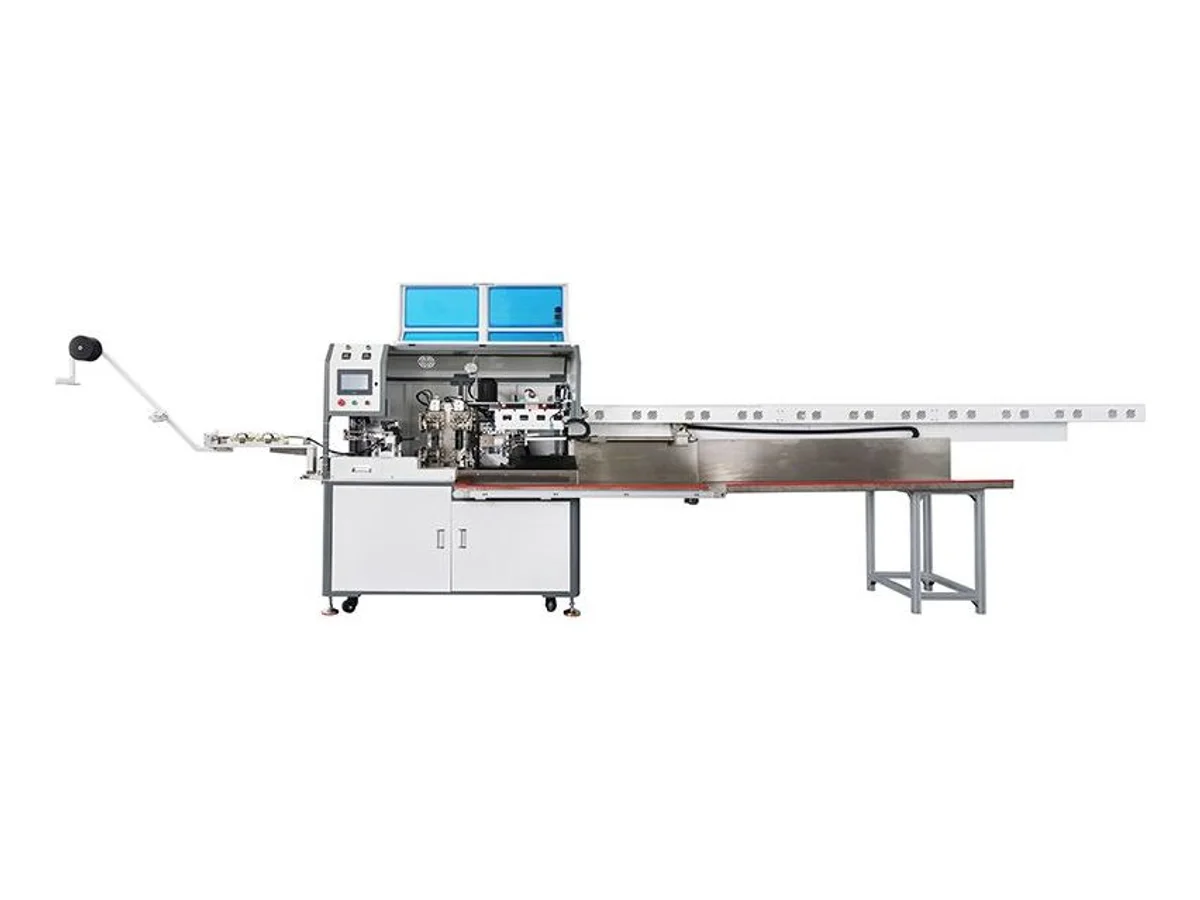
Automatic Multicore Cable Cutting Stripping and Two-End Tinning Machine
Model WM-4706S
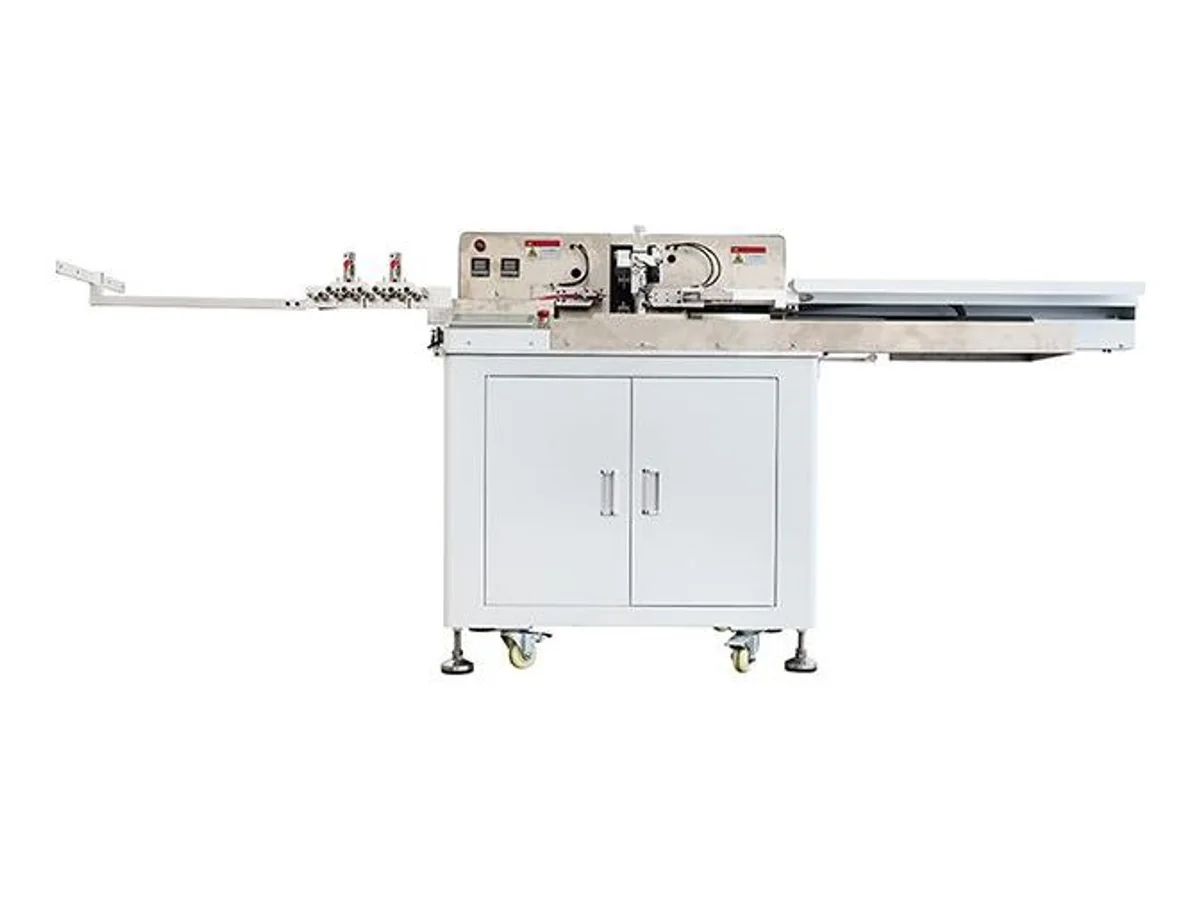
Automatic Multiple-Wire Stripping Twisting and Tinning Machine for 18–28 AWG
Model WM-4706W