Selection guide
Wire Harness Manufacturing: From Drawing to Final Test
Plan wire harness production from the drawing: cutting, stripping, seals, crimping, housing insertion, taping and final electrical checks.
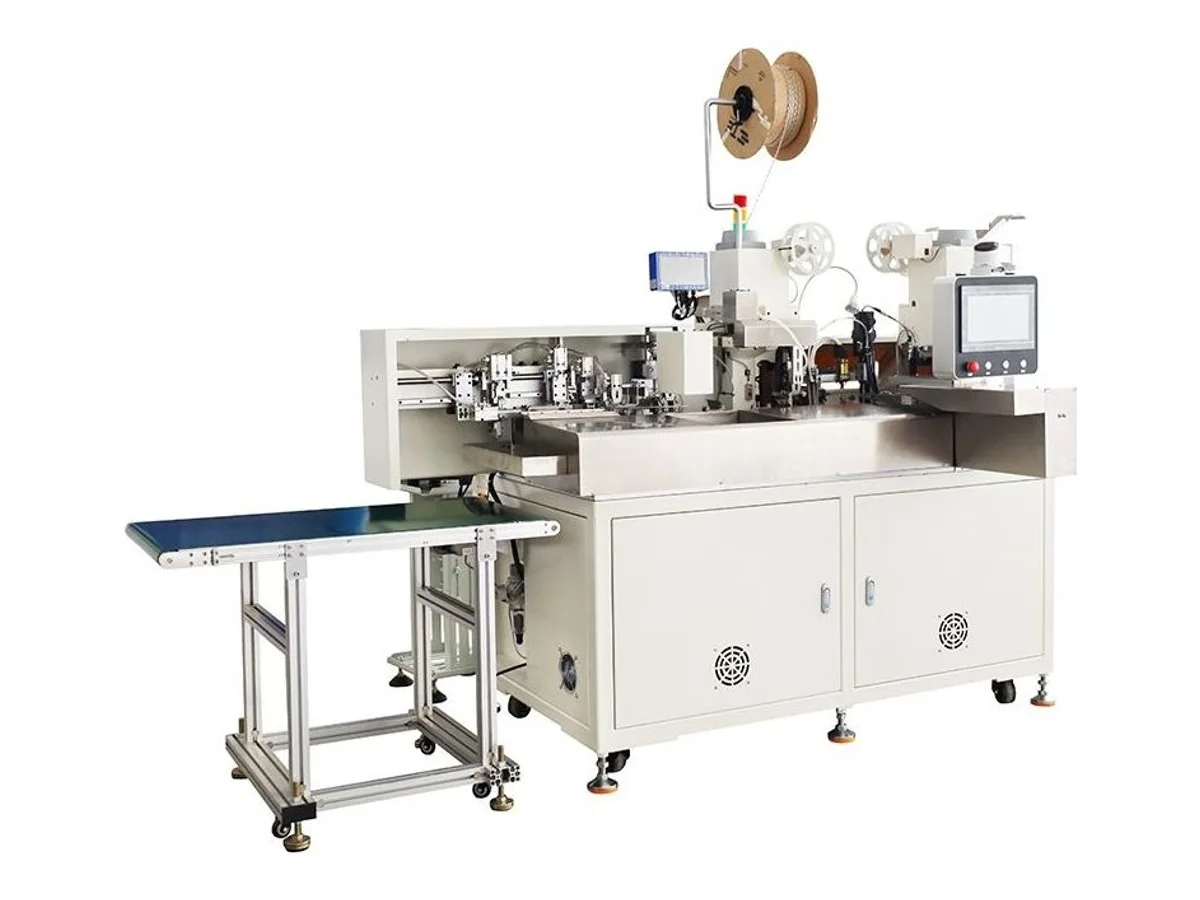
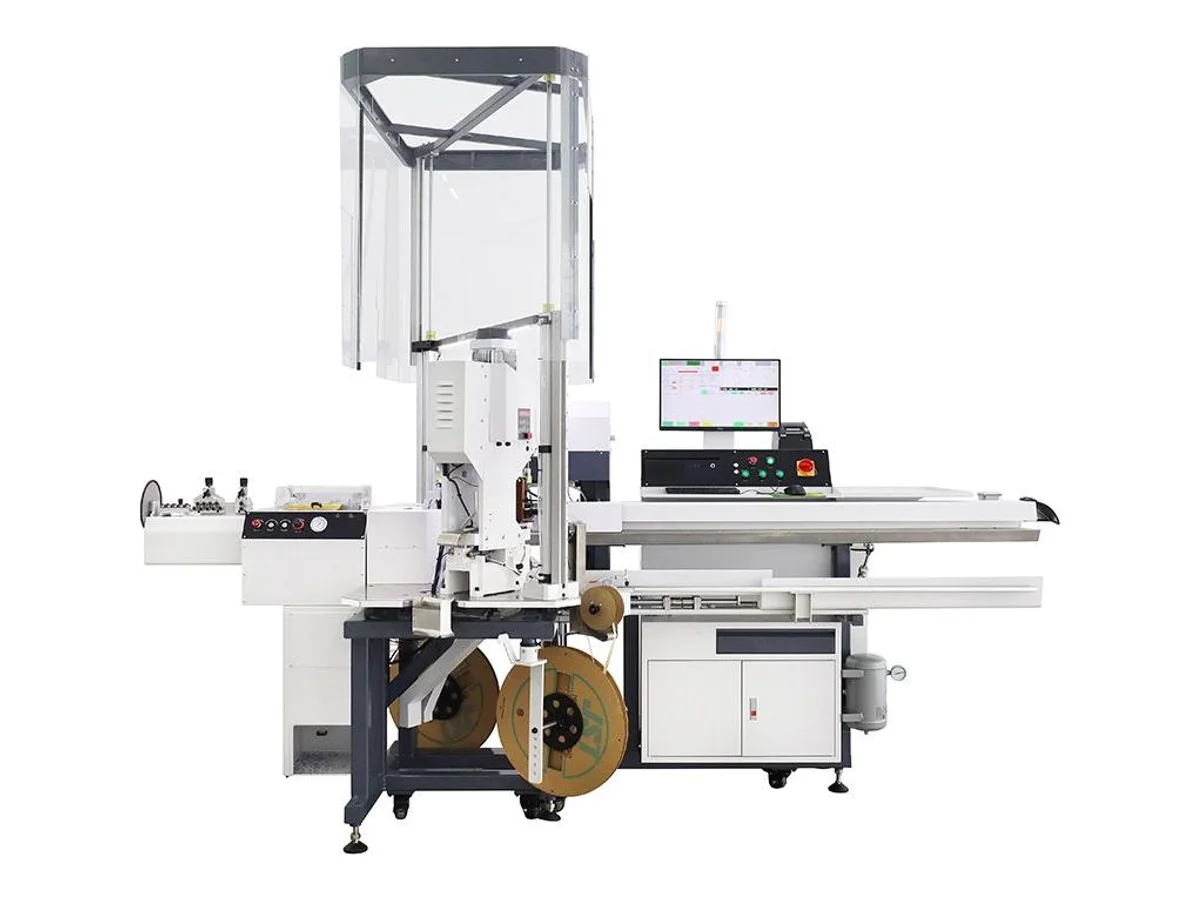
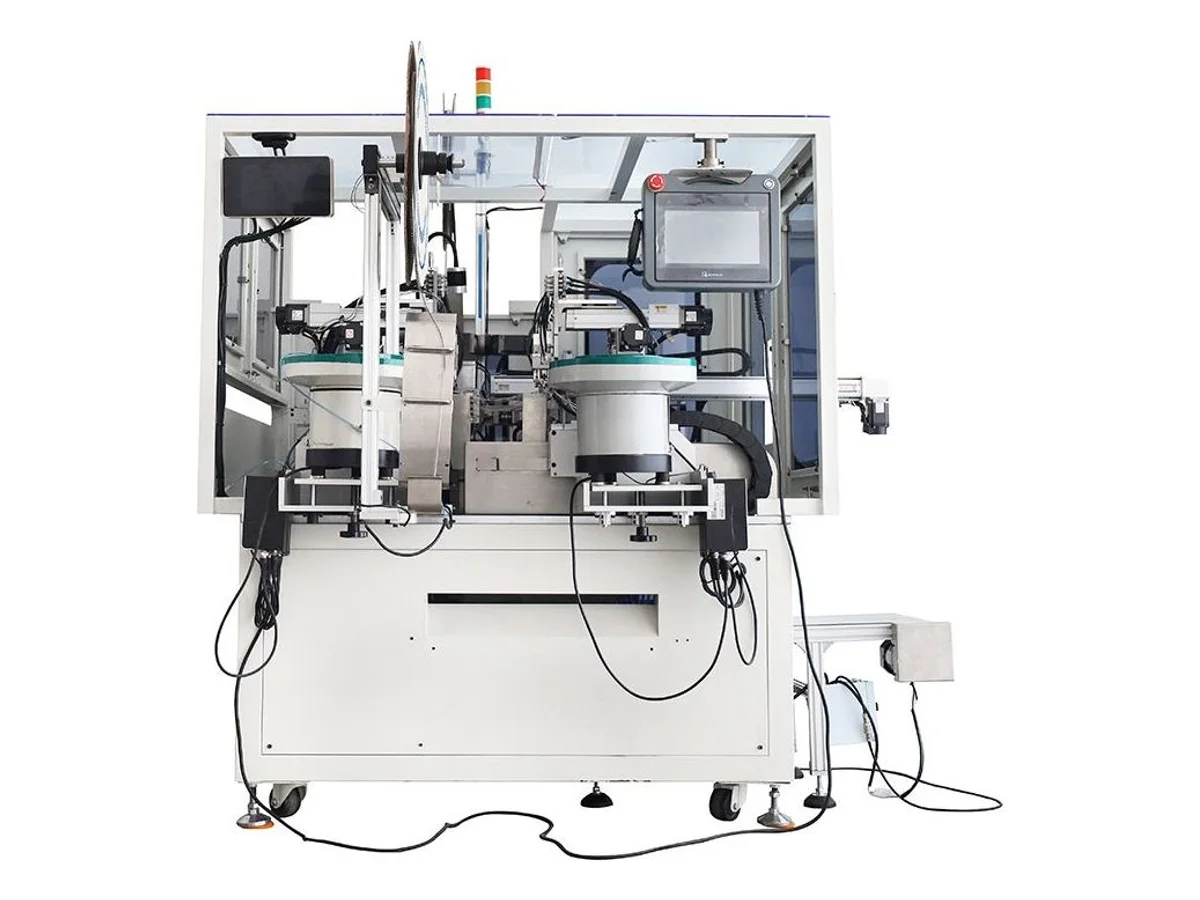
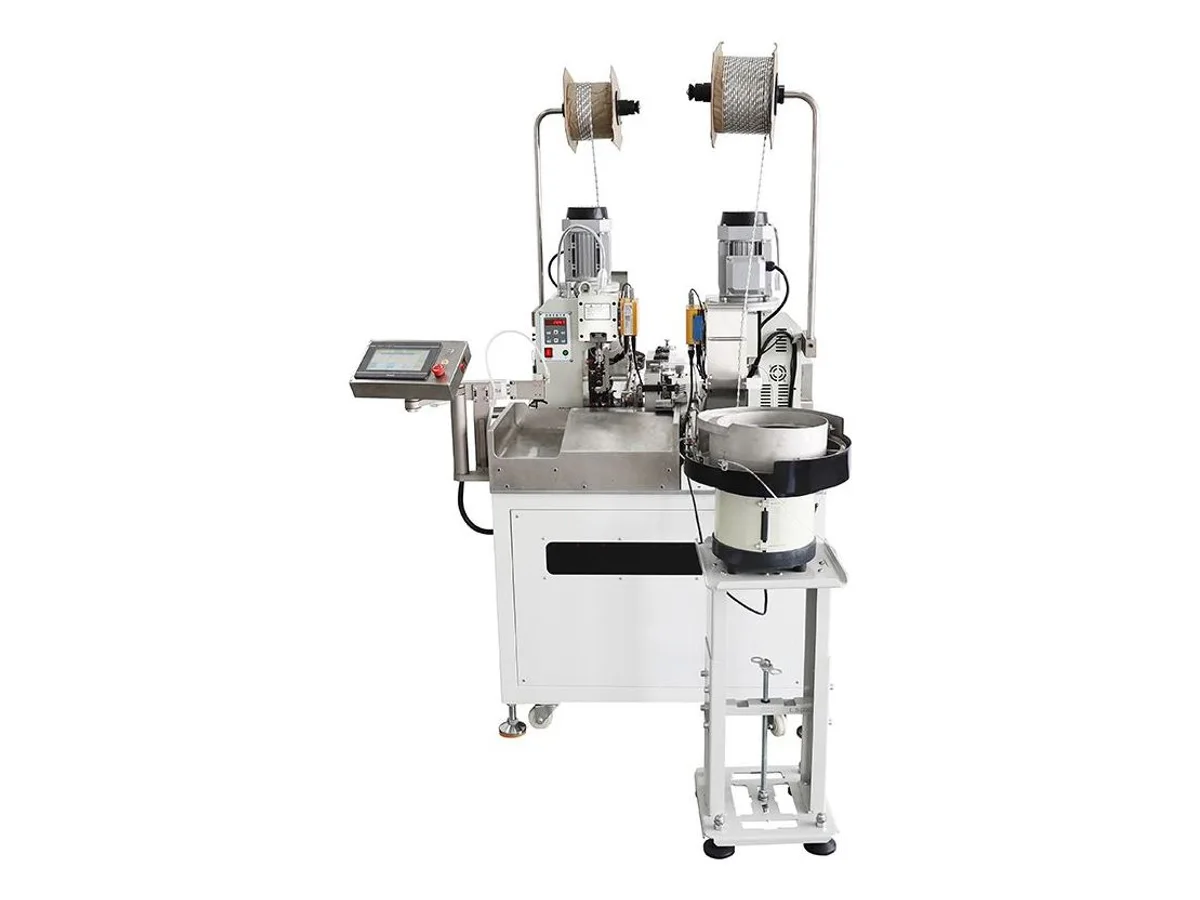
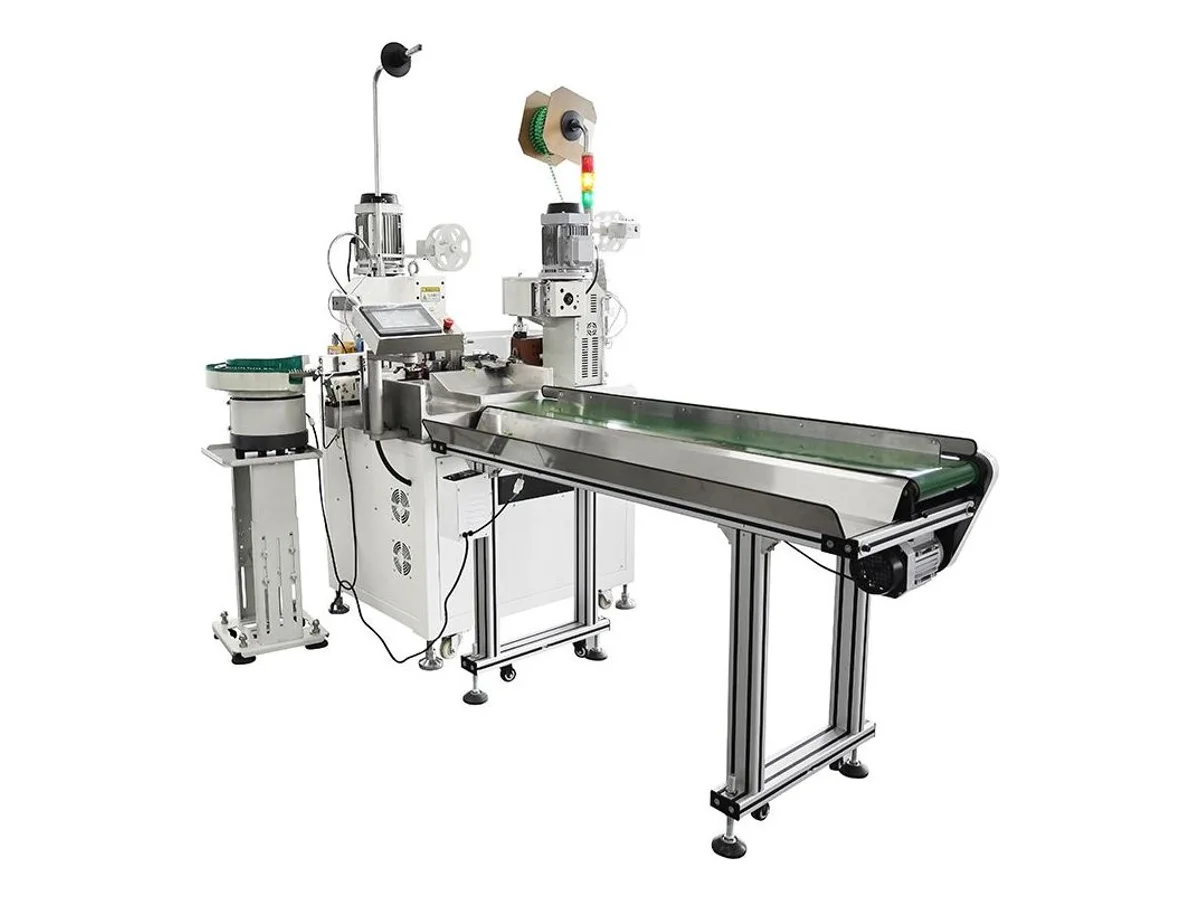
Read engineering guide →Terminal crimping machines from a 2-ton bench press to a 35-ton servo lug crimper: fully automatic double-end lines at up to 4,800 pcs/h, ribbon-cable crimpers placing 15,000 terminals per hour, ferrule and bootlace machines, housing insertion and rubber seal lines, hydraulic lug crimpers for EV cable to 120 mm², and portable crimping tools. Applicator compatibility depends on the press and terminal; see the parts page for tooling. Copper-band splicing presses make mechanical wire joints without solder. Send your terminal strip and wire and we crimp them on video, with crimp-height measurements, before you order.
These machines include this operation as part of a wider process. Open the product page to check the complete working range and configuration.
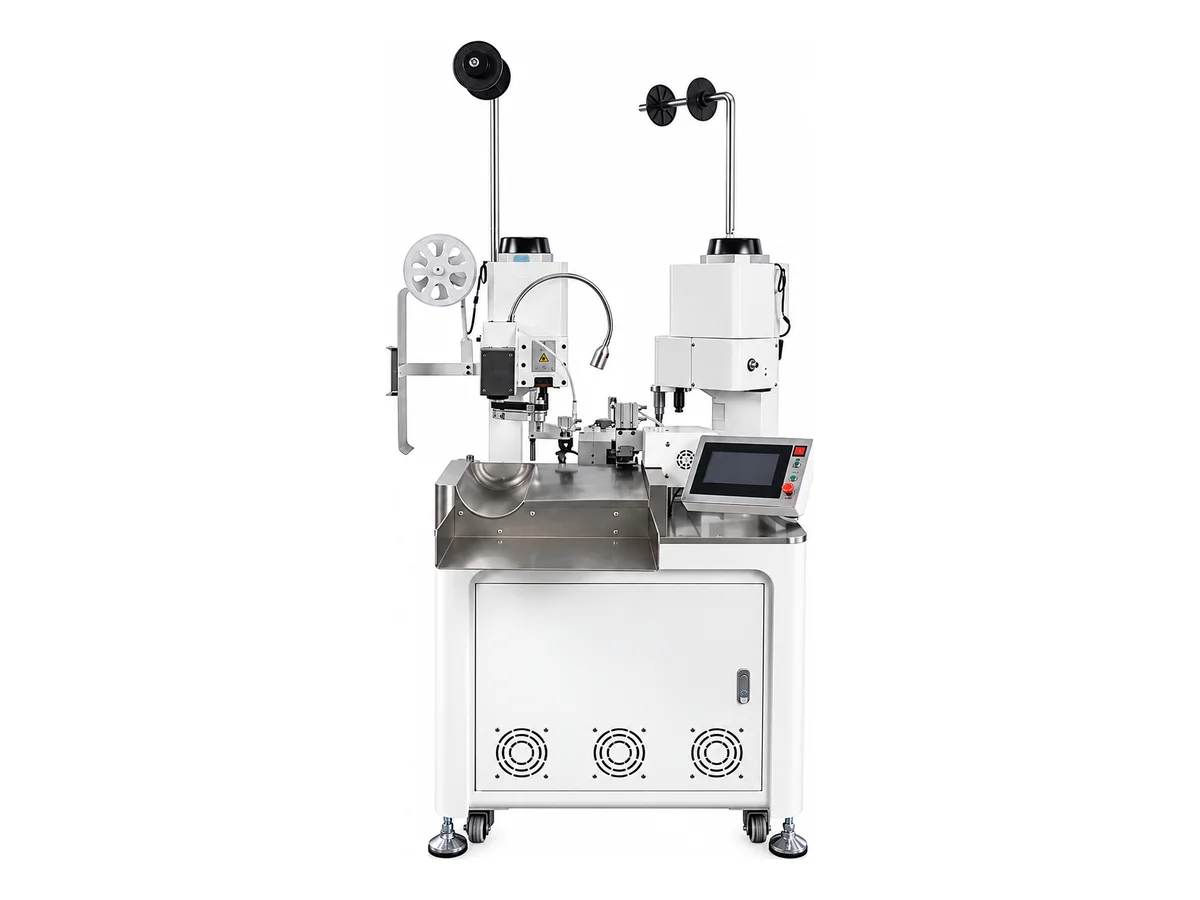
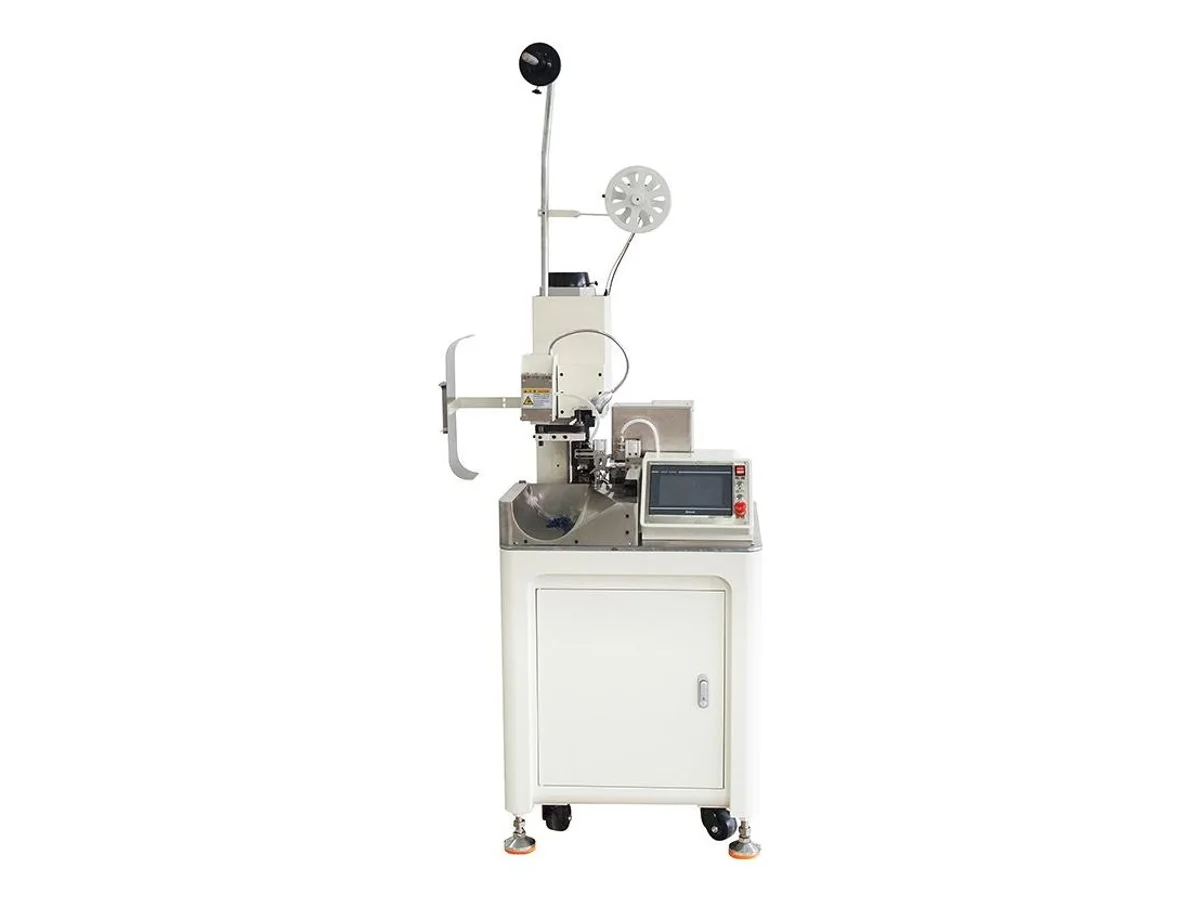
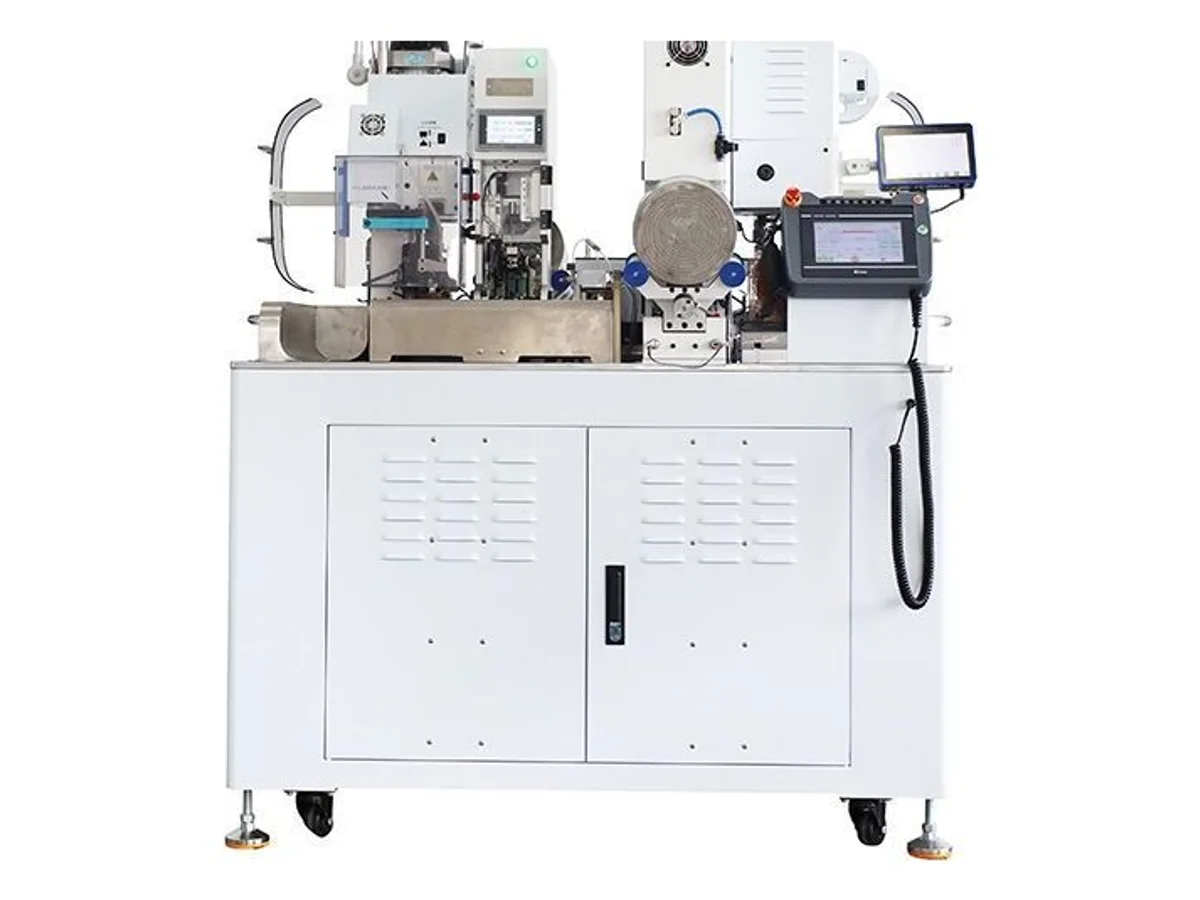
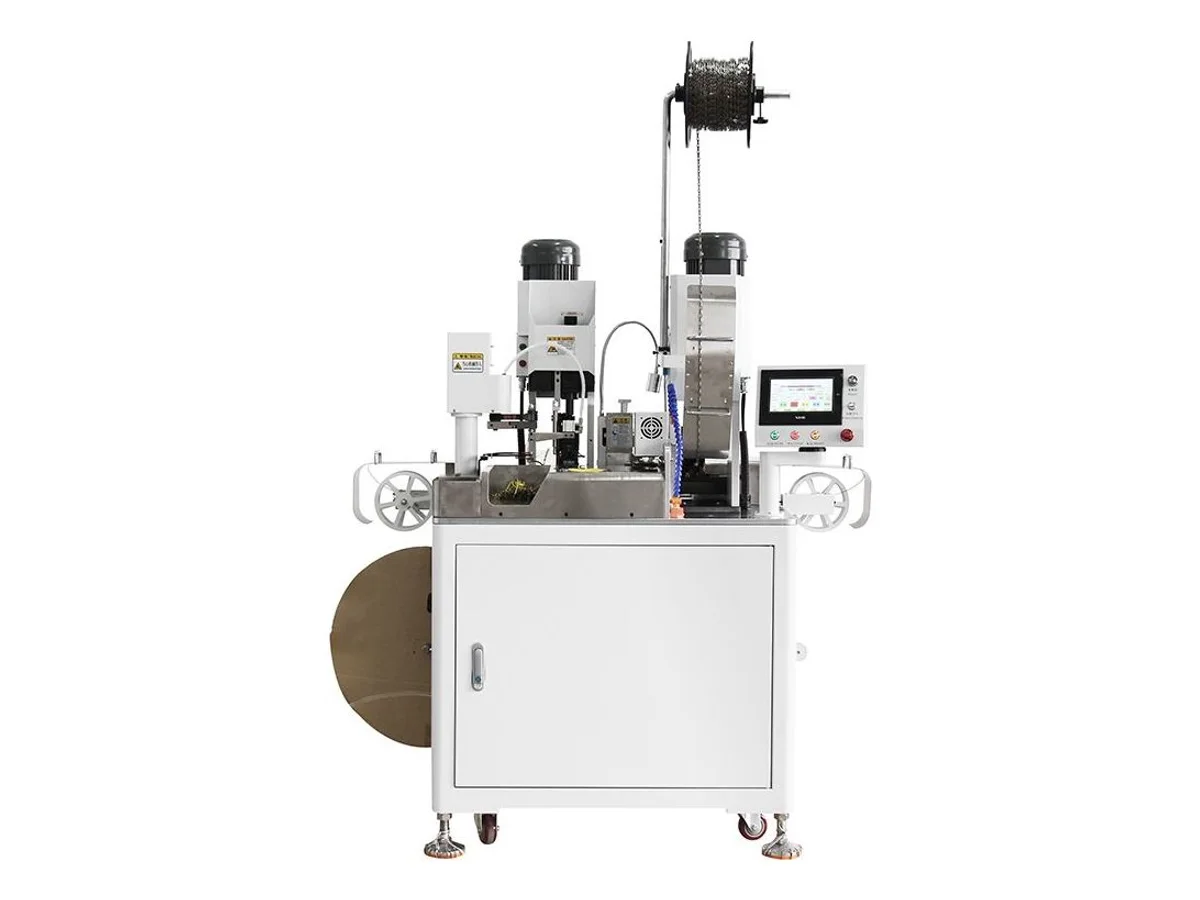
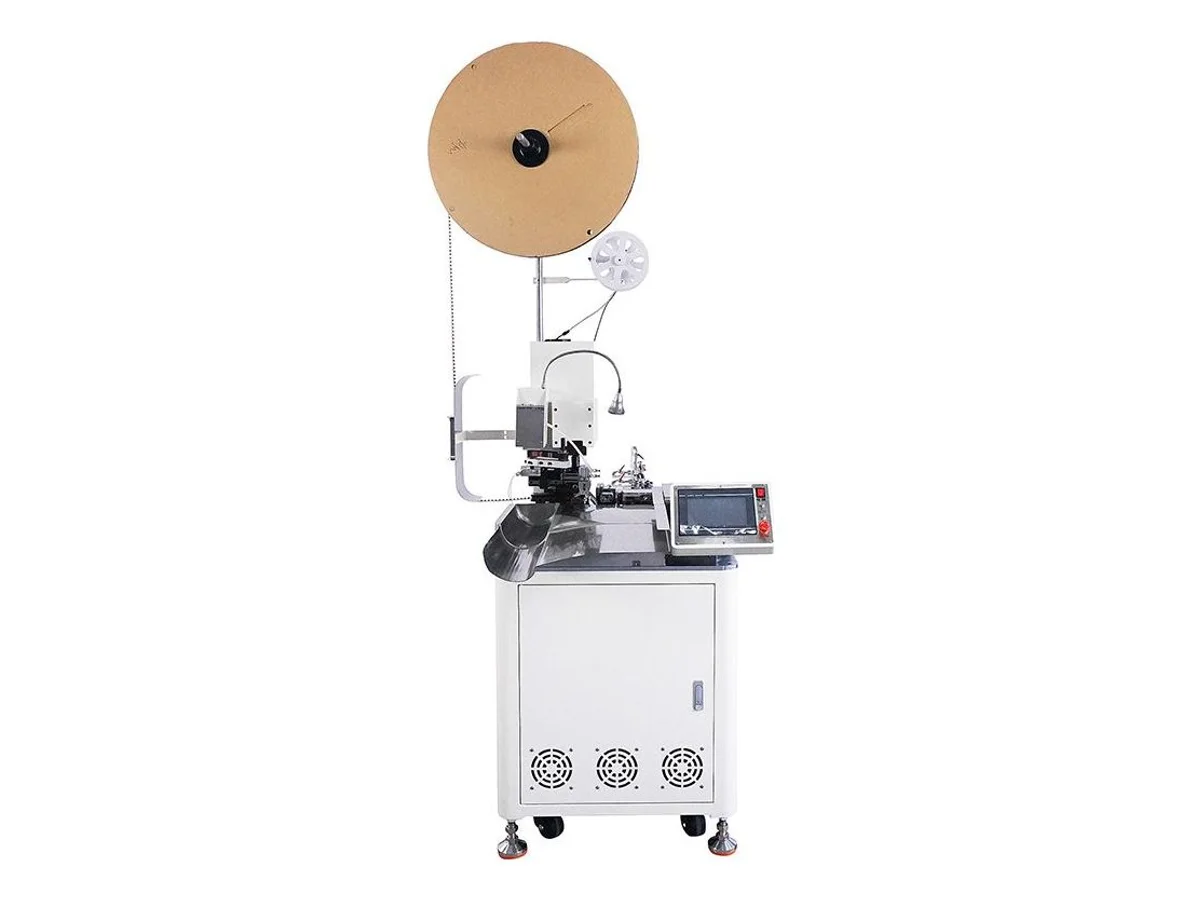
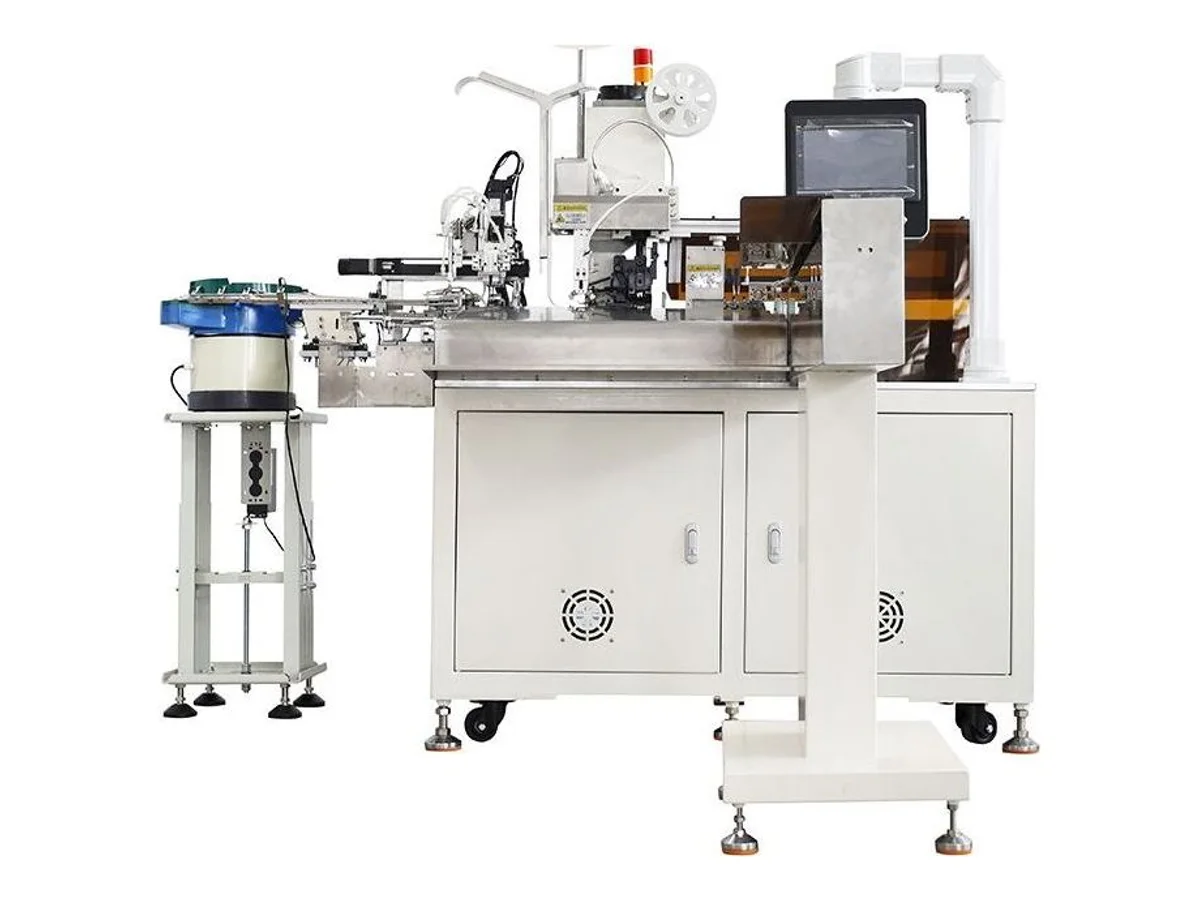
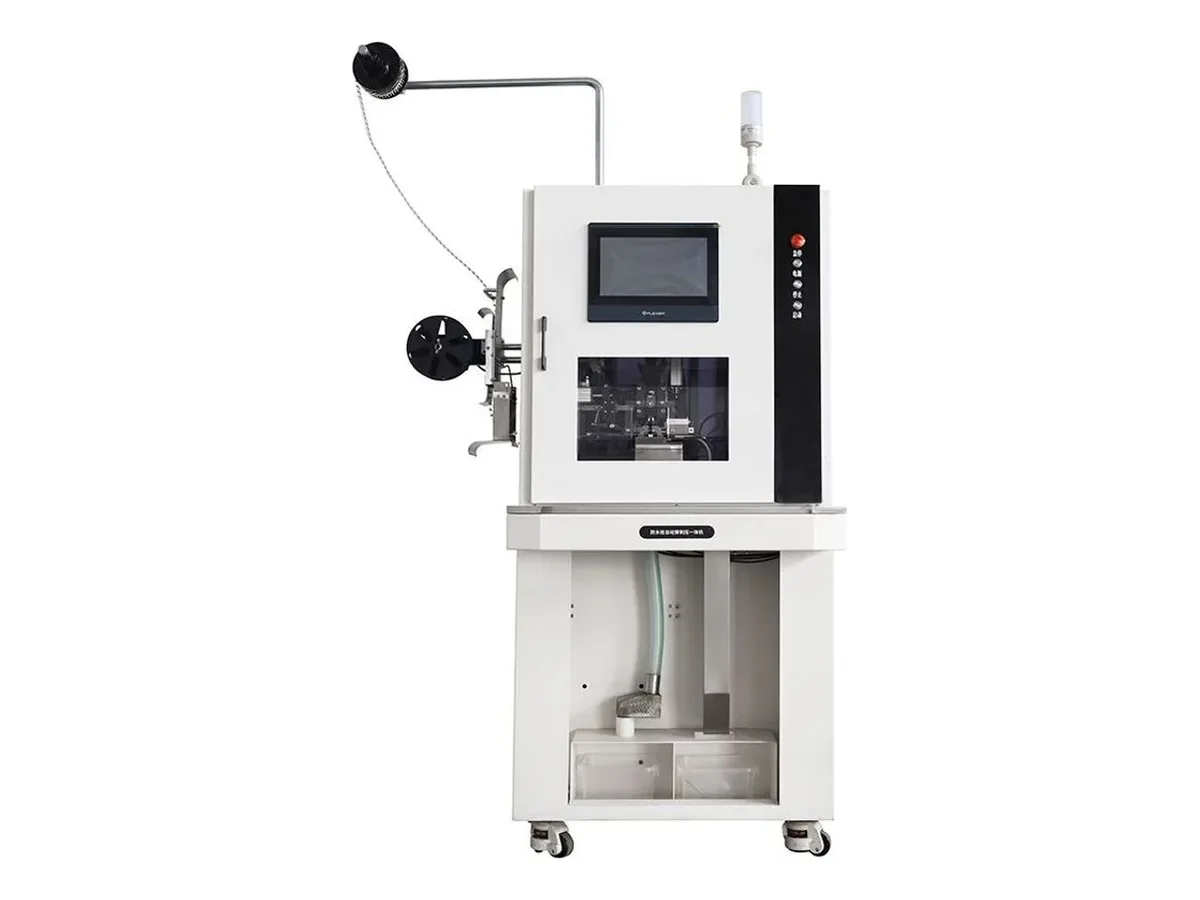
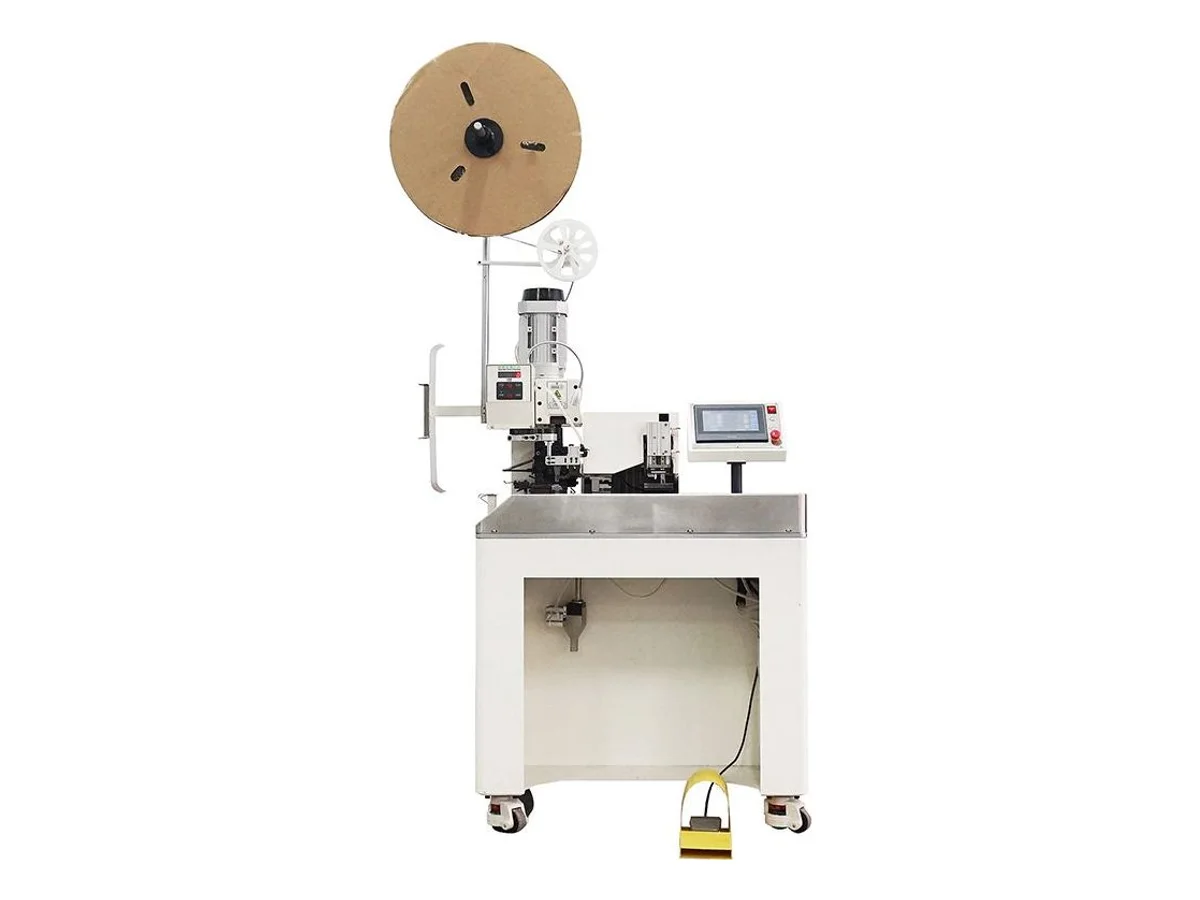
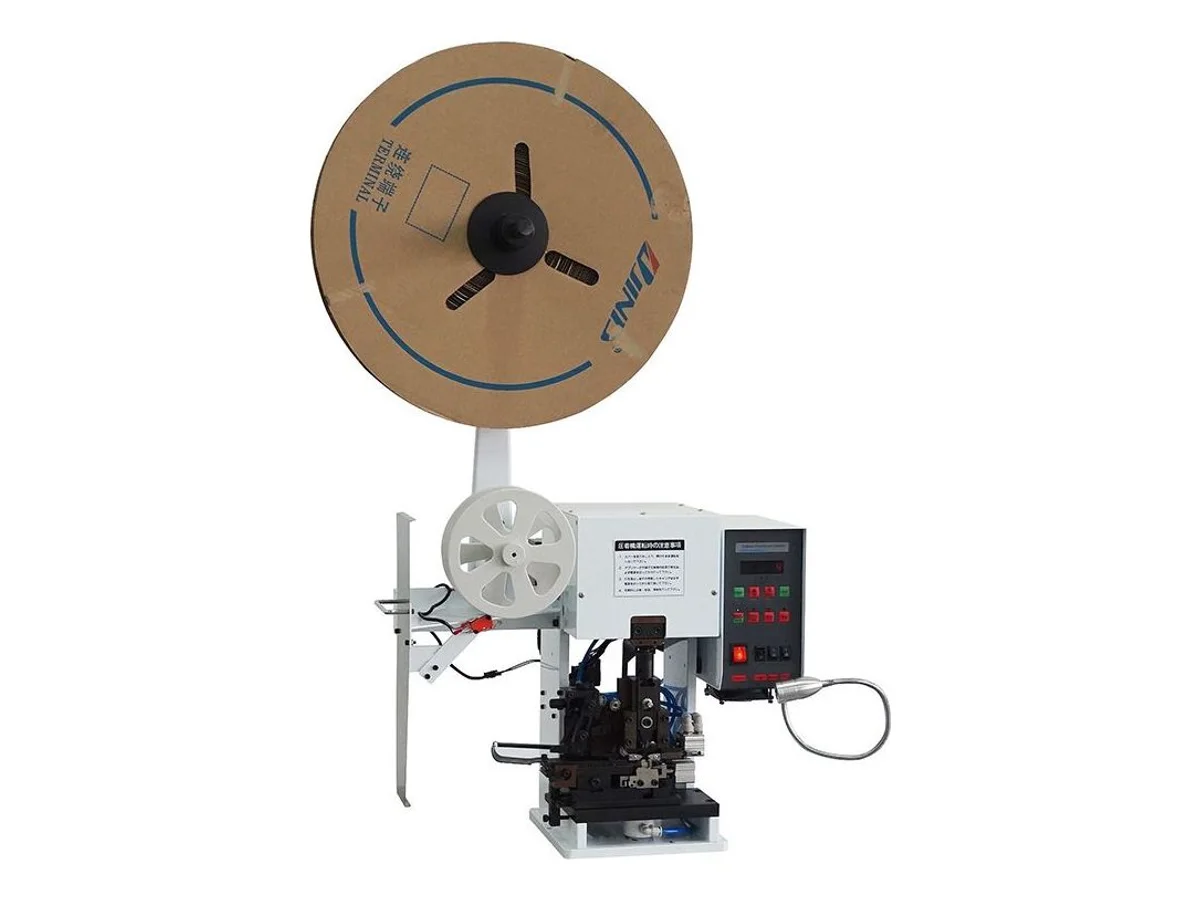
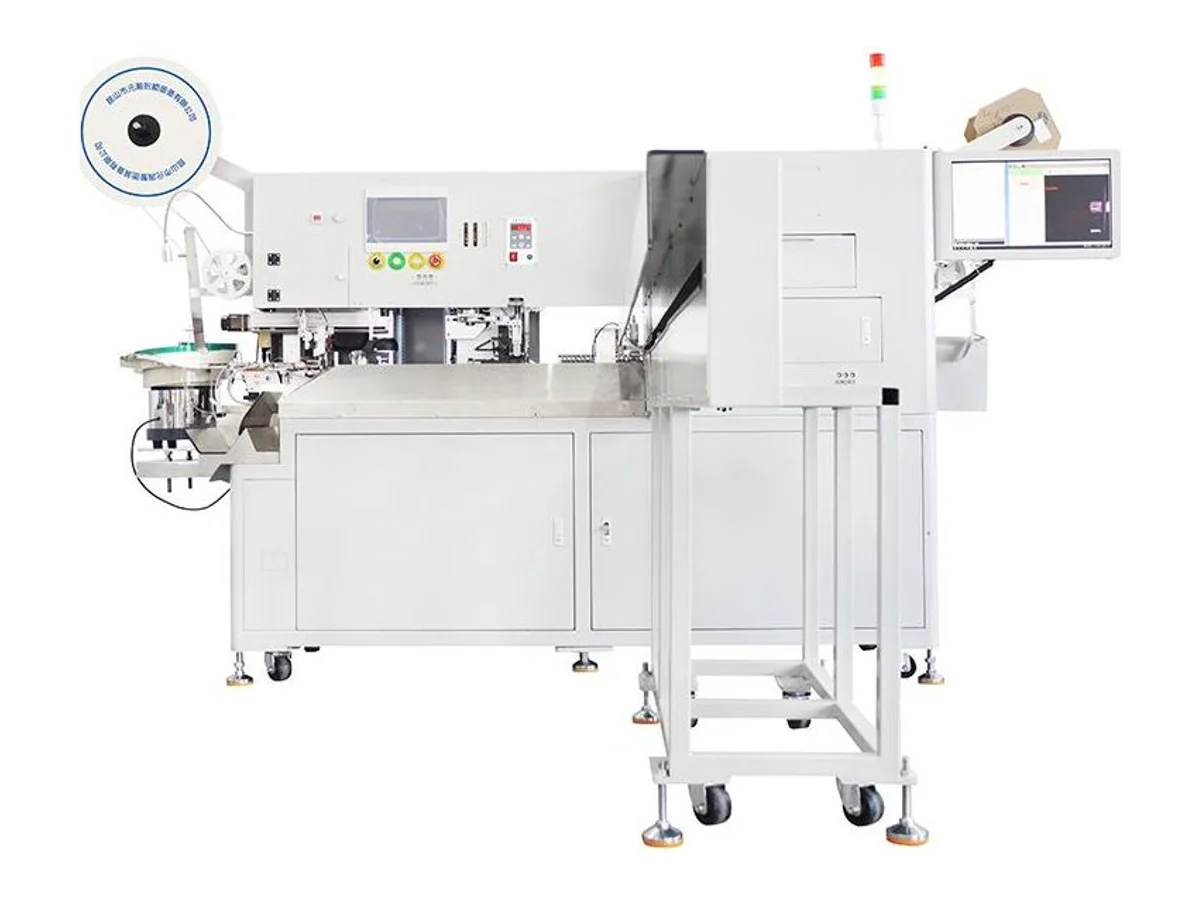
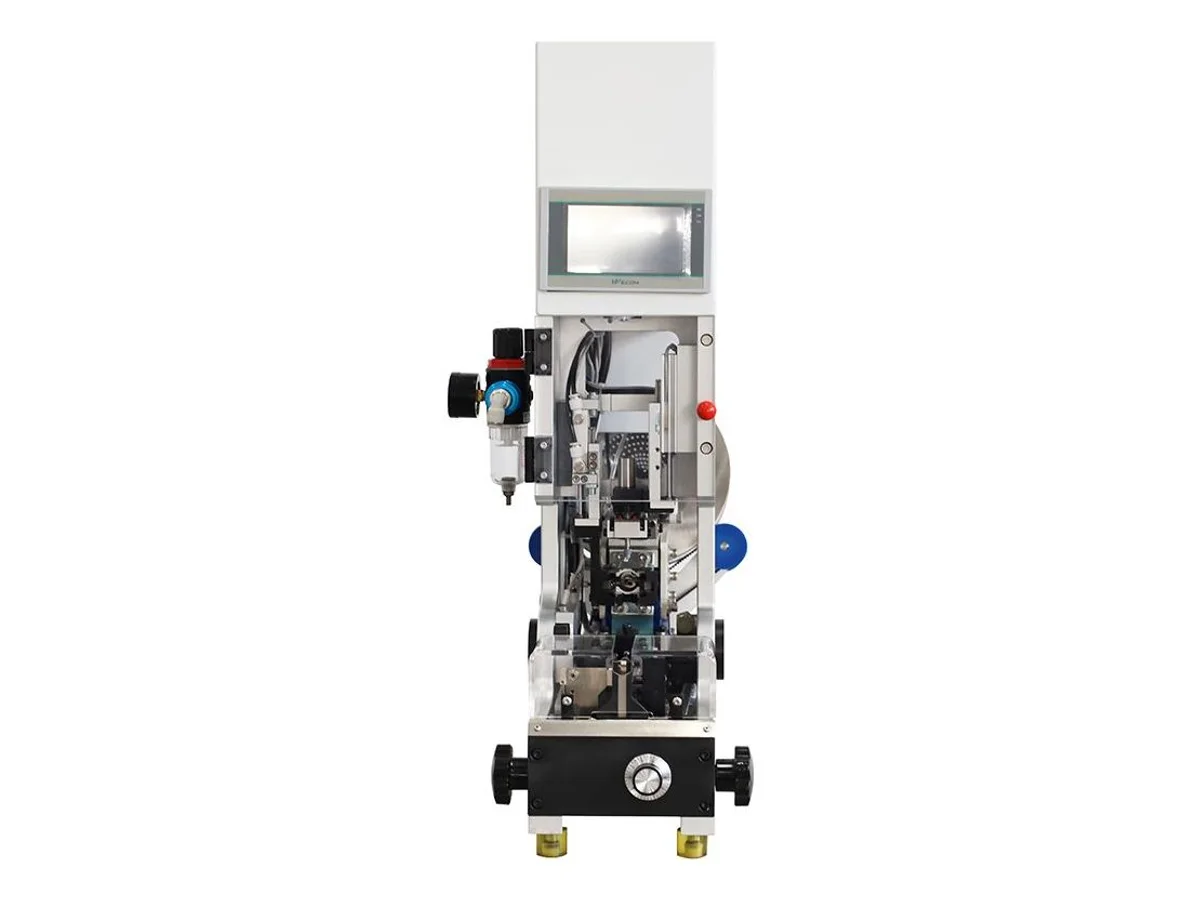
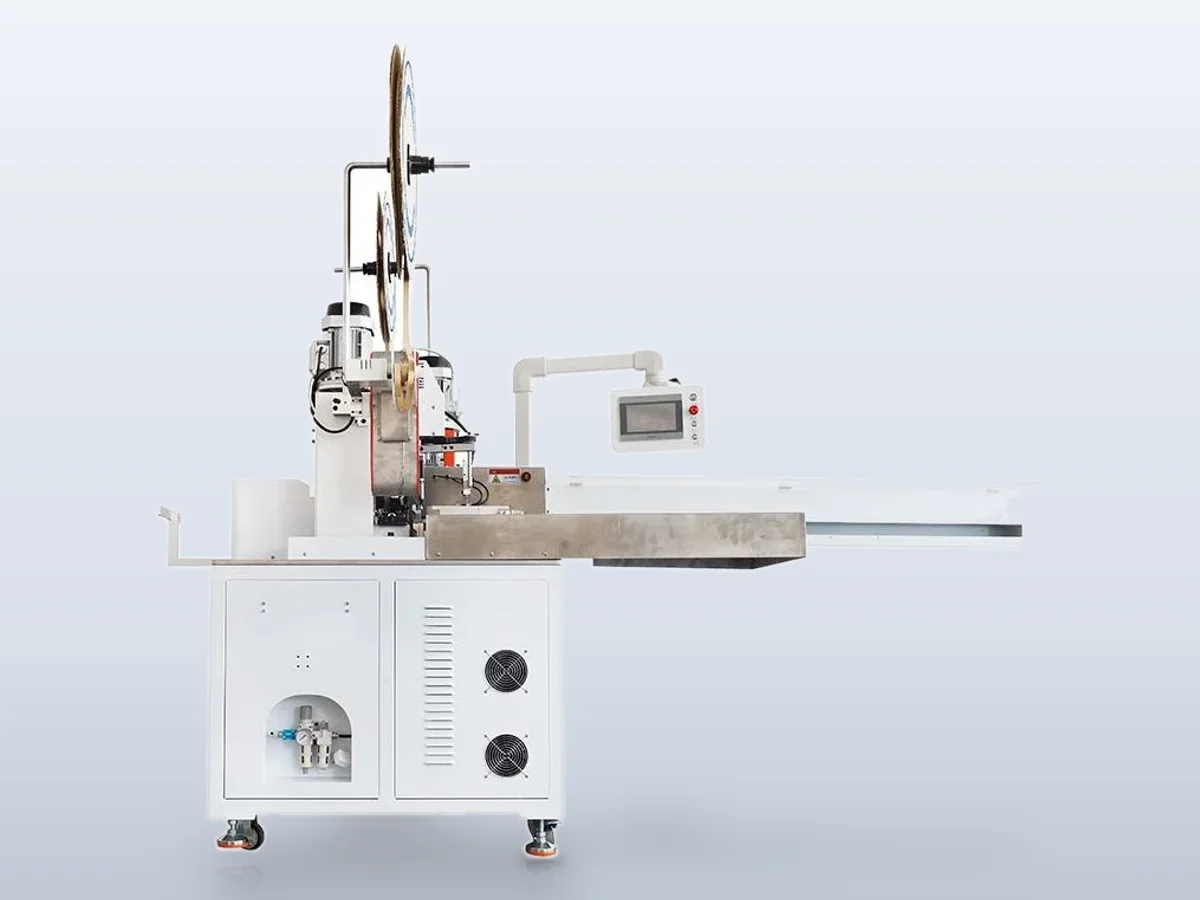
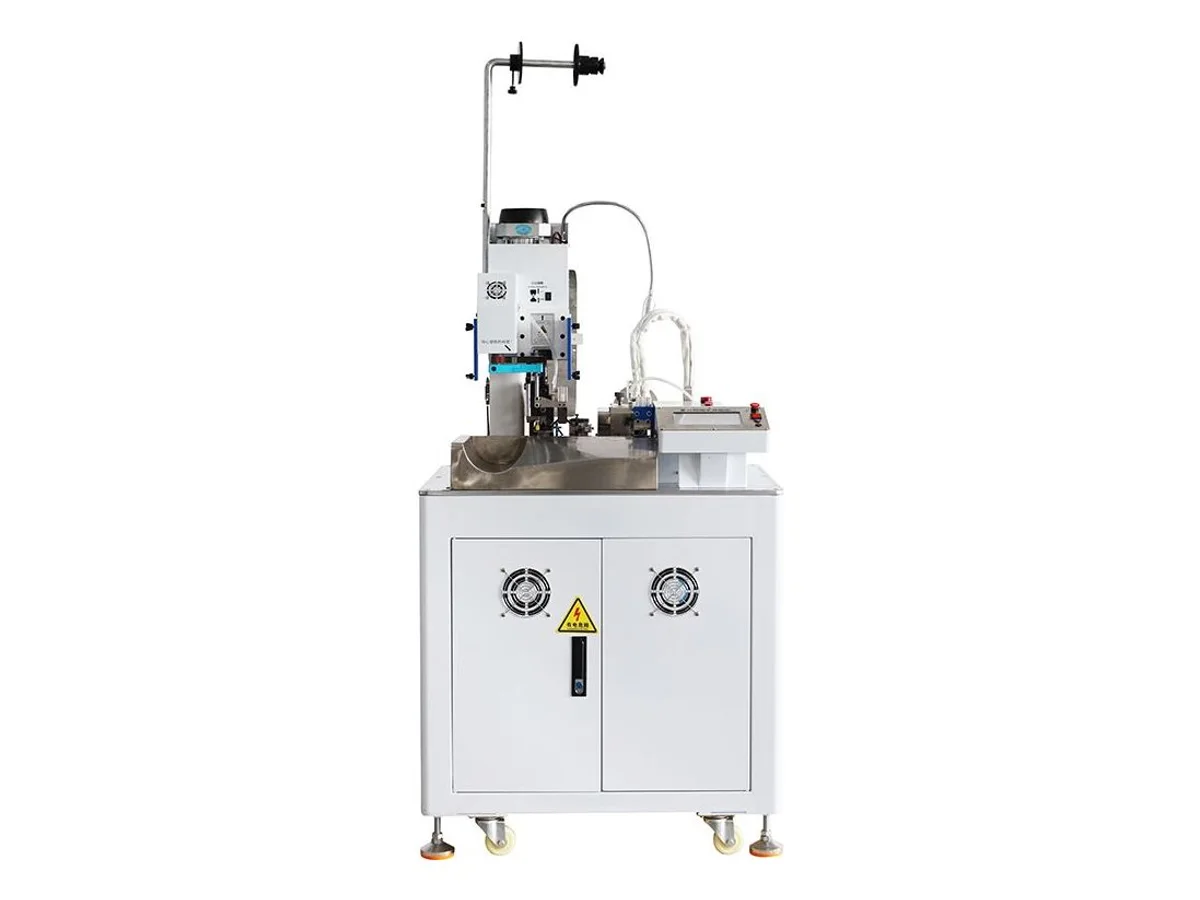
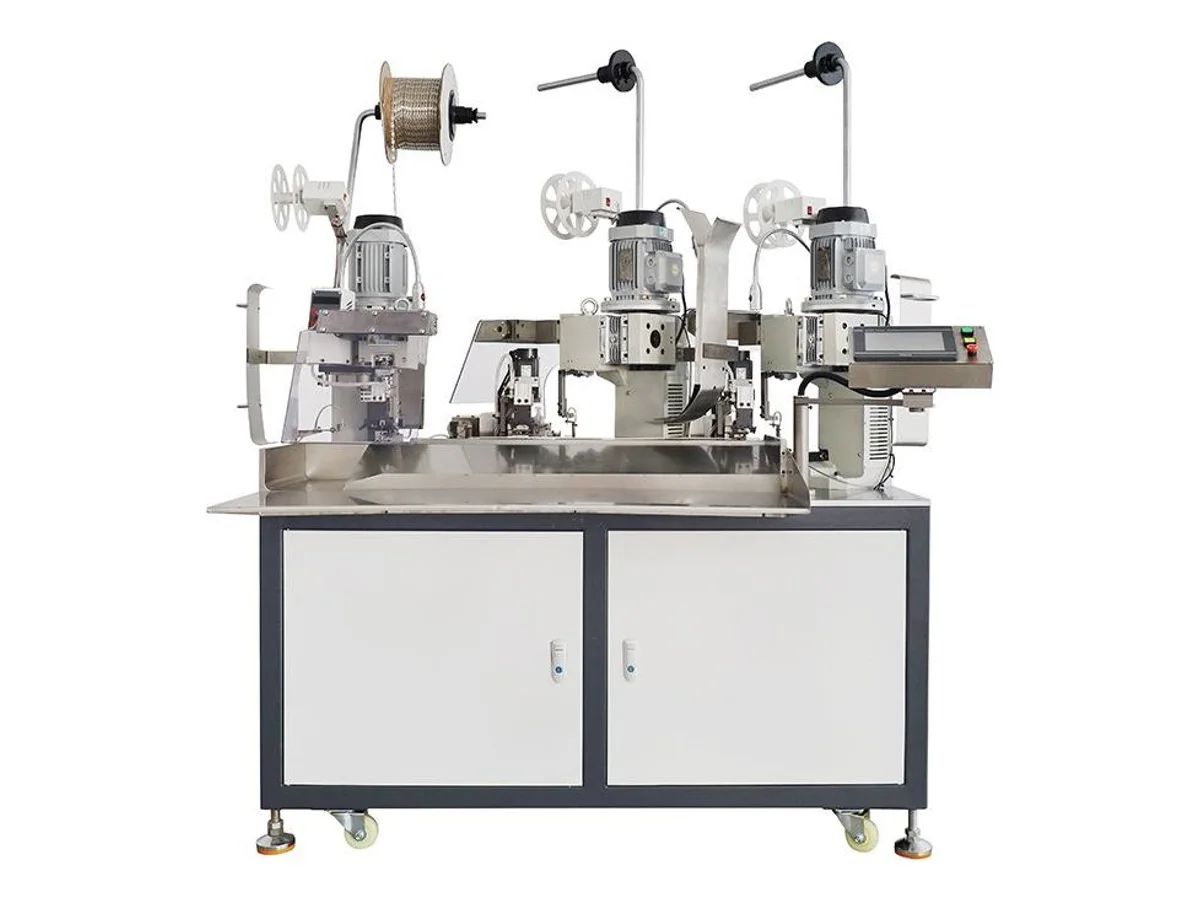
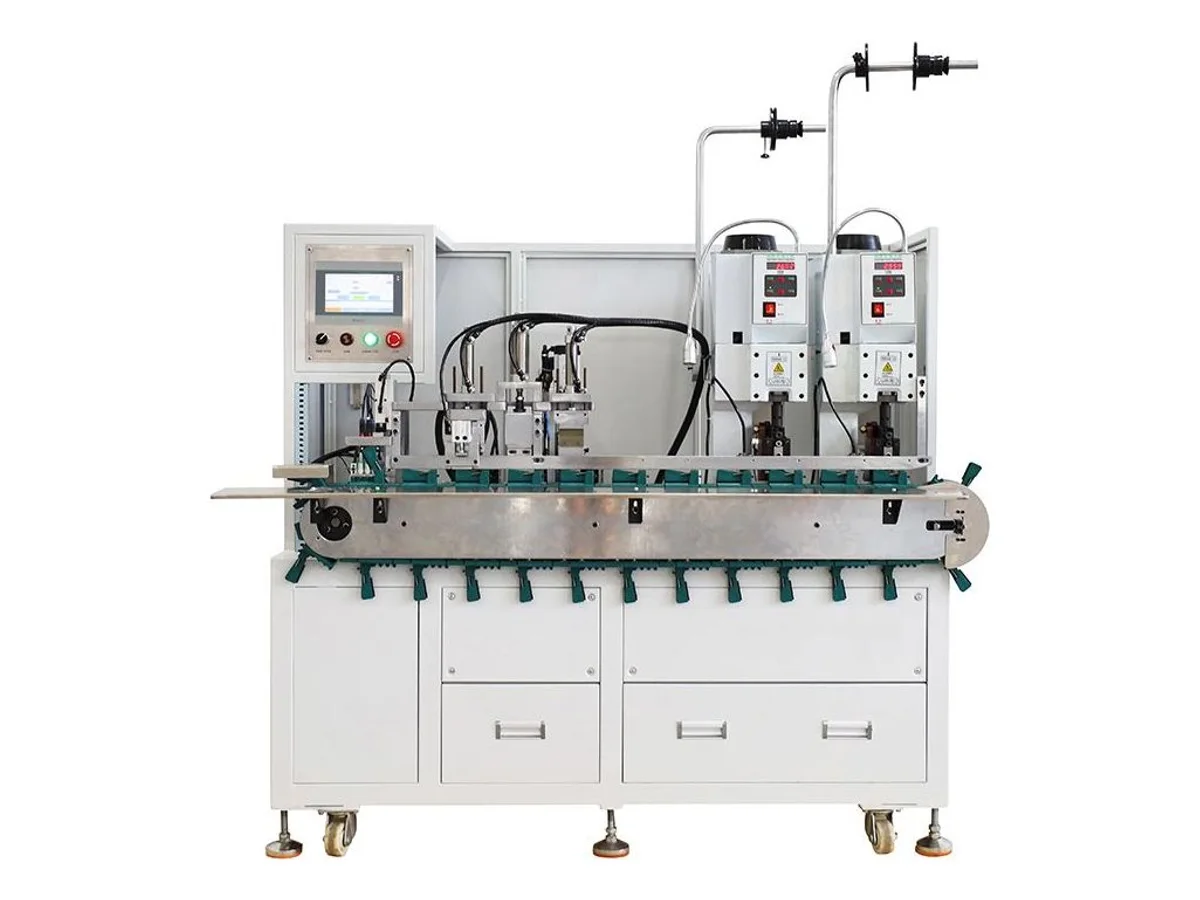
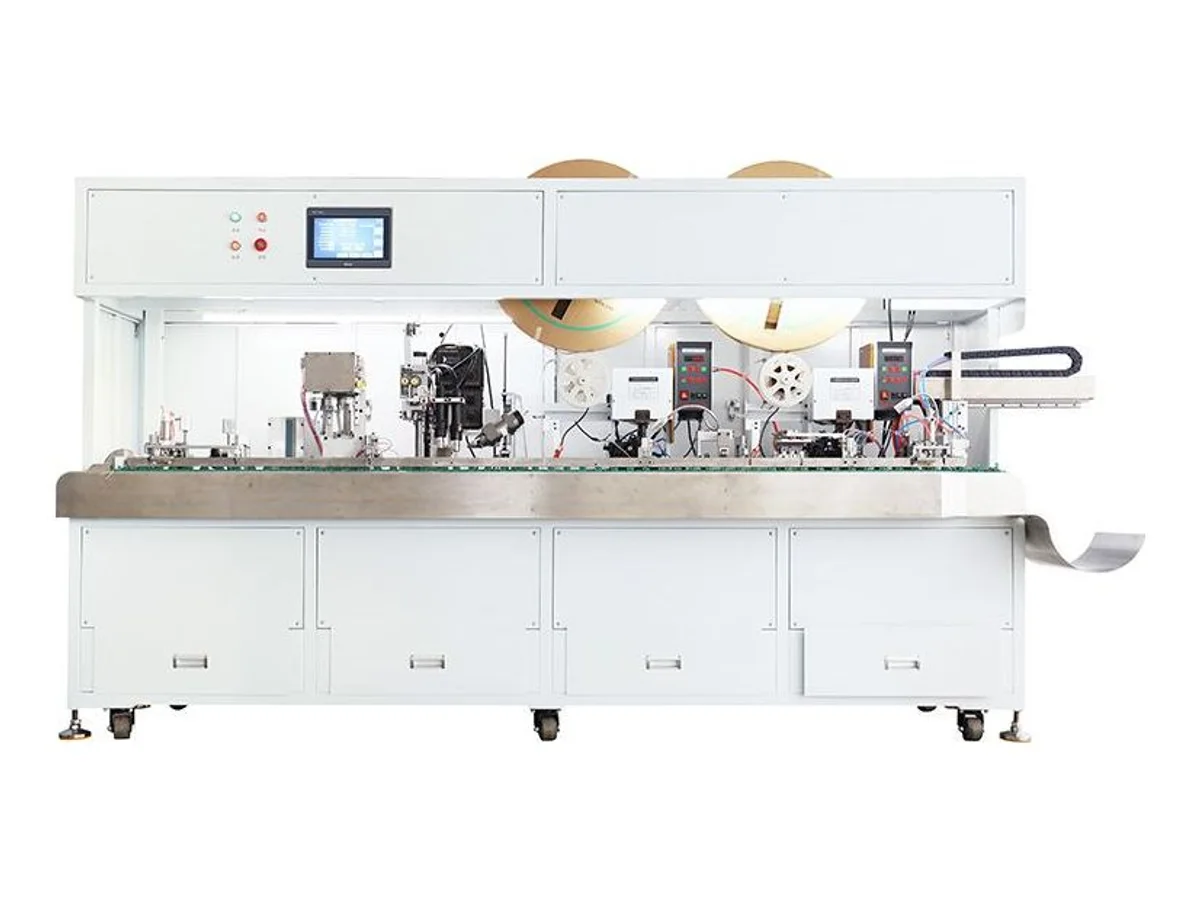
Tinning and crimping on the same line
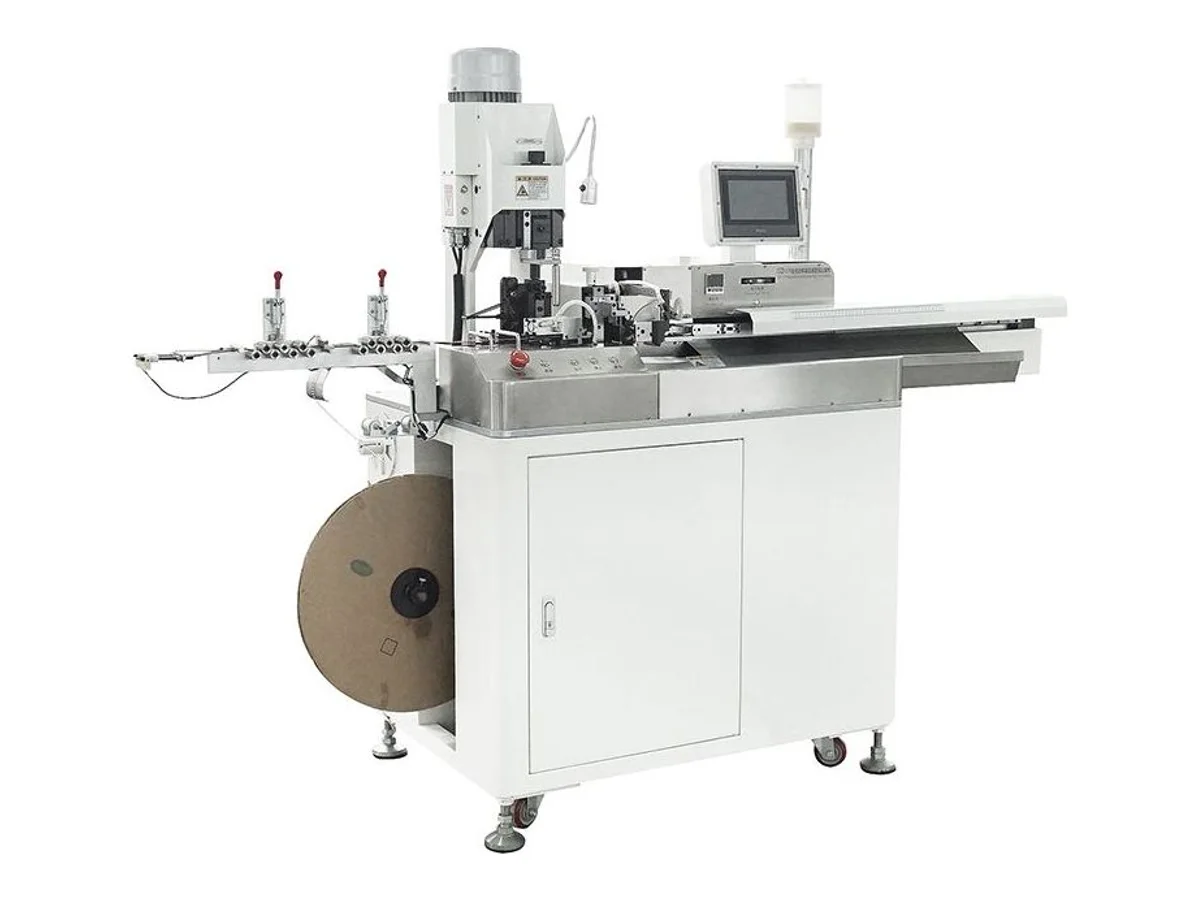
Model WM-462
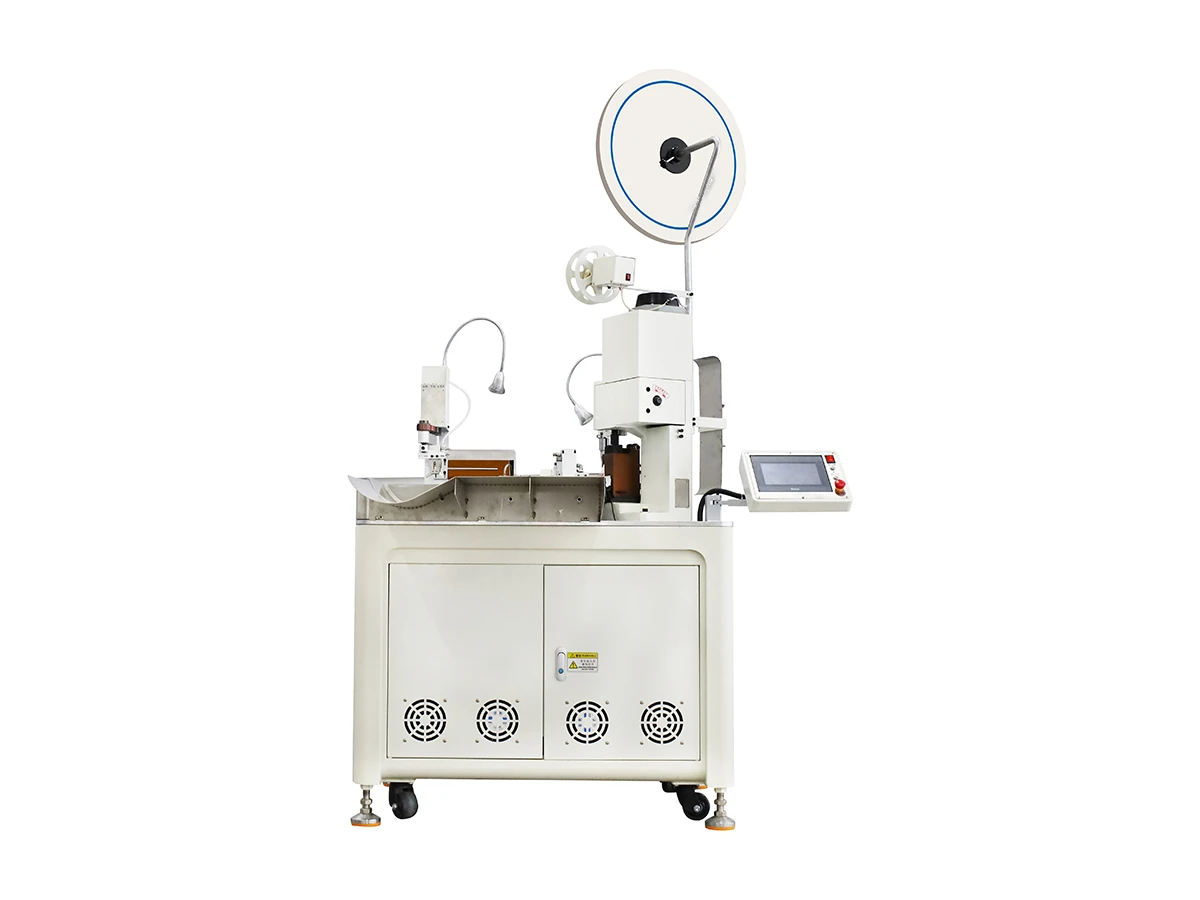
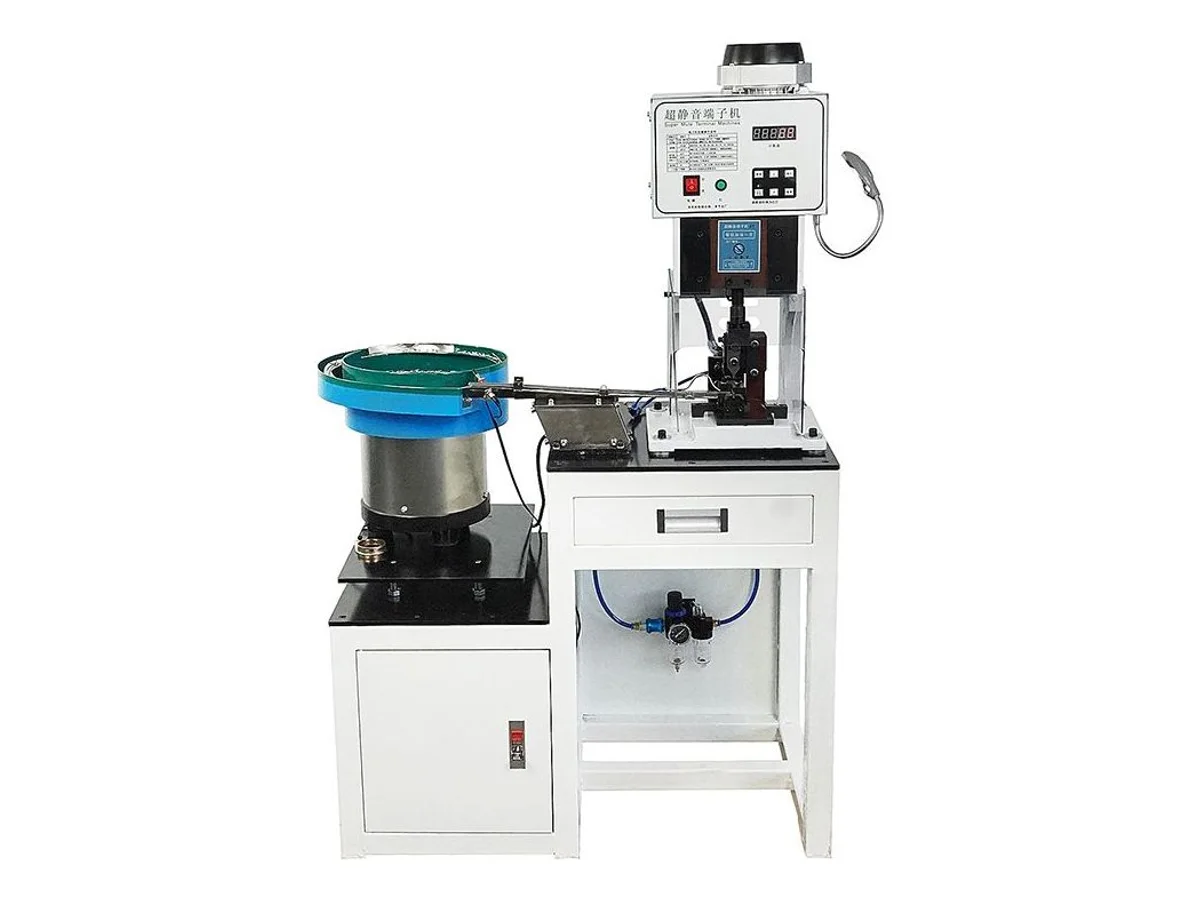
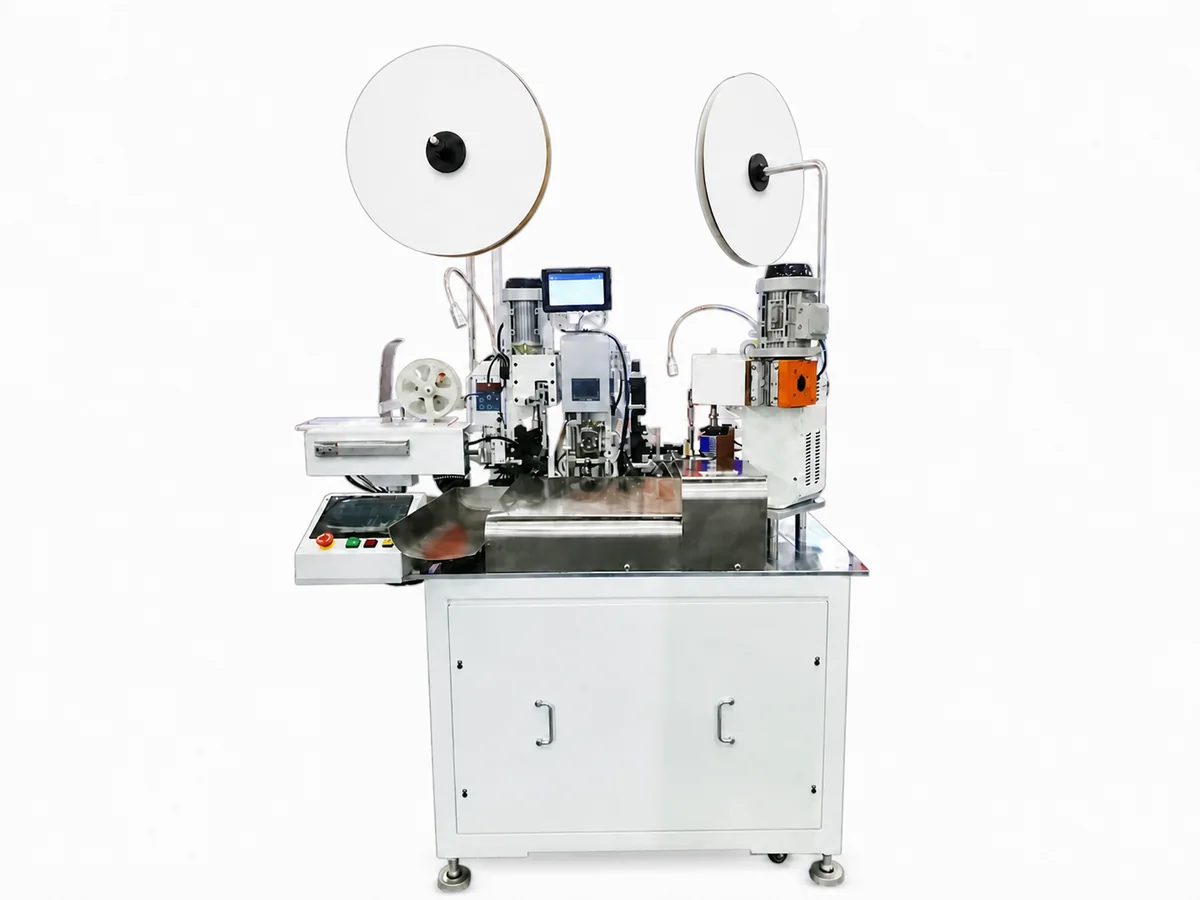
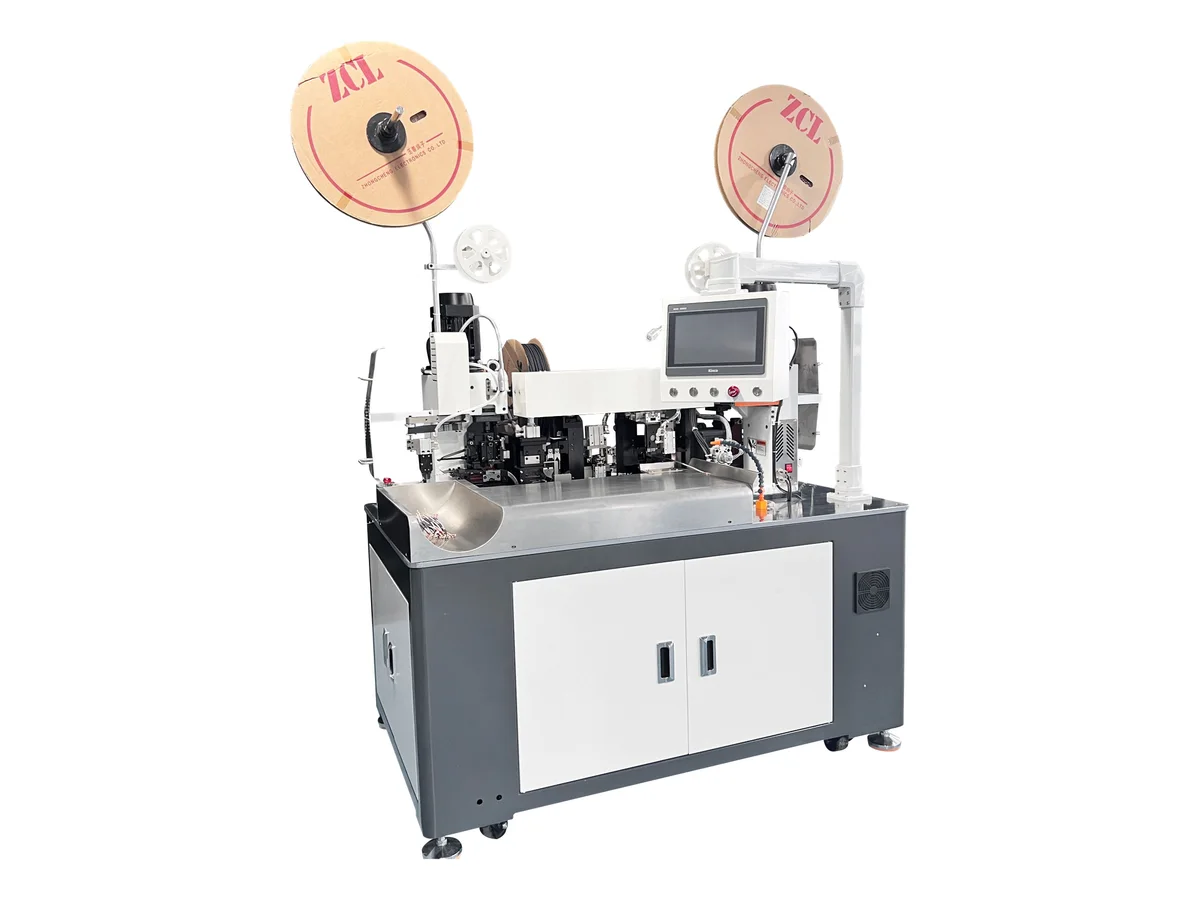
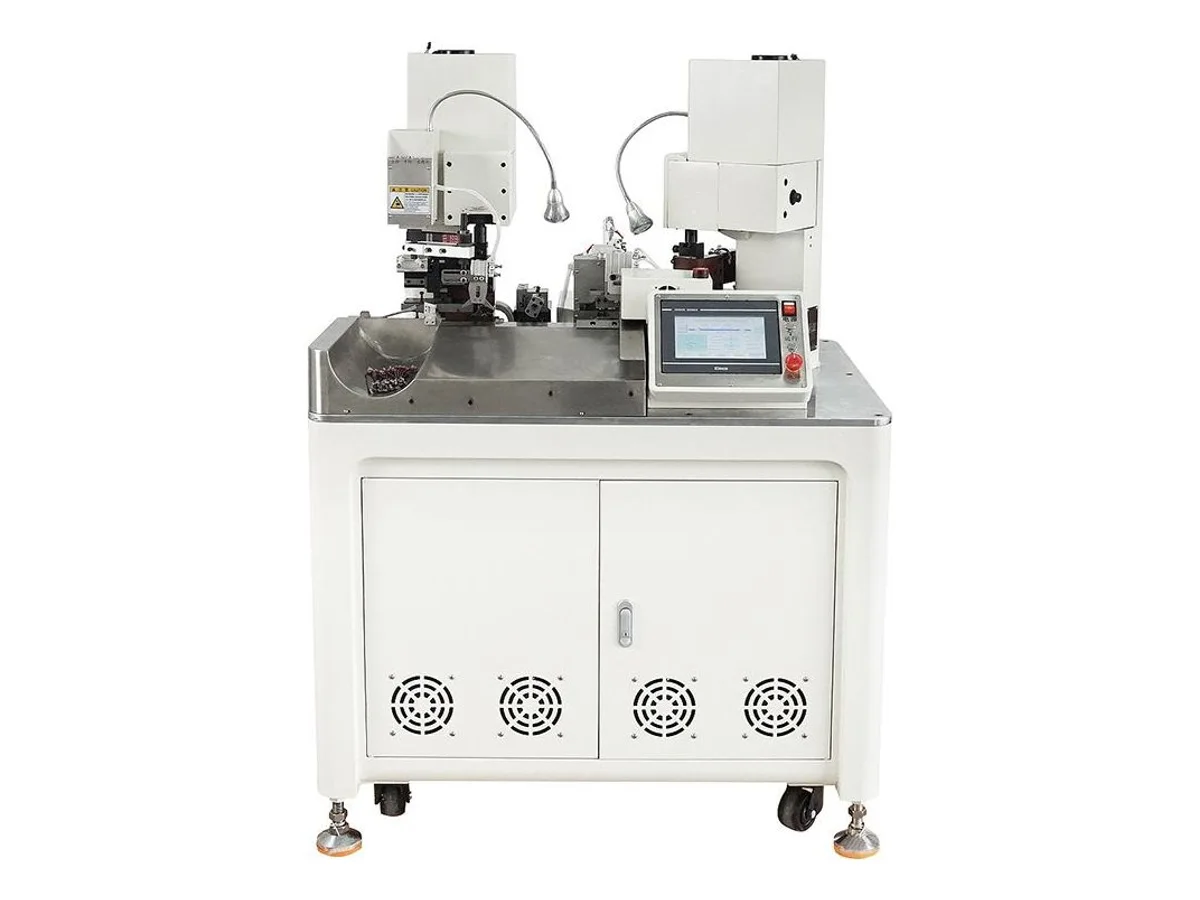
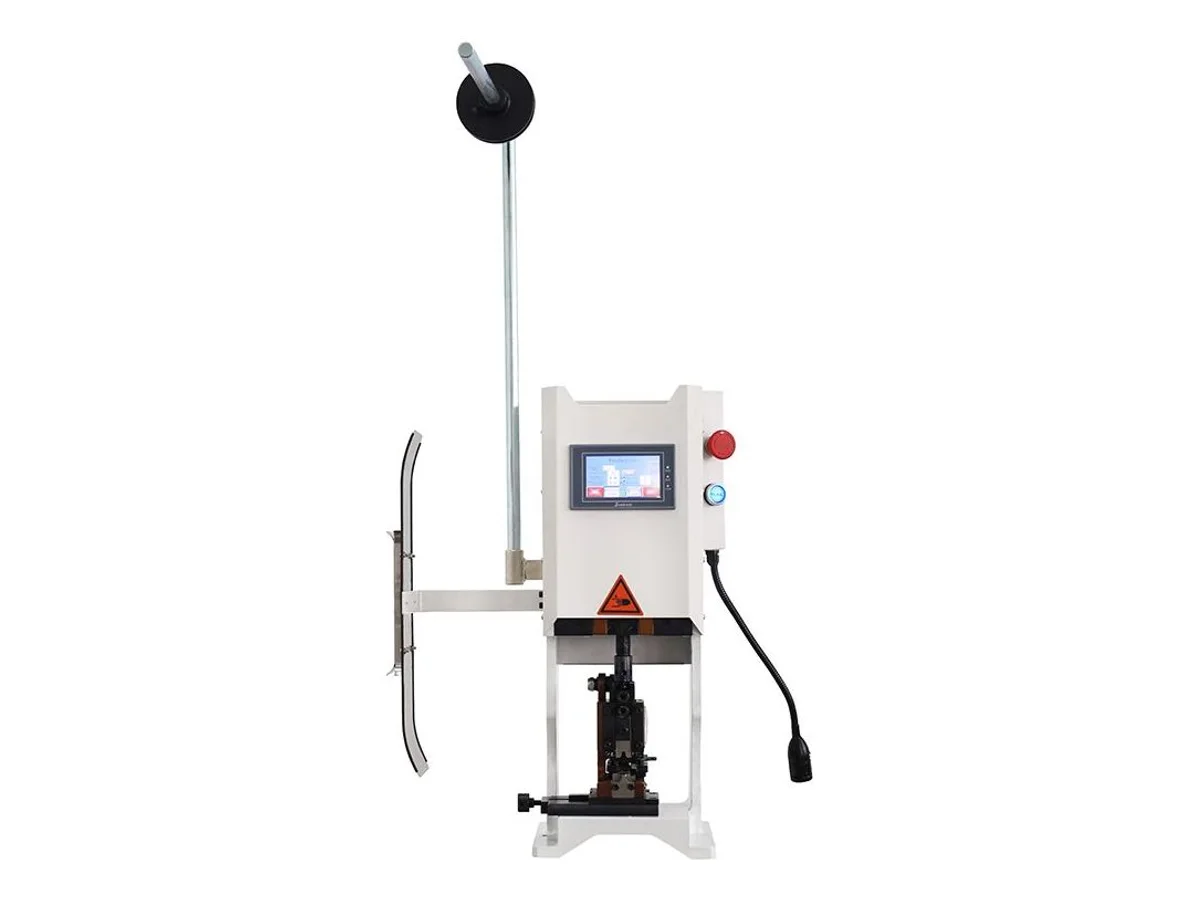
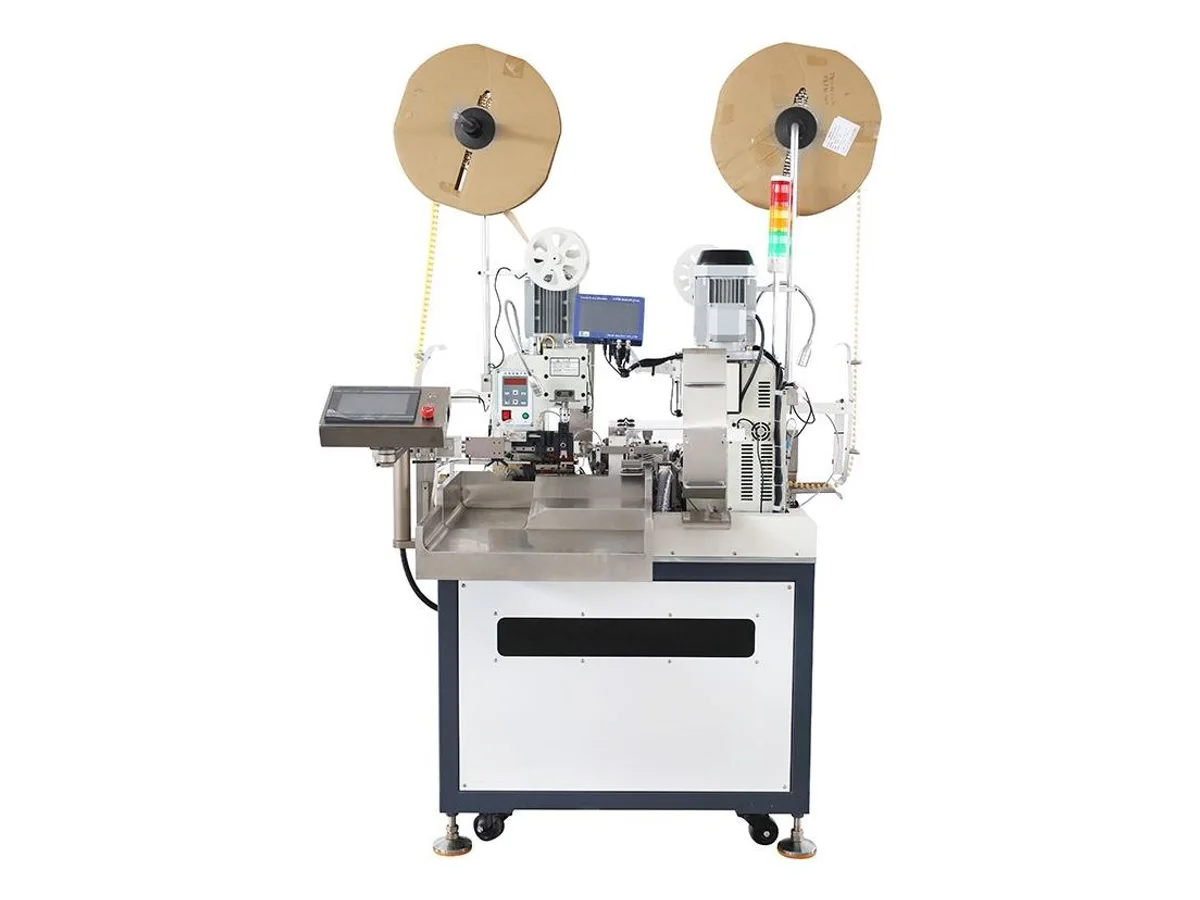
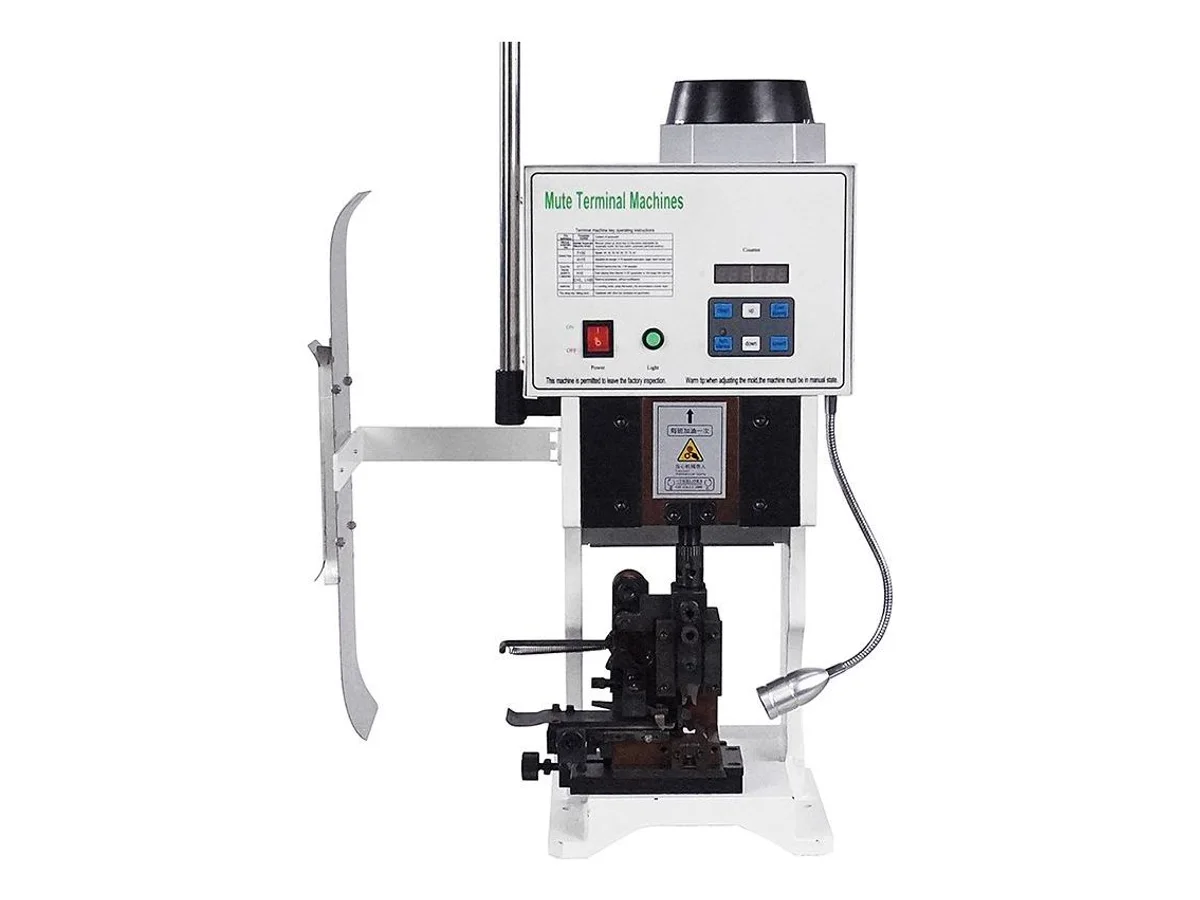
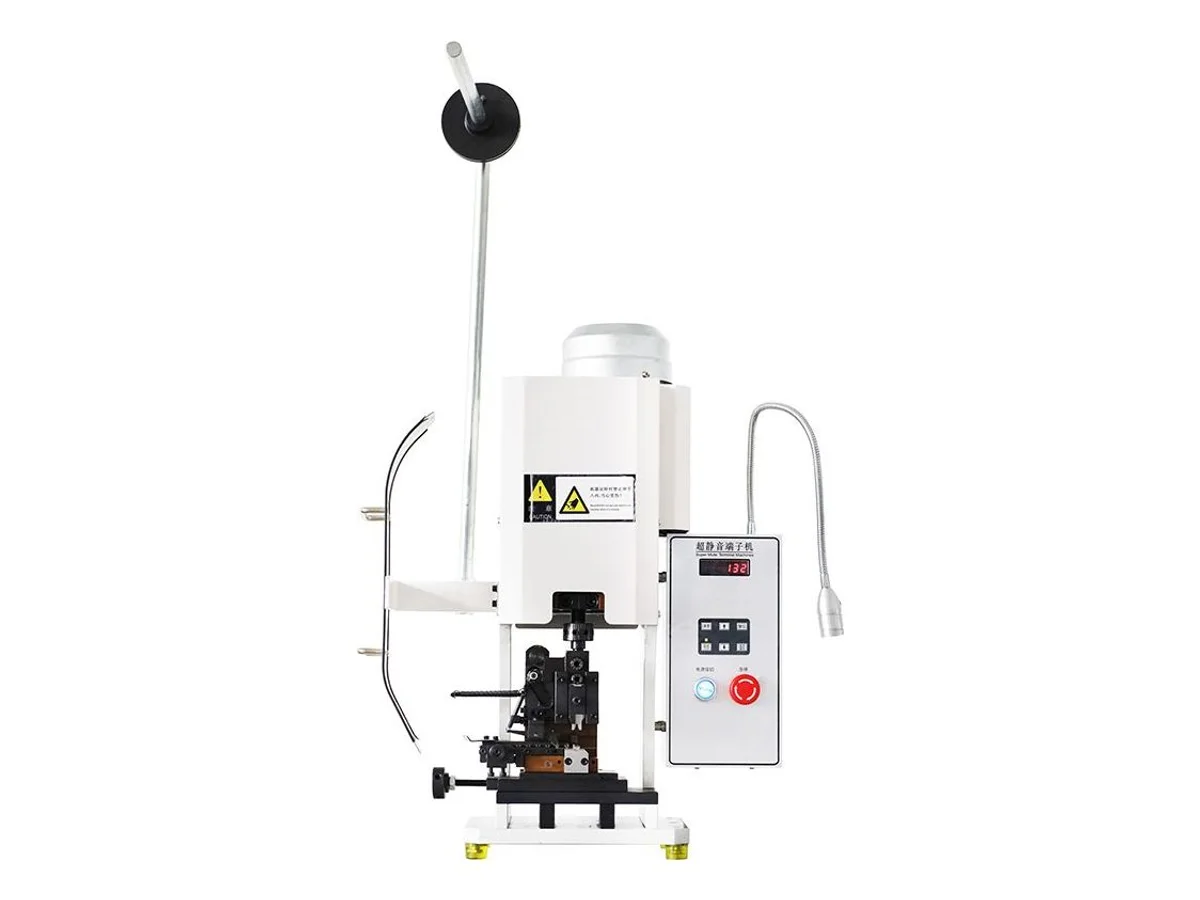
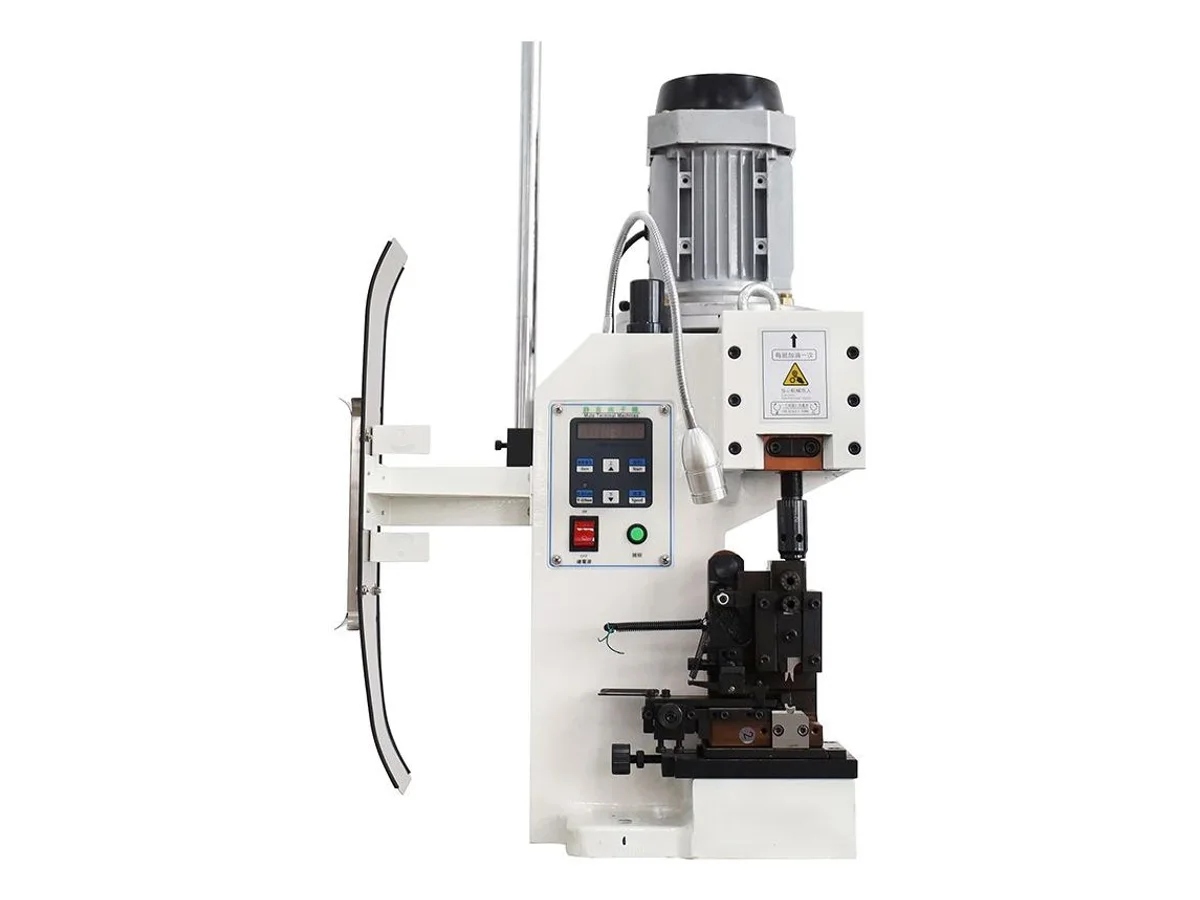
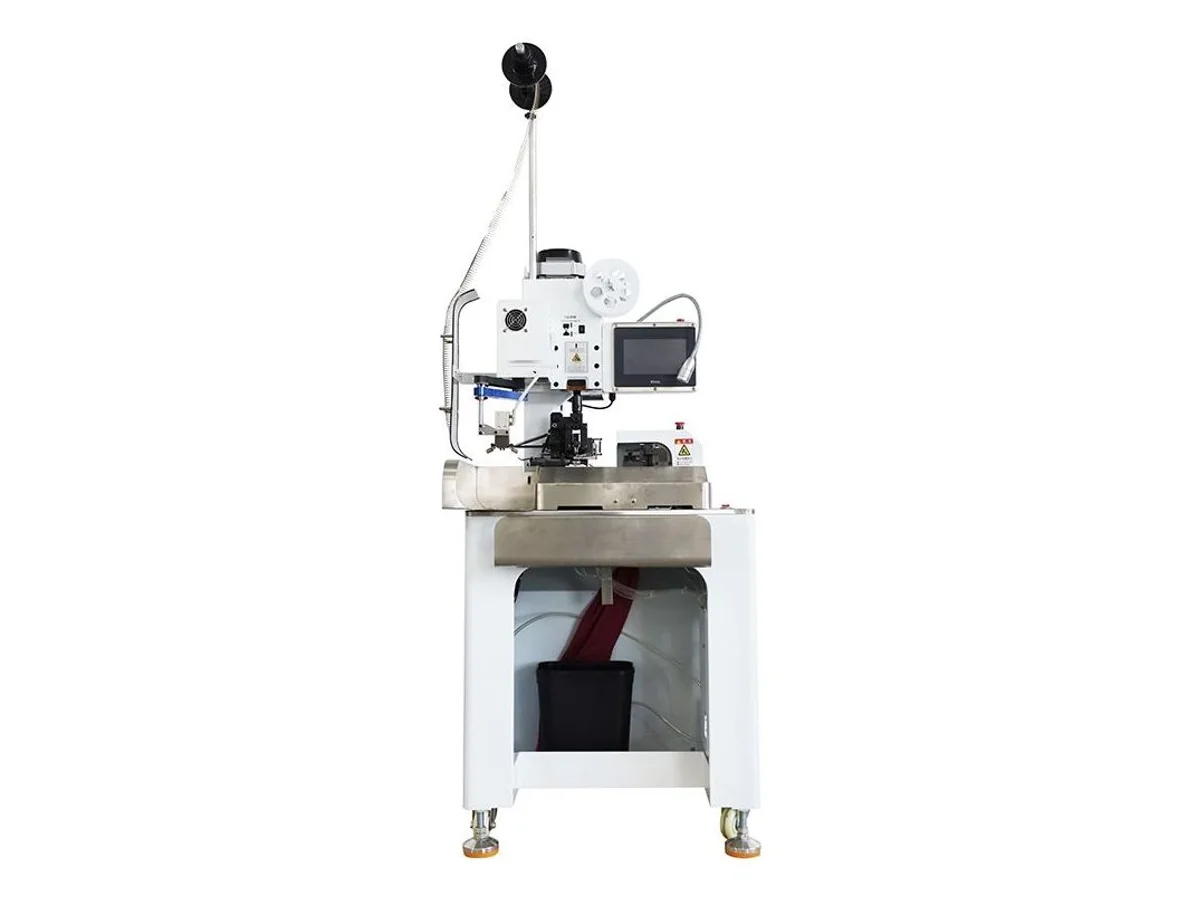
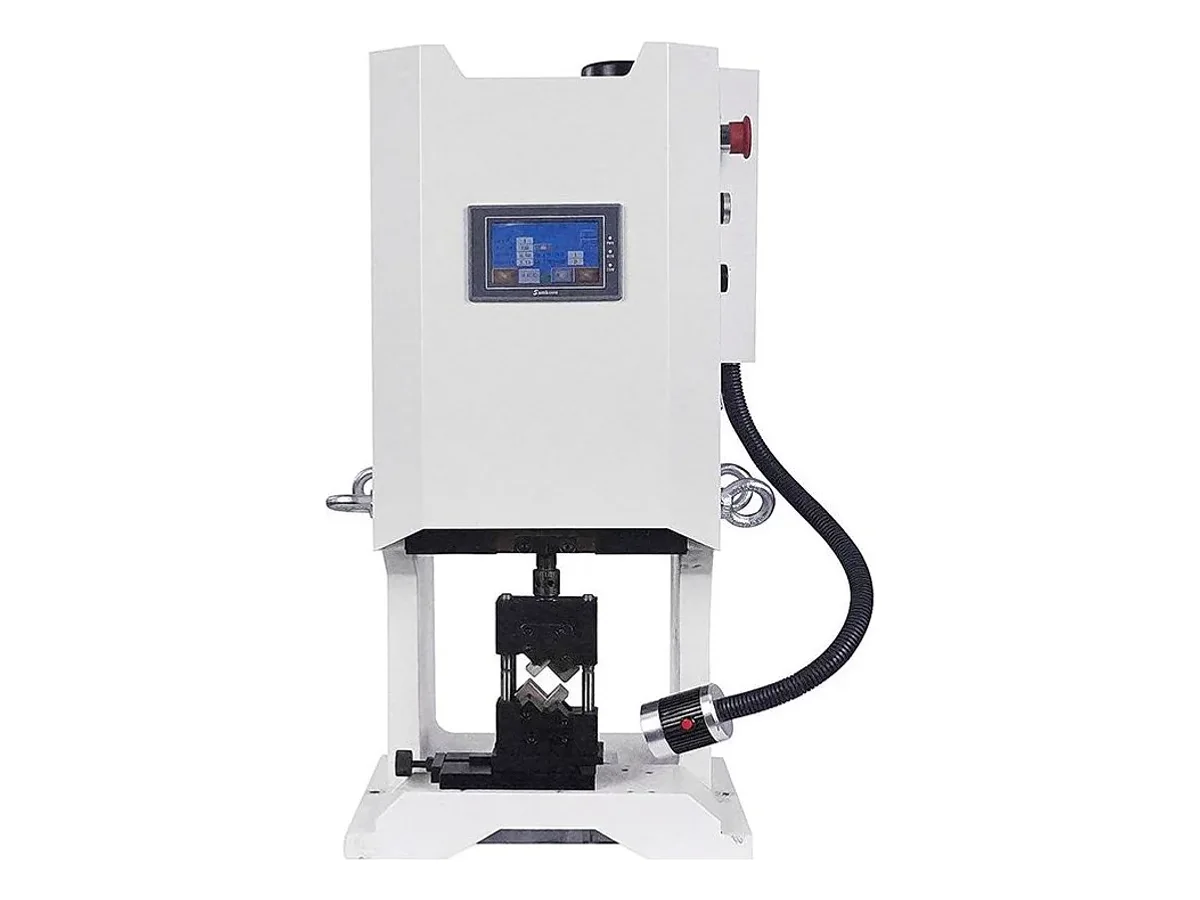
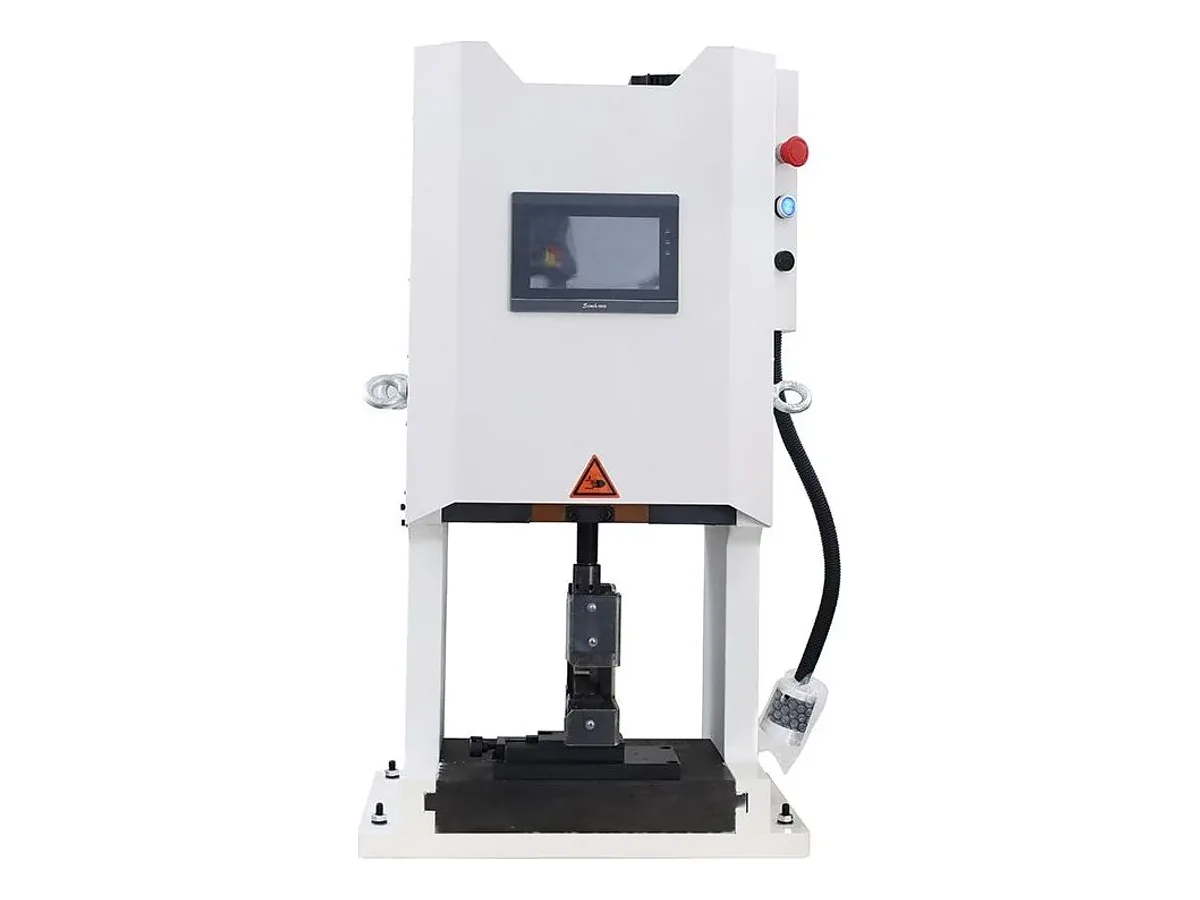
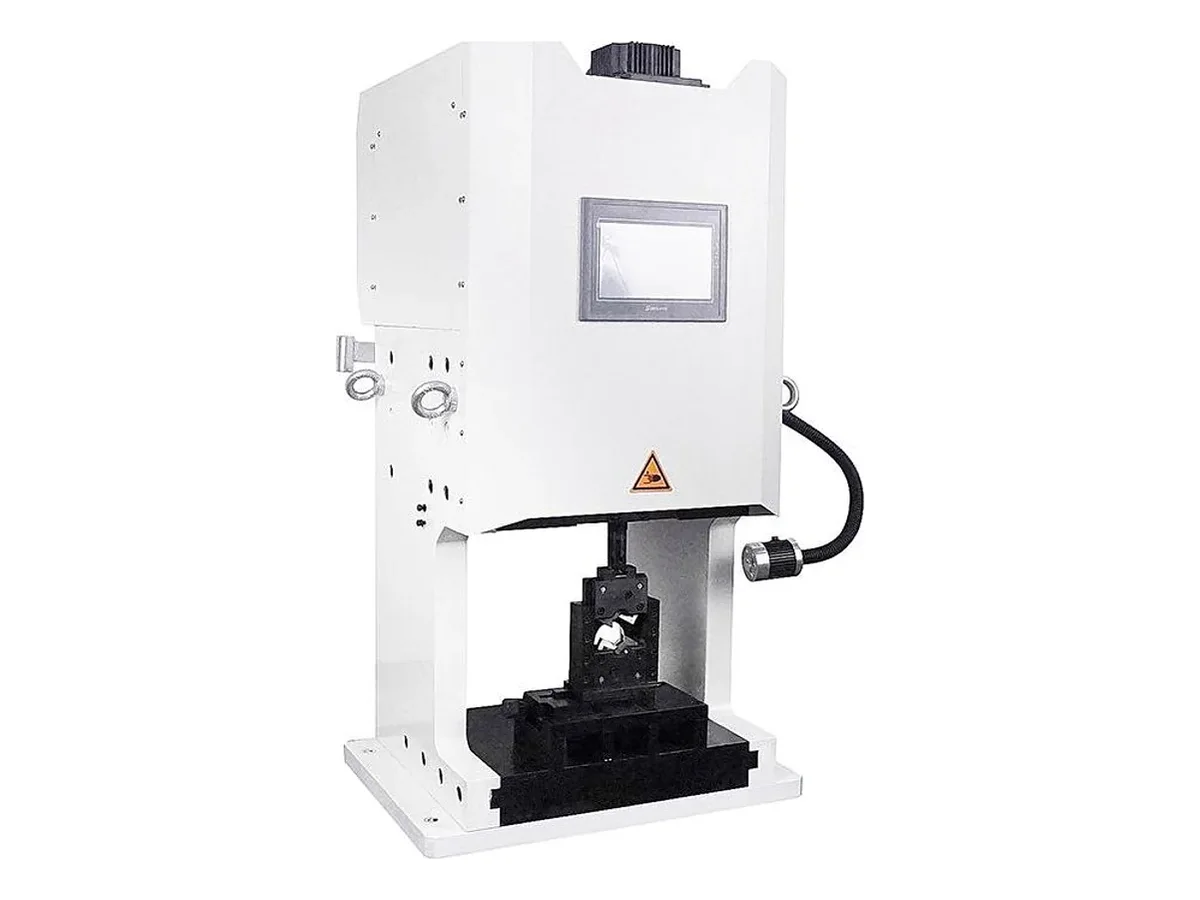
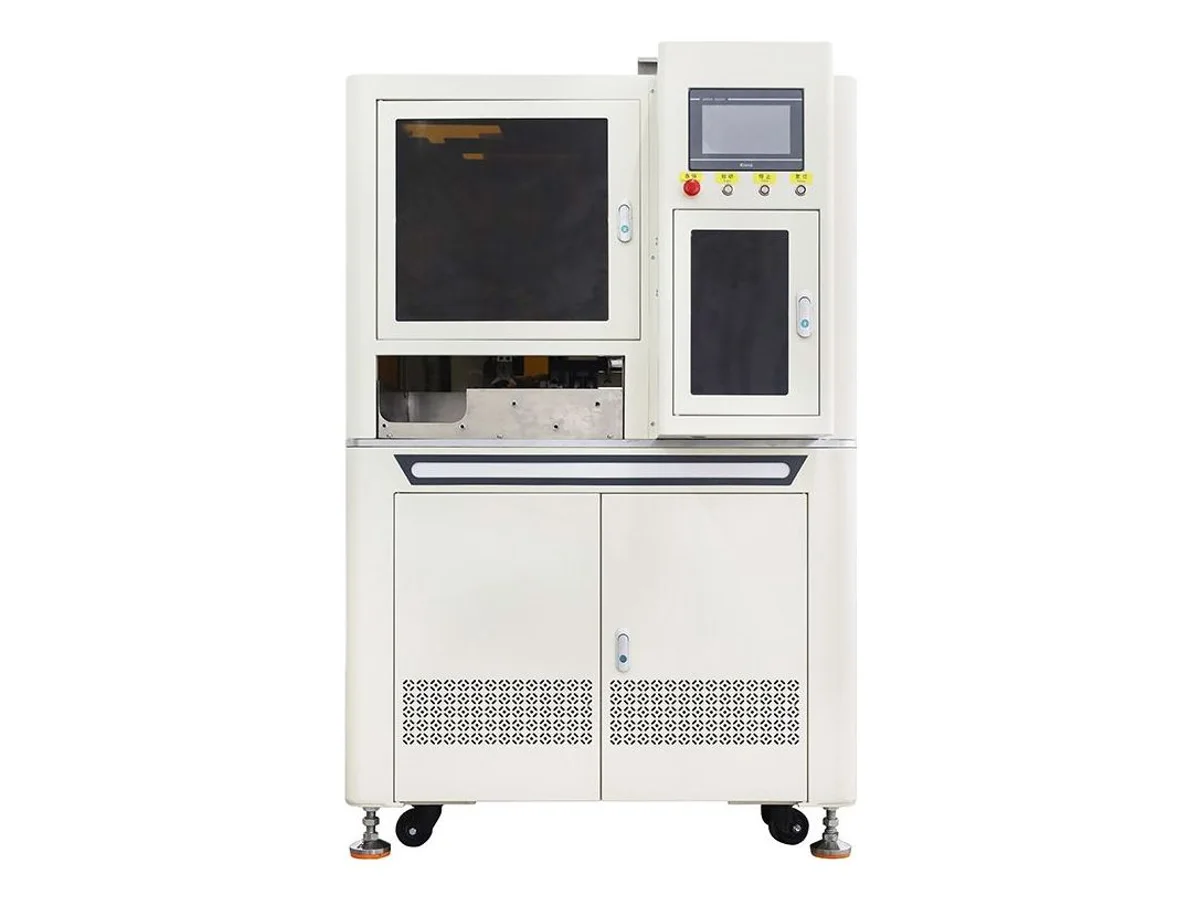
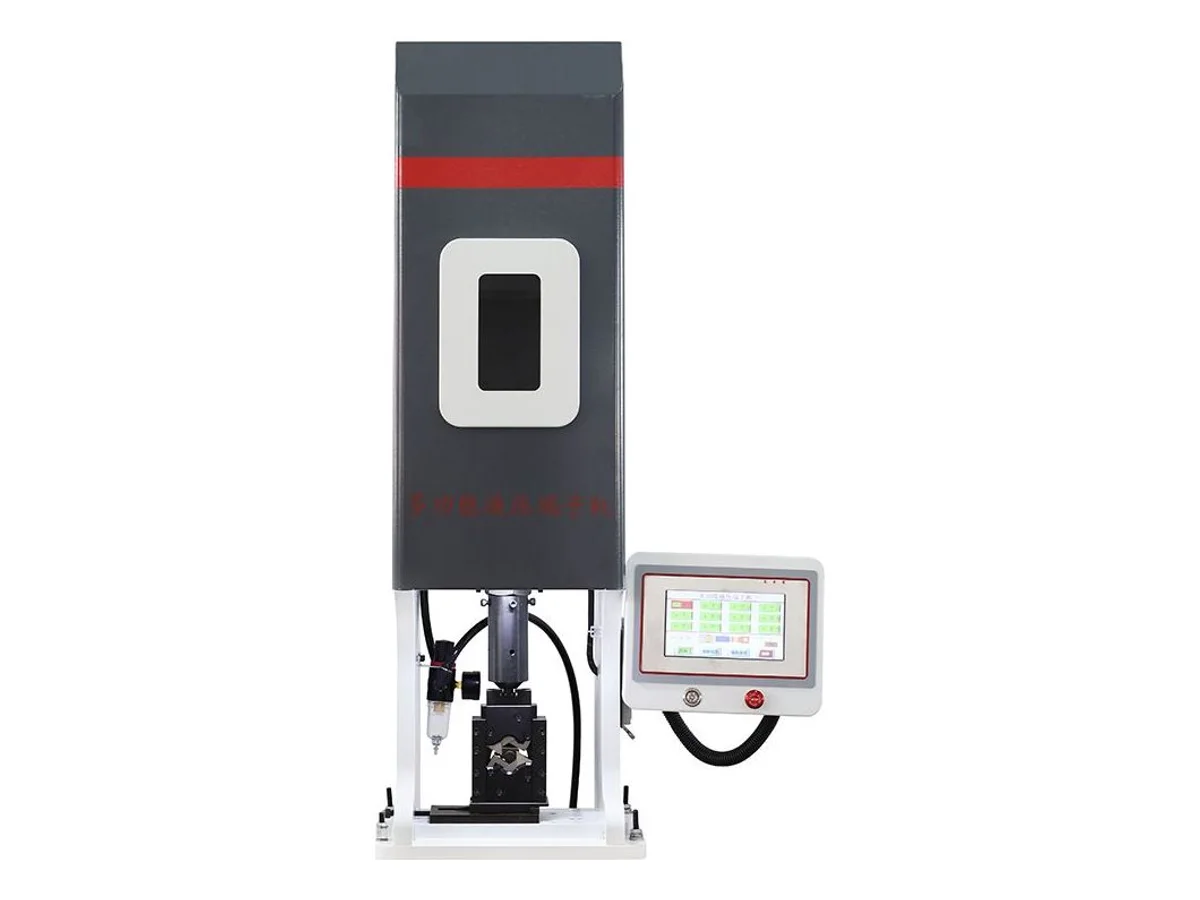
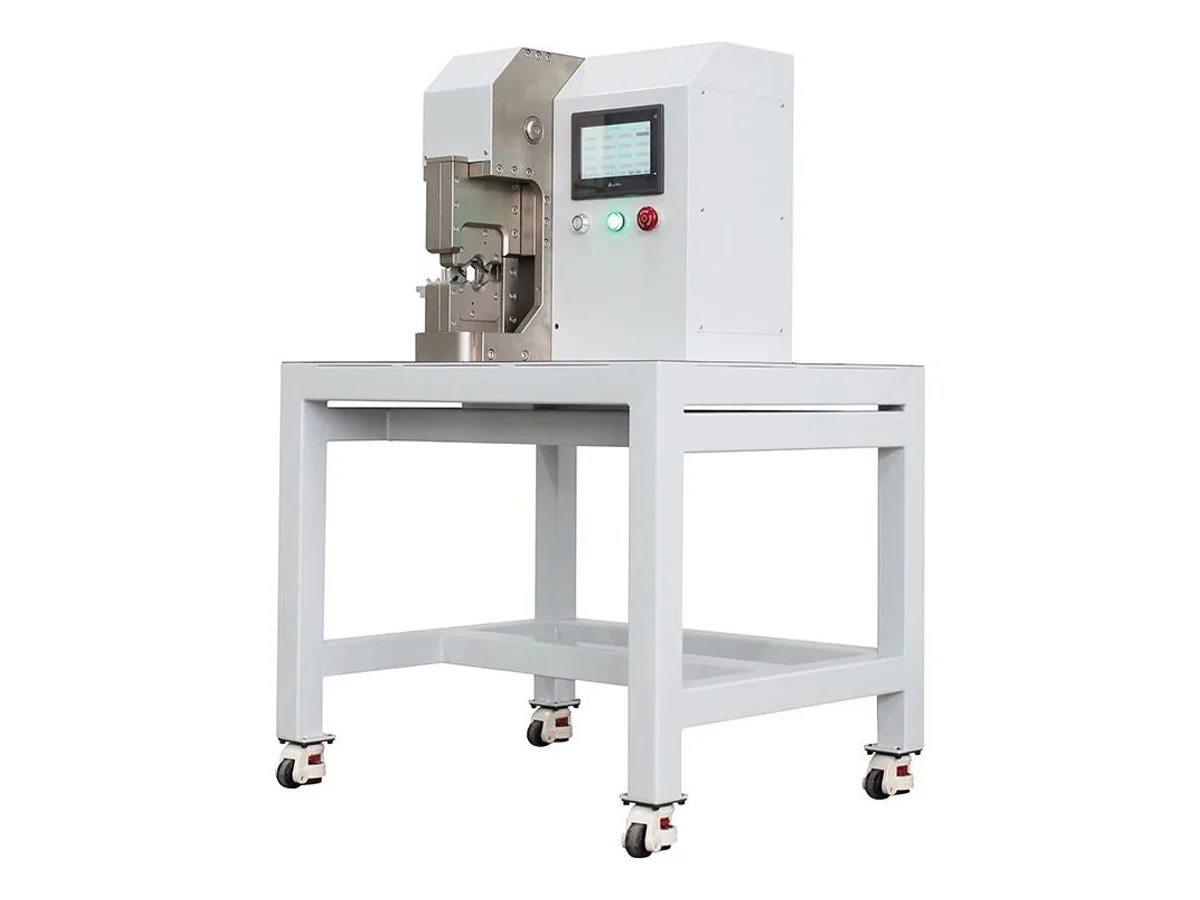
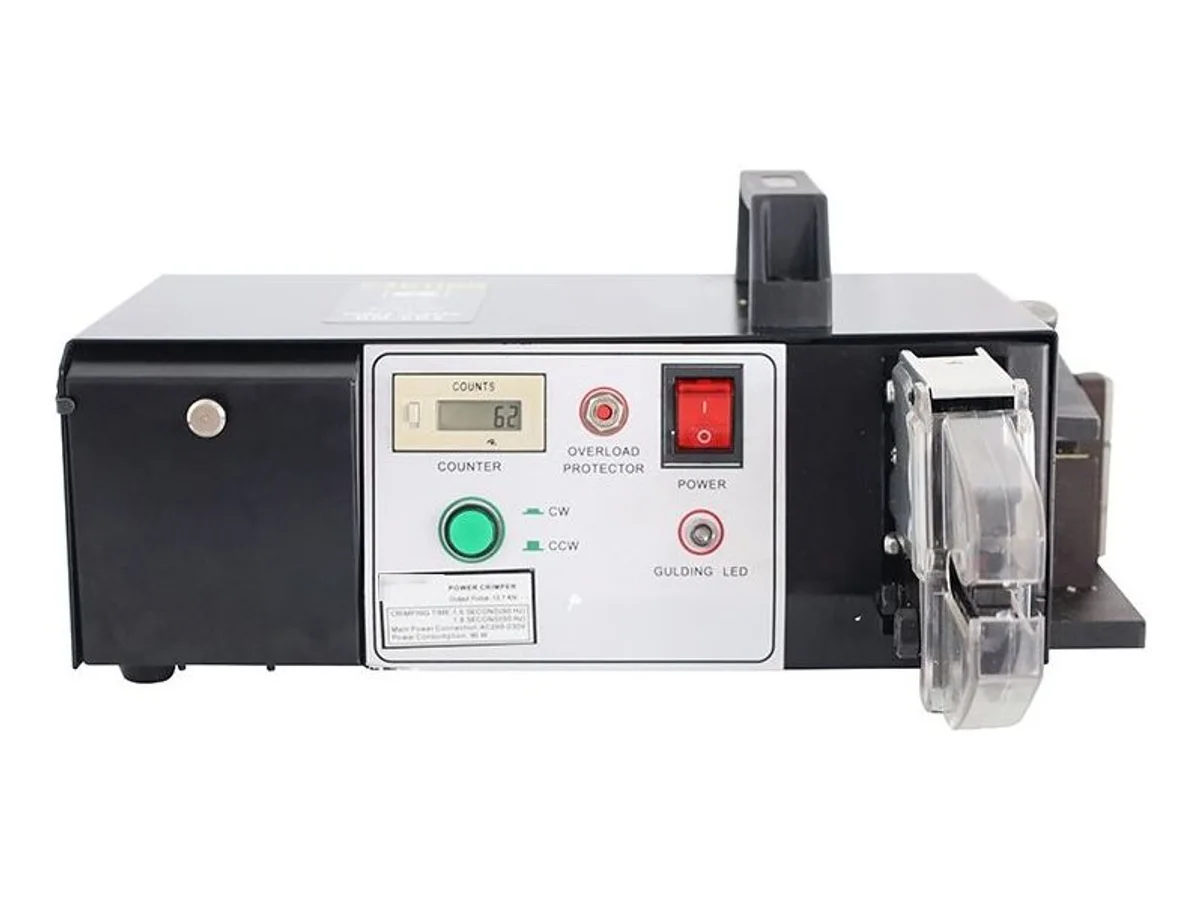
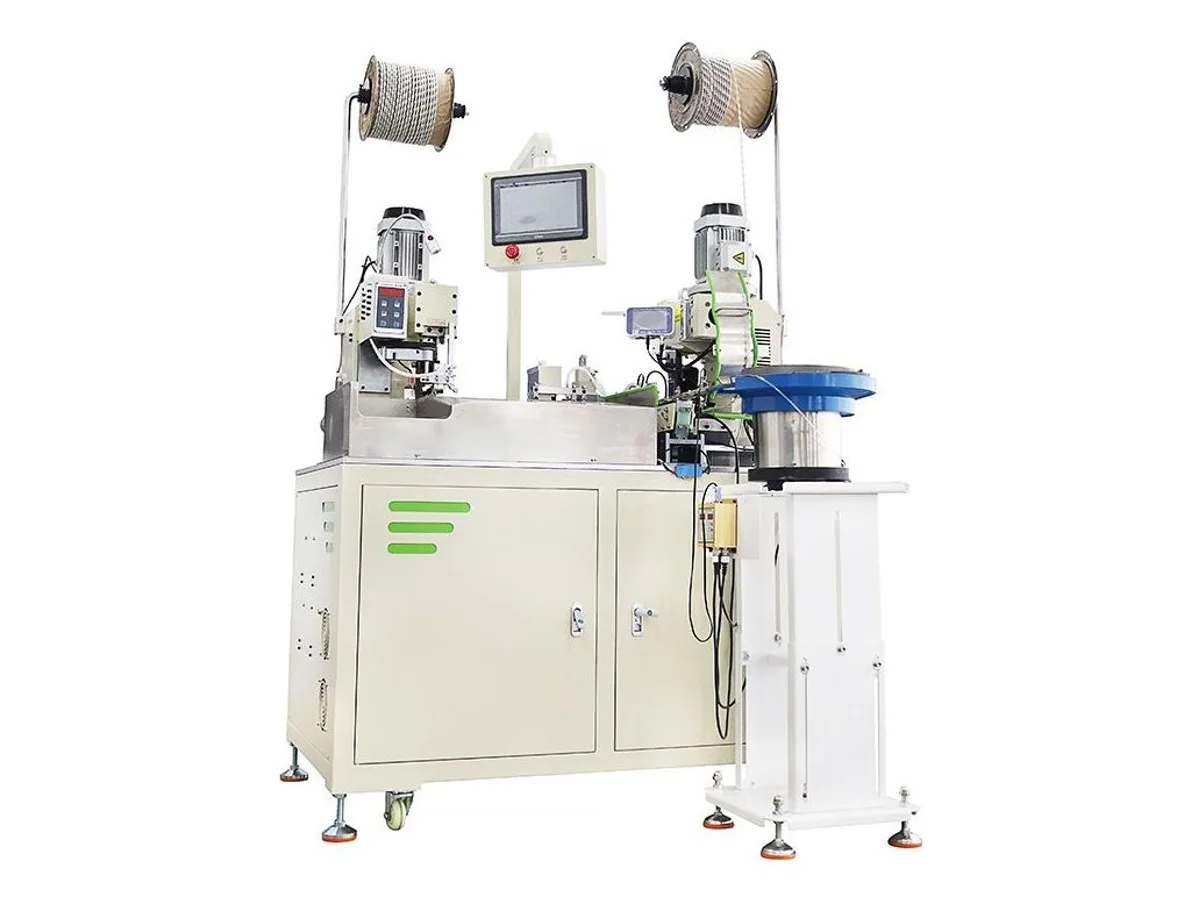
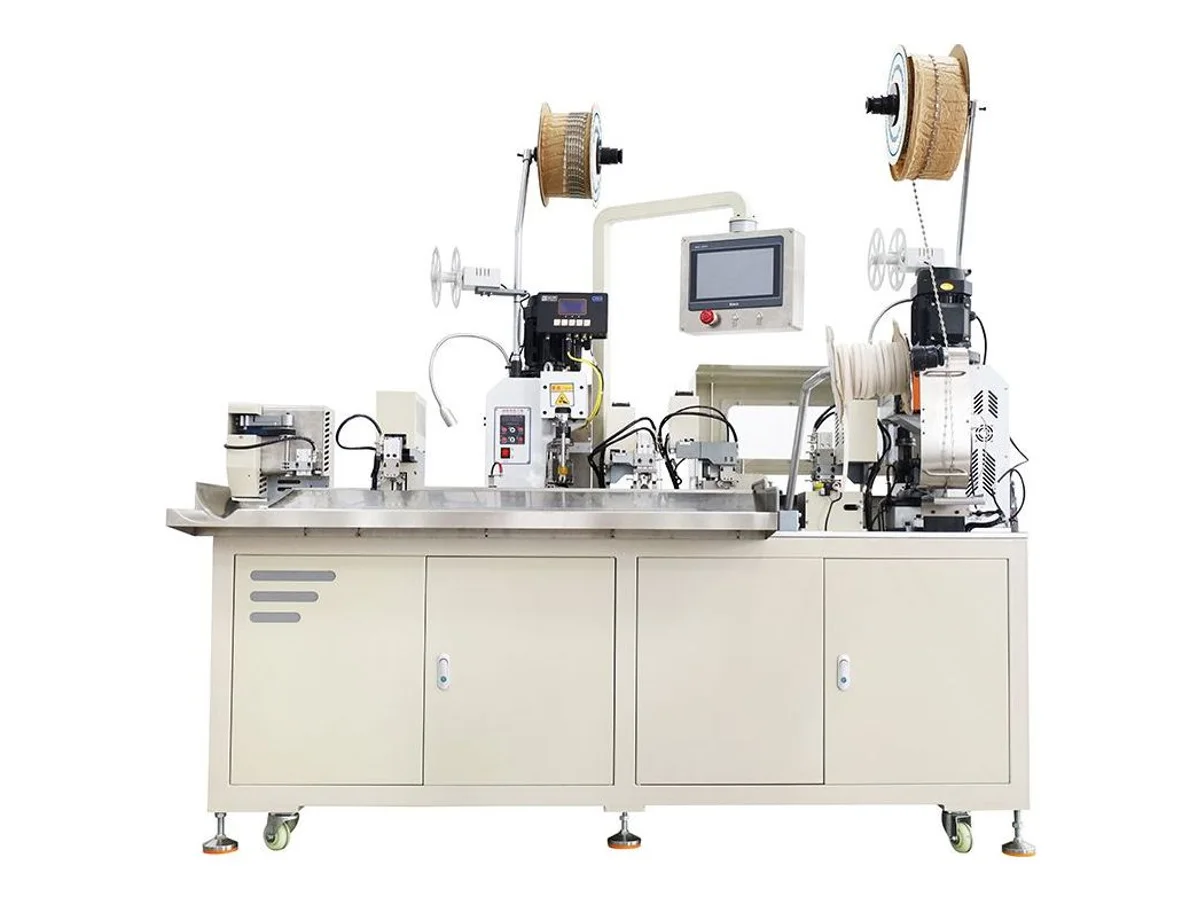
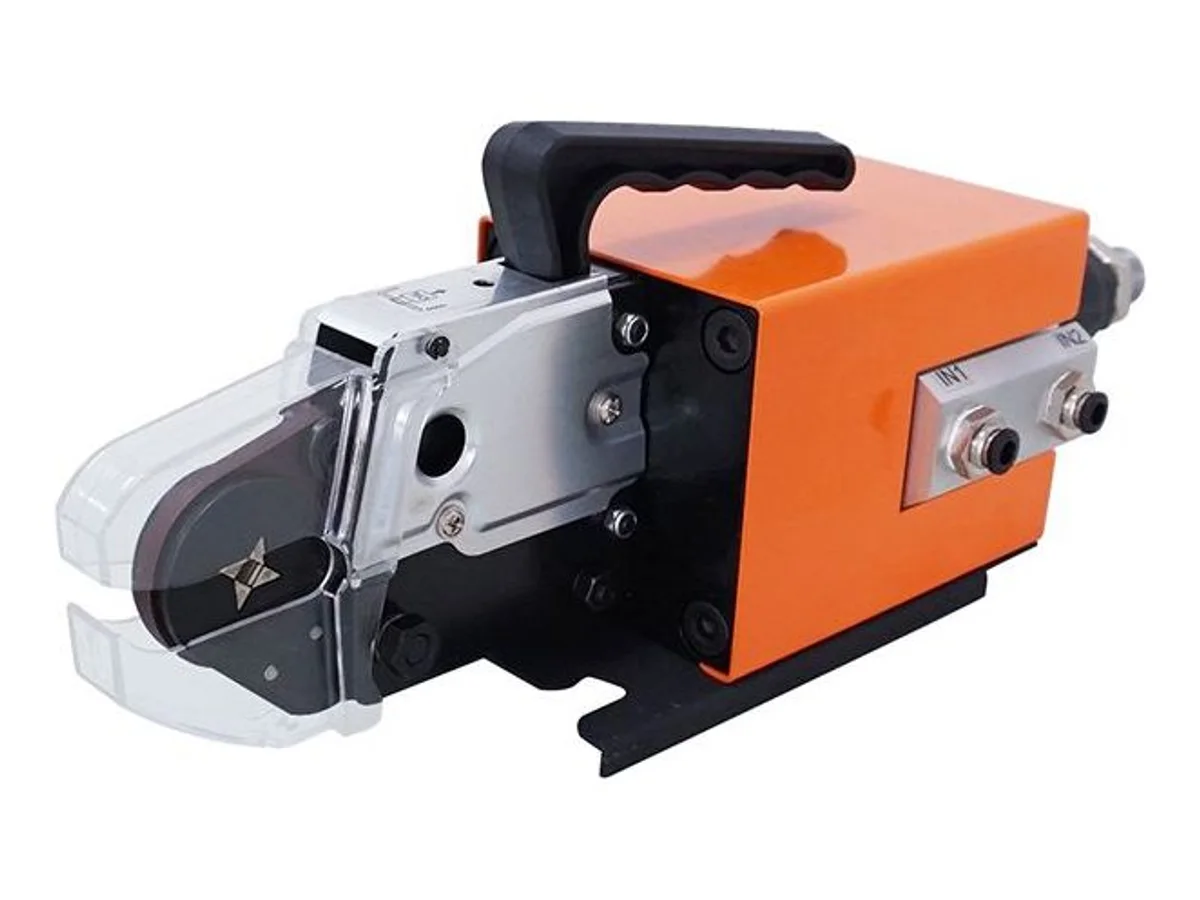
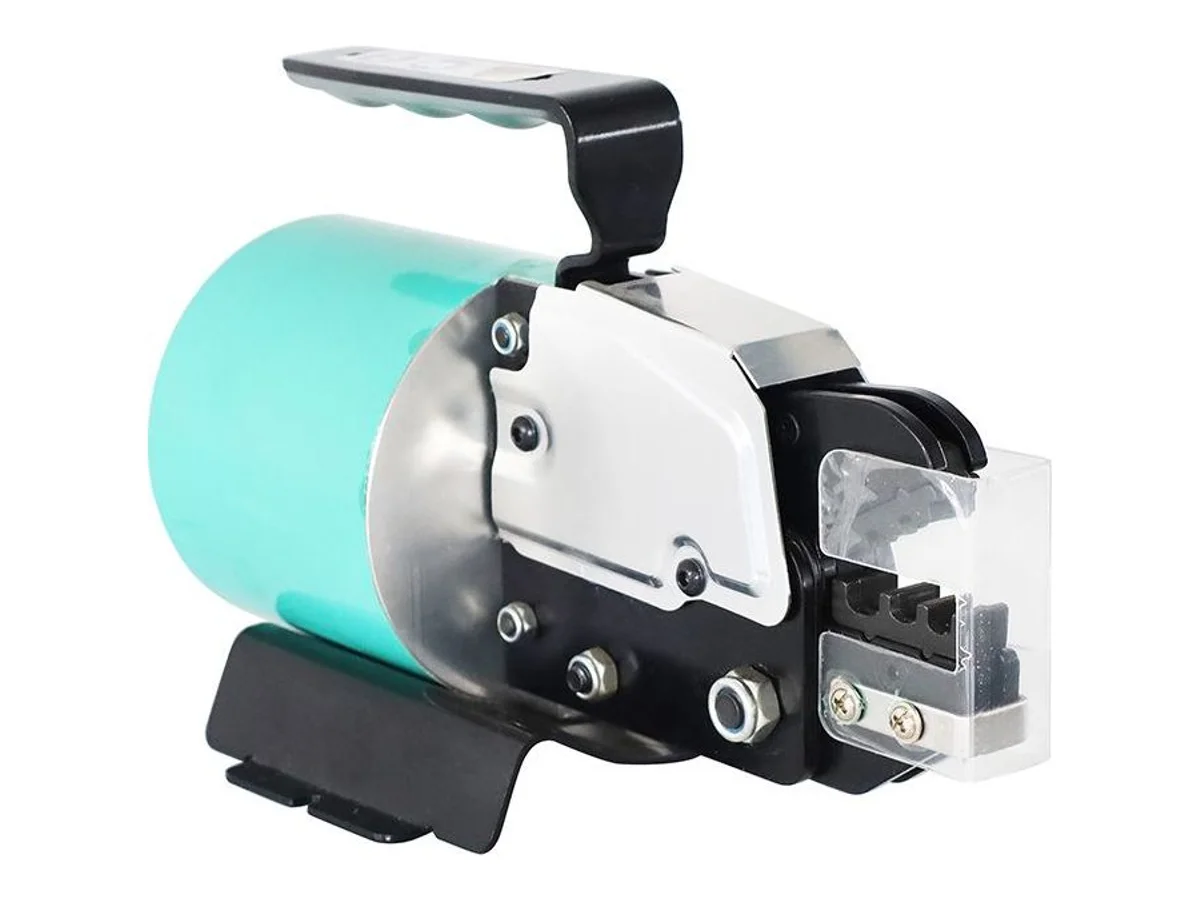
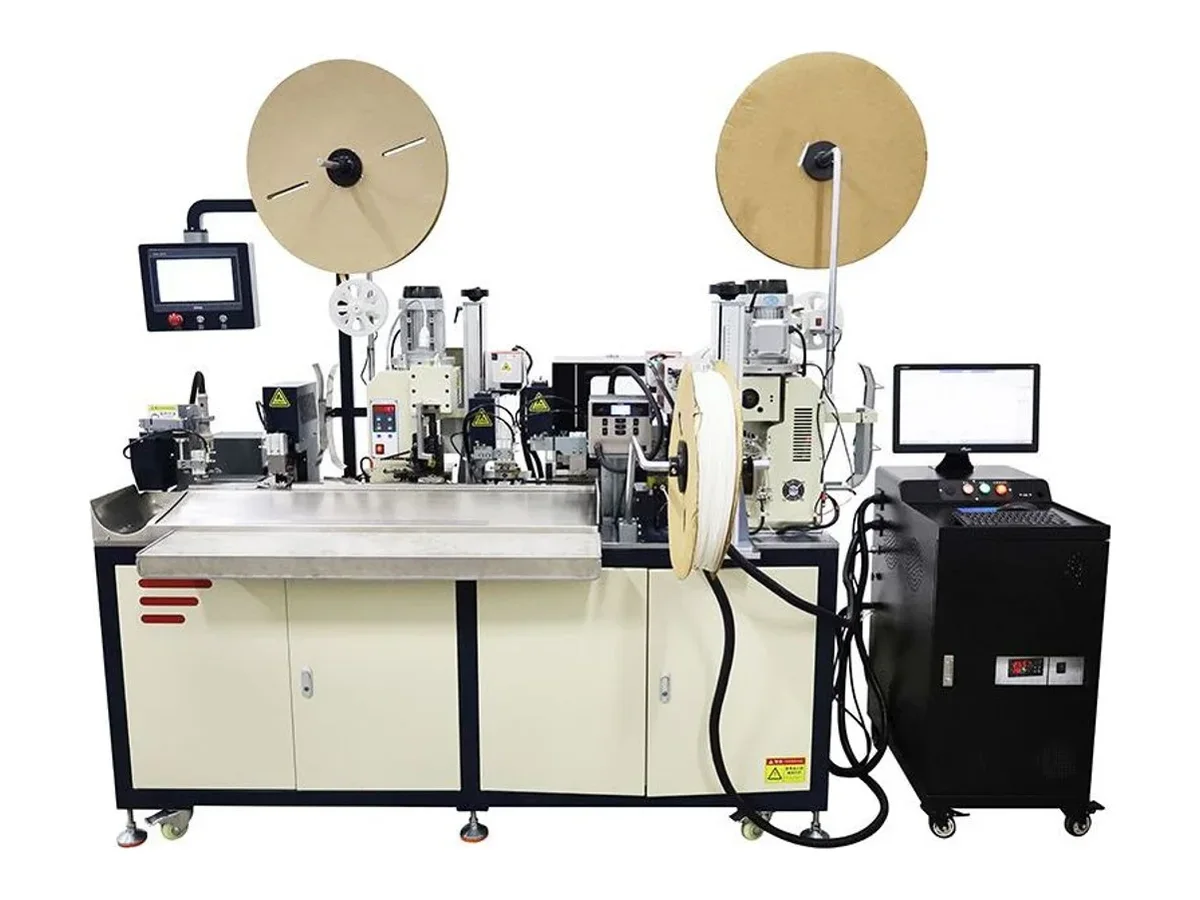
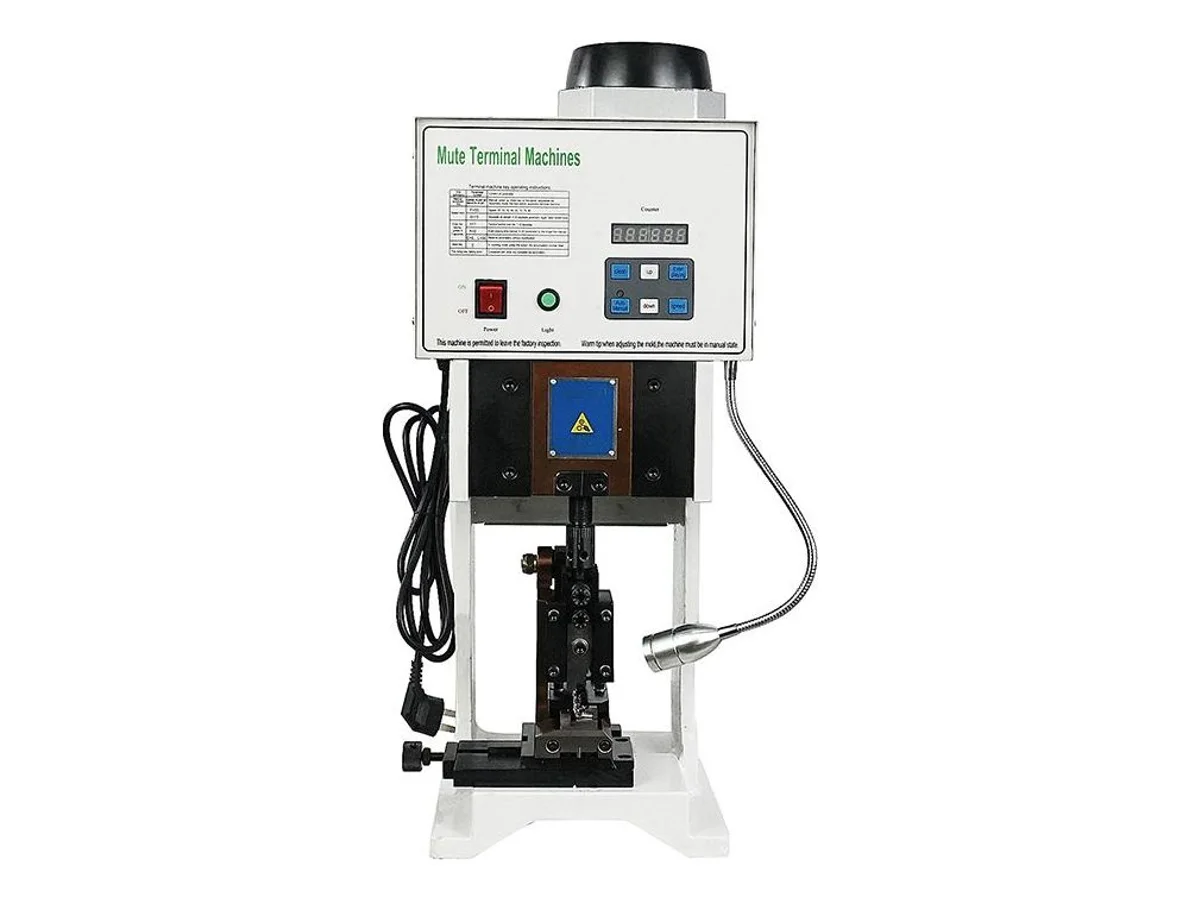
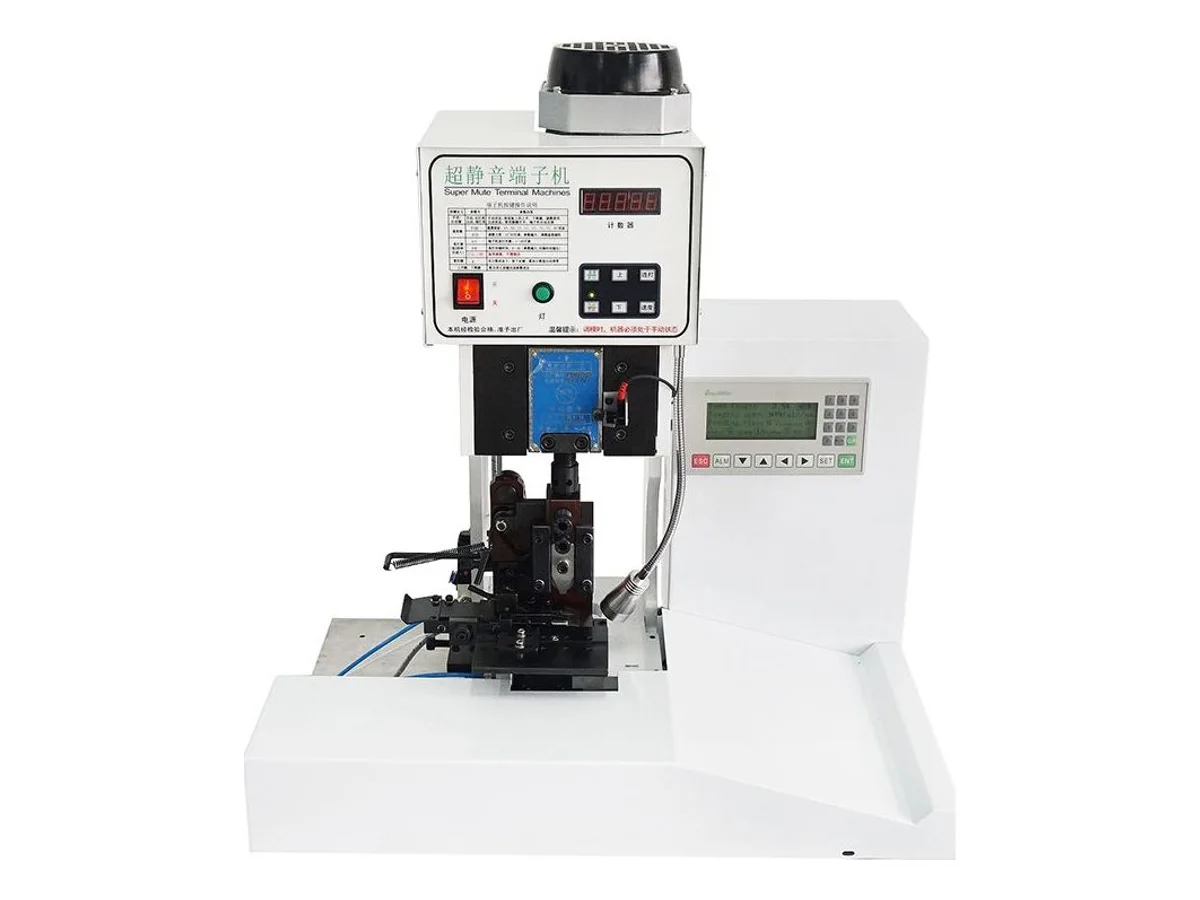
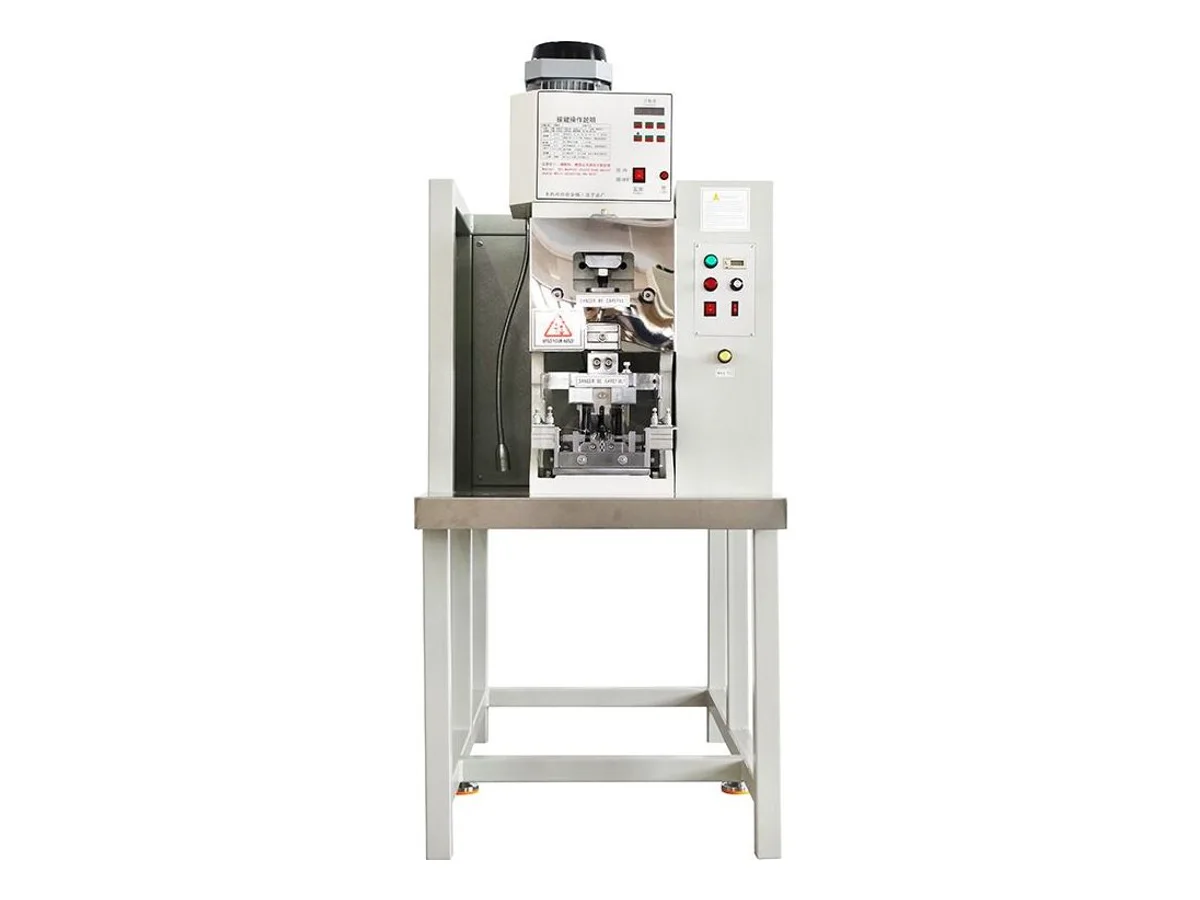
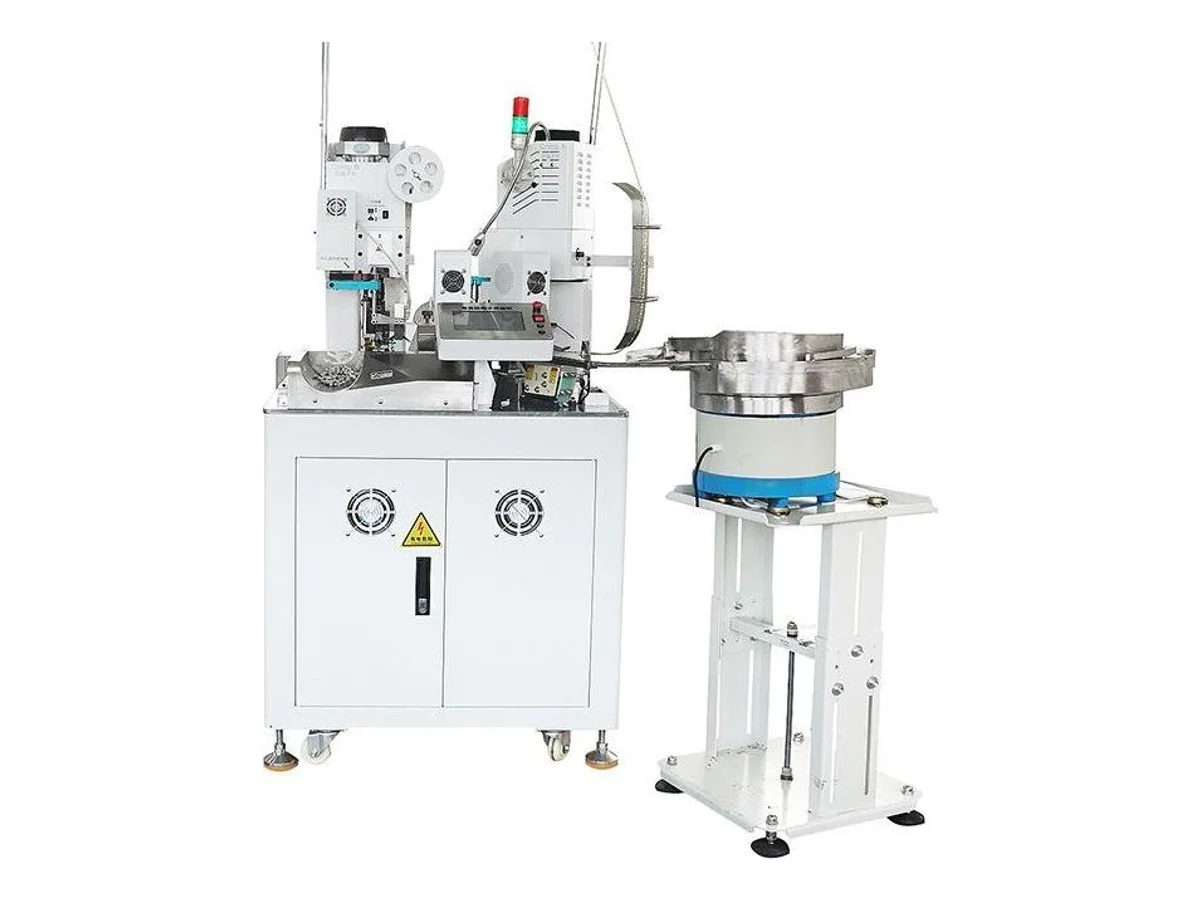
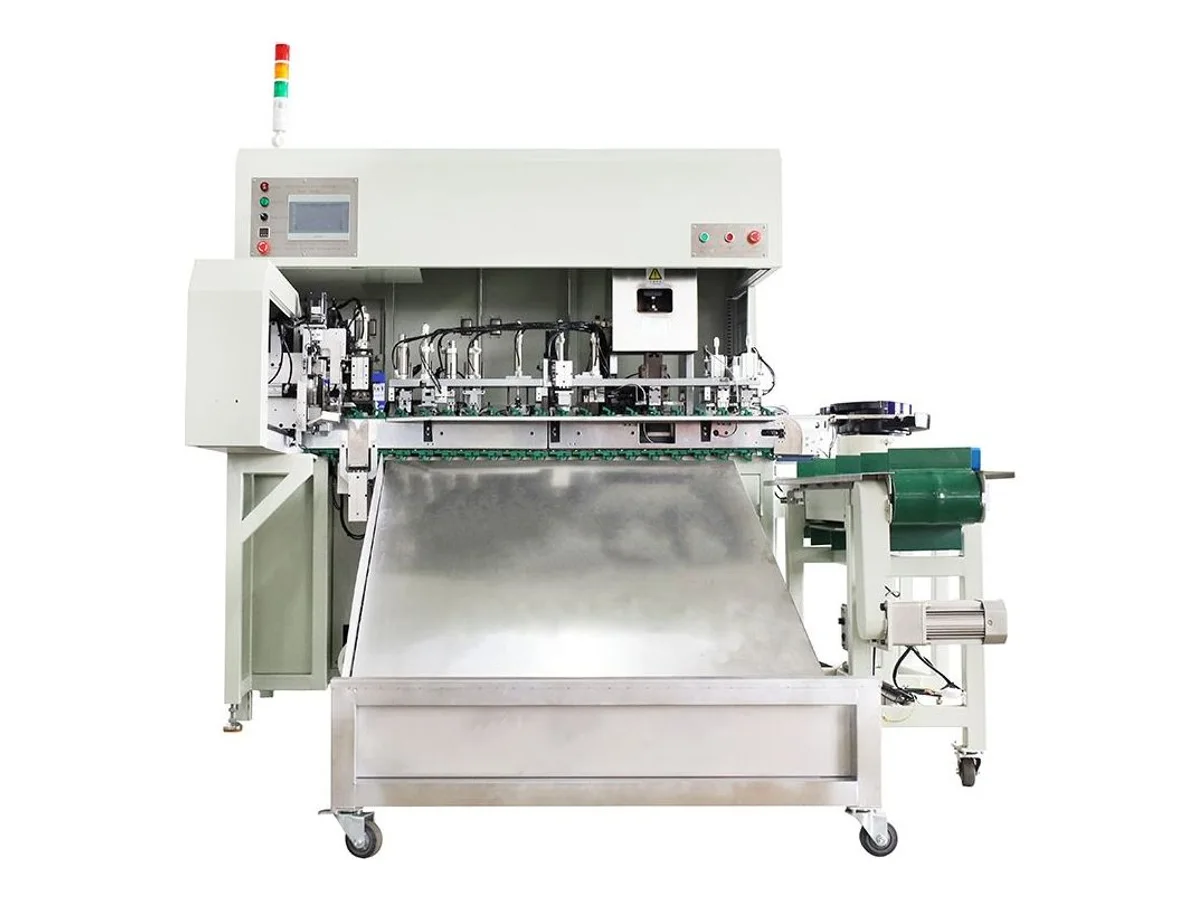
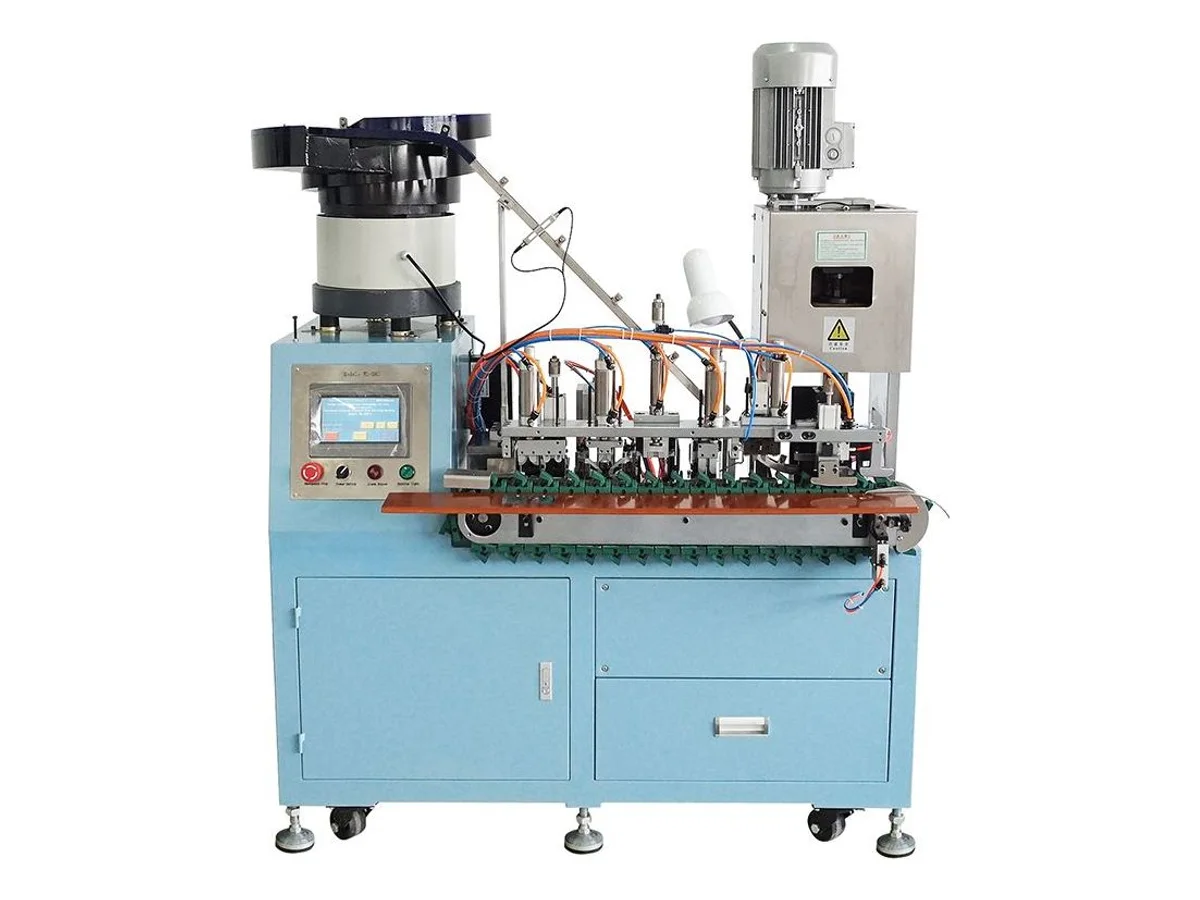
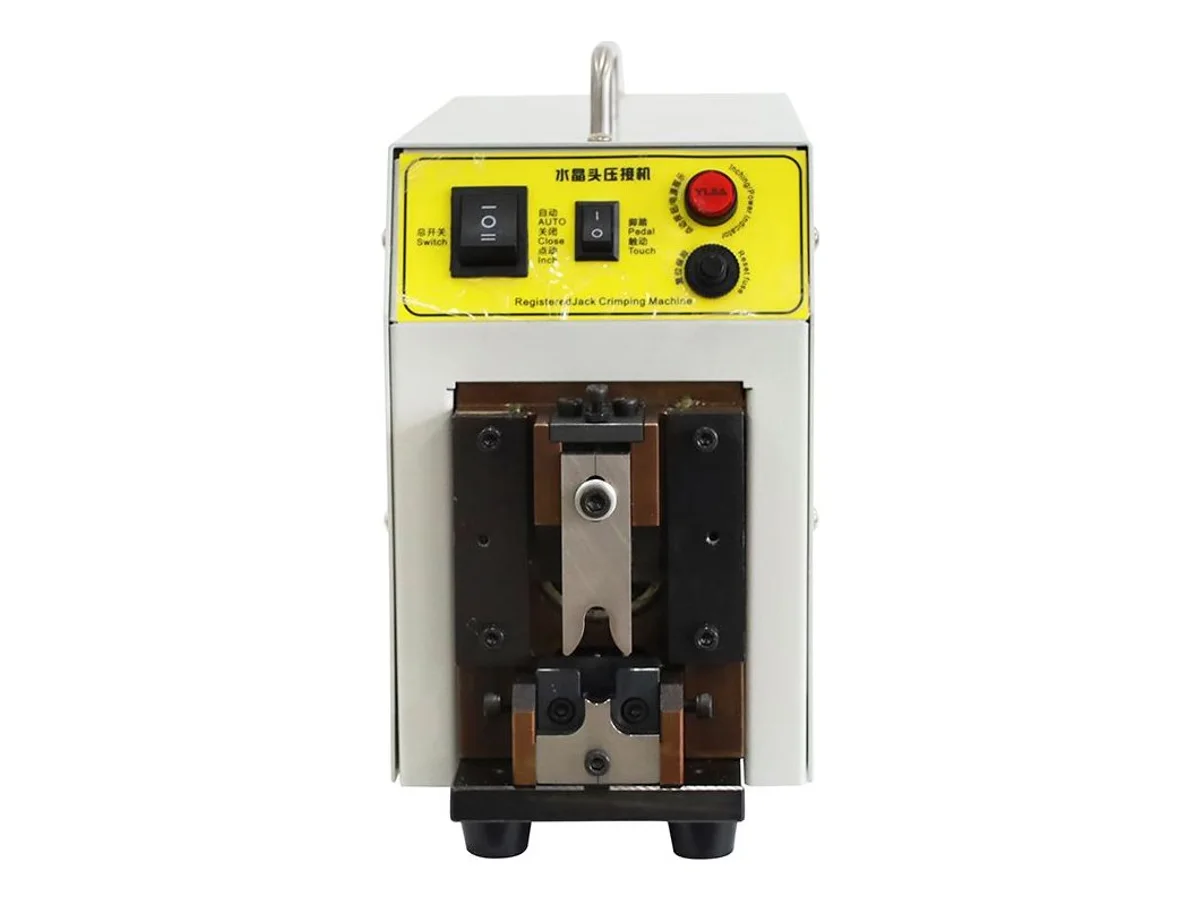
A bench press crimps whatever applicator you mount — one press, many terminals: the WM-3102T is the quiet 2-ton standard, the WM-3229 the cast-iron version, and the WM-3120BT adds stripping before the crimp. They take interchangeable applicators (Chinese 30 mm or European 40 mm stroke — the parts page explains the standards). An automatic line buys throughput: the WM-3210 crimps both ends servo-driven at 4,000–4,800 pcs/h, the WM-3202 runs 3,800+, the WM-392 feeds five wires for ≈5,000 pcs/h, and the WM-3215 places 15,000 terminals per hour on flat ribbon. Lug crimping is a force problem, not a speed problem: the WM-3218 presses 13 tons hydraulically for lugs to 75 mm², the WM-3234 crimps EV charging cable at 10 or 20 tons up to 120 mm², the WM-3240 makes servo-controlled hexagonal crimps on 10–120 mm², and the WM-3135T tops out at 35 tons. In between sit the portable tools: the WM-3238 (pneumatic, 2 kg, 0.25–6 mm²) and the WM-3239 (electric, mains-only, 0.25–10 mm²).
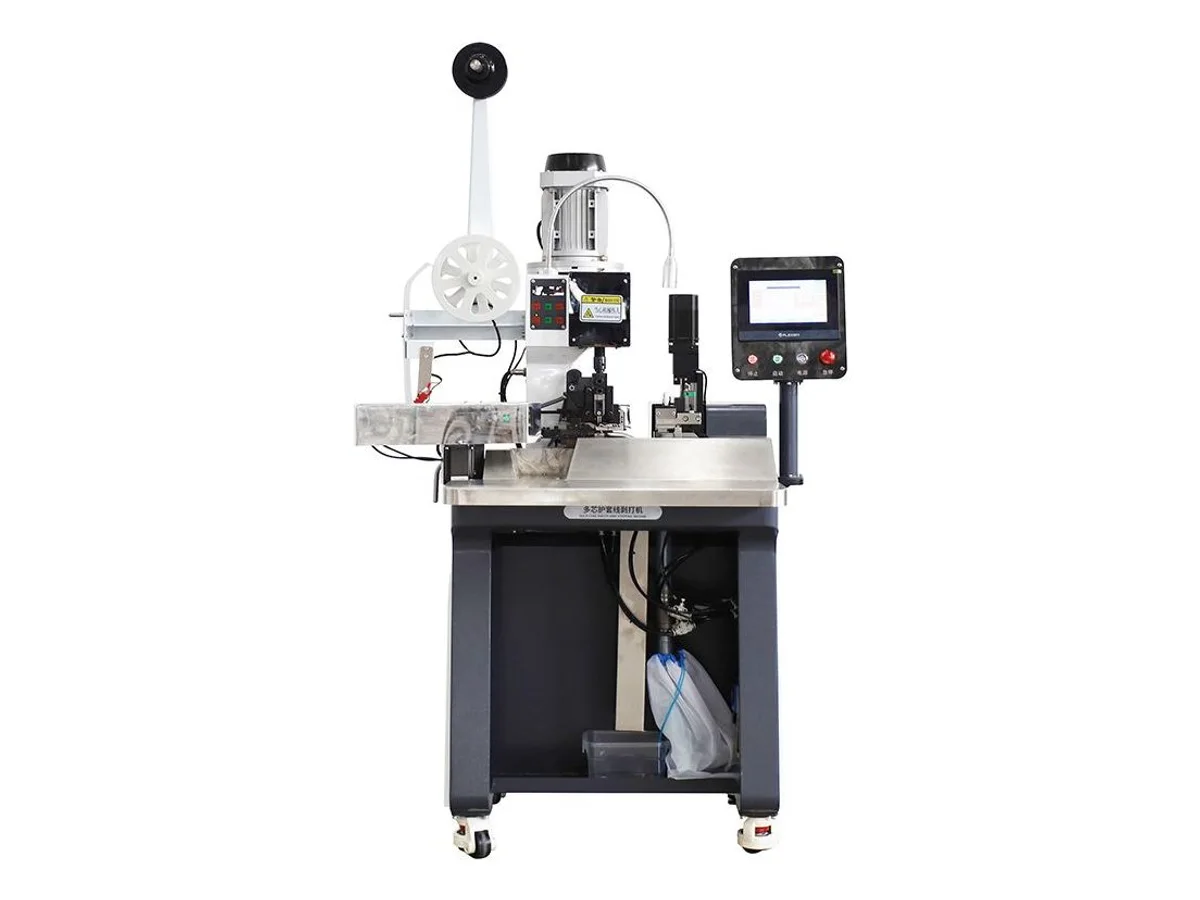
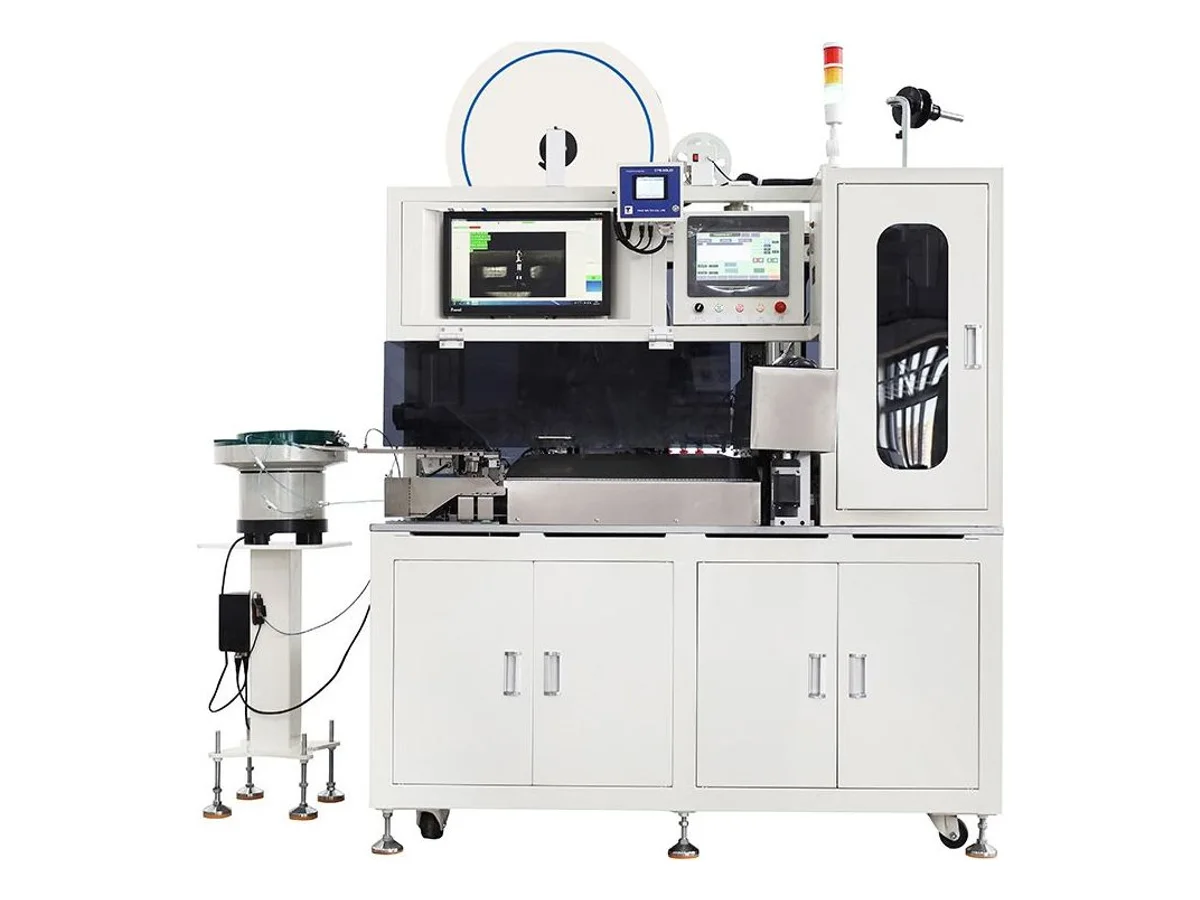
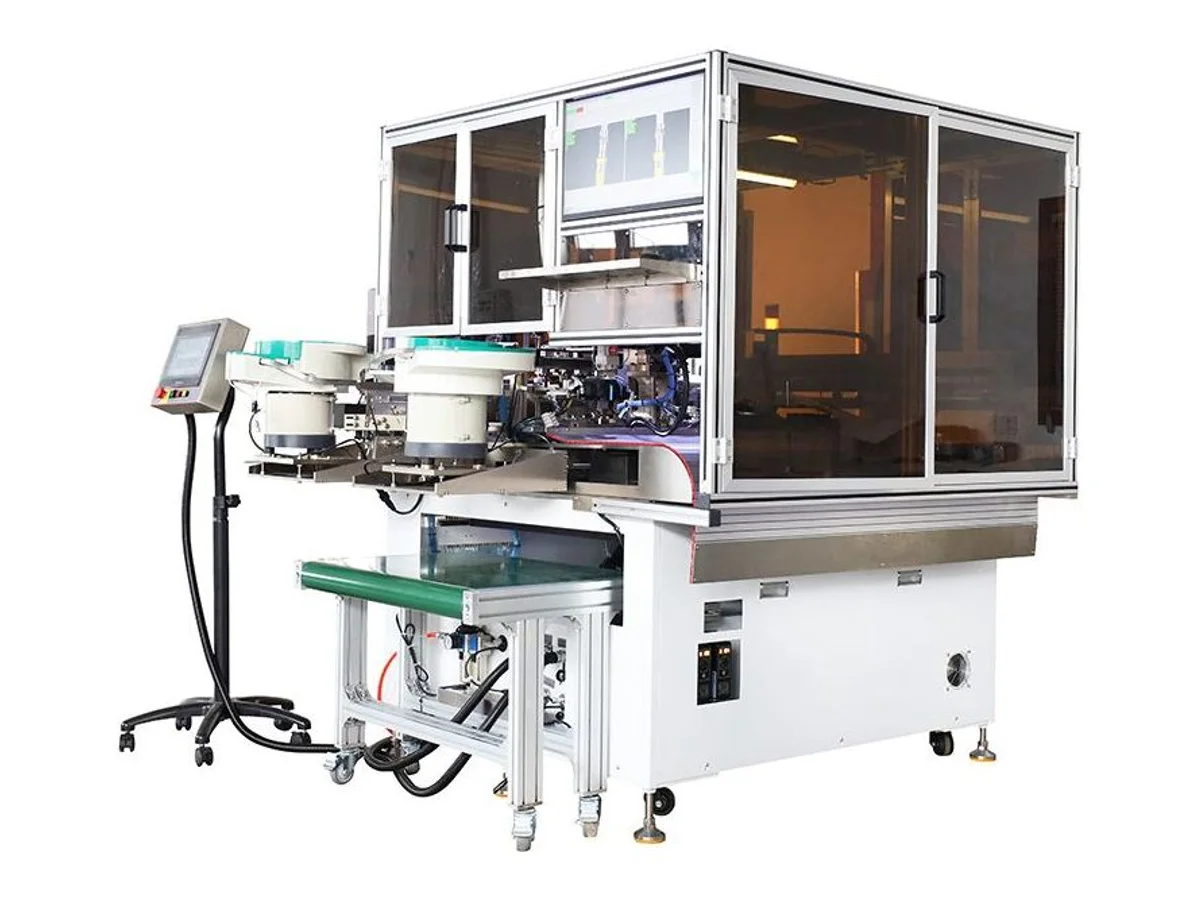
Ferrules (bootlace ends for screw terminals) have their own machines because the tooling differs from open-barrel terminals: the WM-3103 crimps loose ferrules of 0.35–4 mm² in 2.5 s, the WM-3116 spans 0.3–16 mm², the WM-397 runs e-tube ferrules at 1,000–1,300 pcs/h. Rubber seals must go on before the crimp: the WM-377 inserts seals and crimps both ends at 3,000 pcs/h, the WM-3222 strips, seats the seal and crimps semi-automatically, the WM-3231 places seals up to 13 × 14 mm at 60 cycles/min. Housing insertion finishes the job: the WM-362S crimps and inserts single-ended at 2,200 pcs/h, the WM-366 fills up to 6,000 cavities per hour, and the semi-automatic multi-core family — WM-3226, WM-3232, WM-3237, WM-3236 — takes sheathed cable through core stripping, crimping and insertion, up to 14 cores. Cord sets close the category: a power-cord line at 800–1,200 pcs/h, European pin riveting, French plug inserts, RJ45 modular plugs.
Need to cut wire, strip it and crimp a chain-fed tubular ferrule on one end? Compare the WM-3243 cut-strip-ferrule crimping machine. Its specified output is 1,500 pieces/hour for lengths within 300 mm. Ferrule presentation and wire preparation matter: our chain-fed vs loose-ferrule guide compares the complete process and changeover questions.
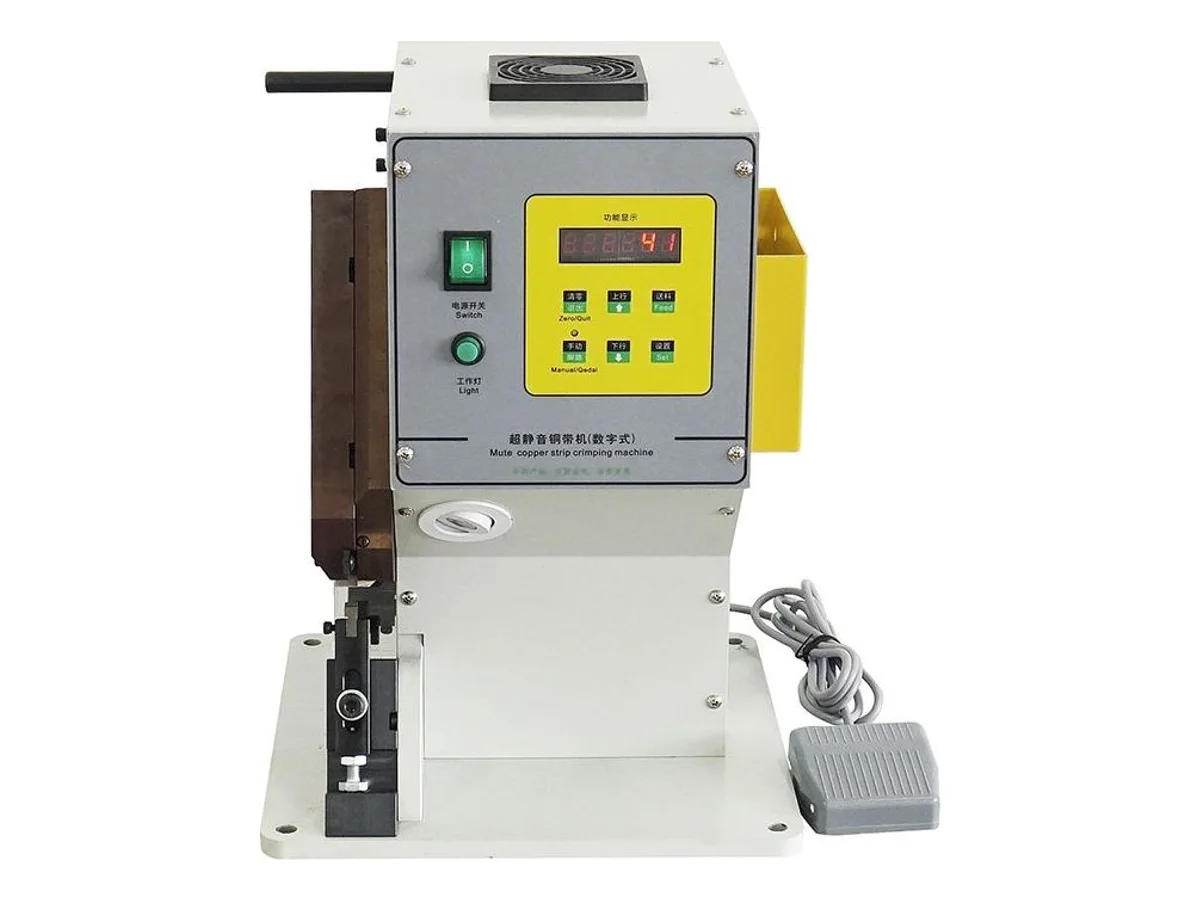
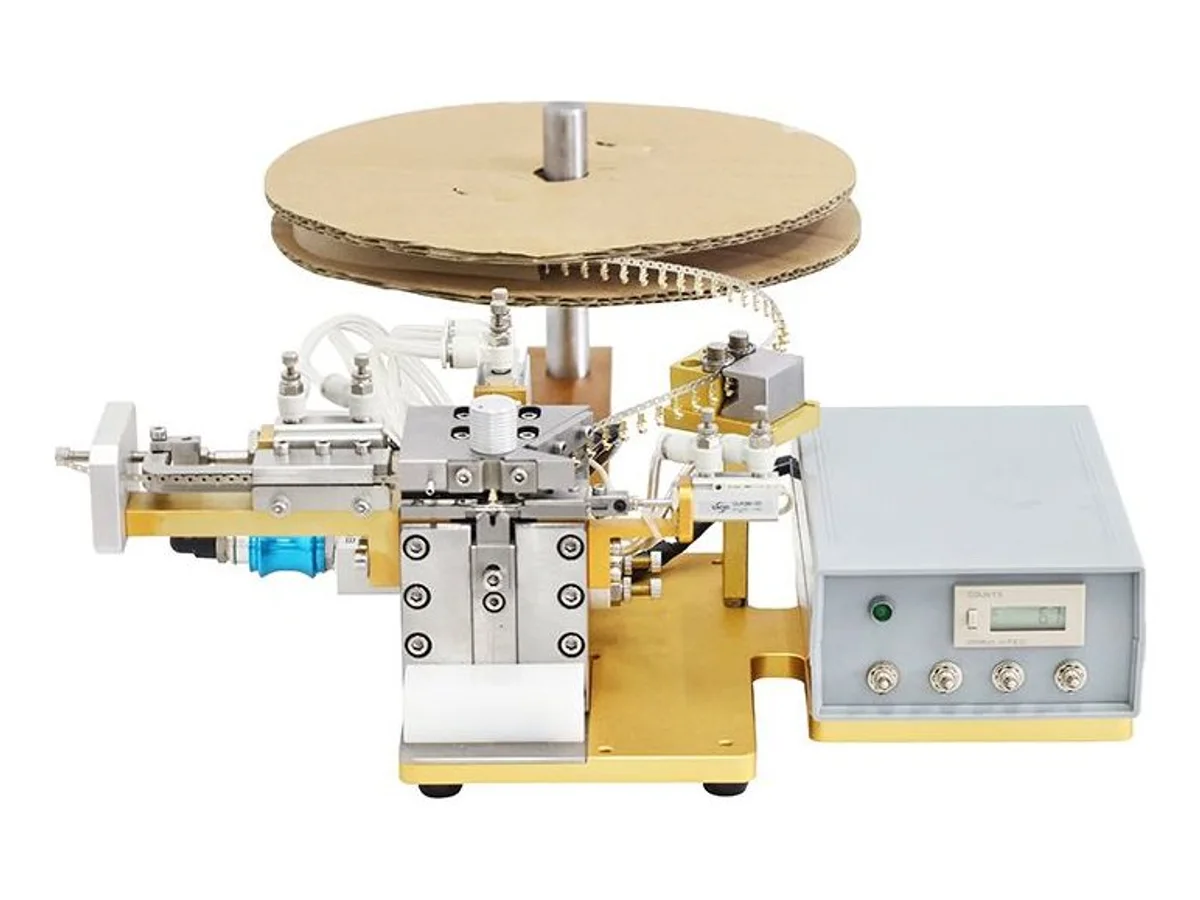
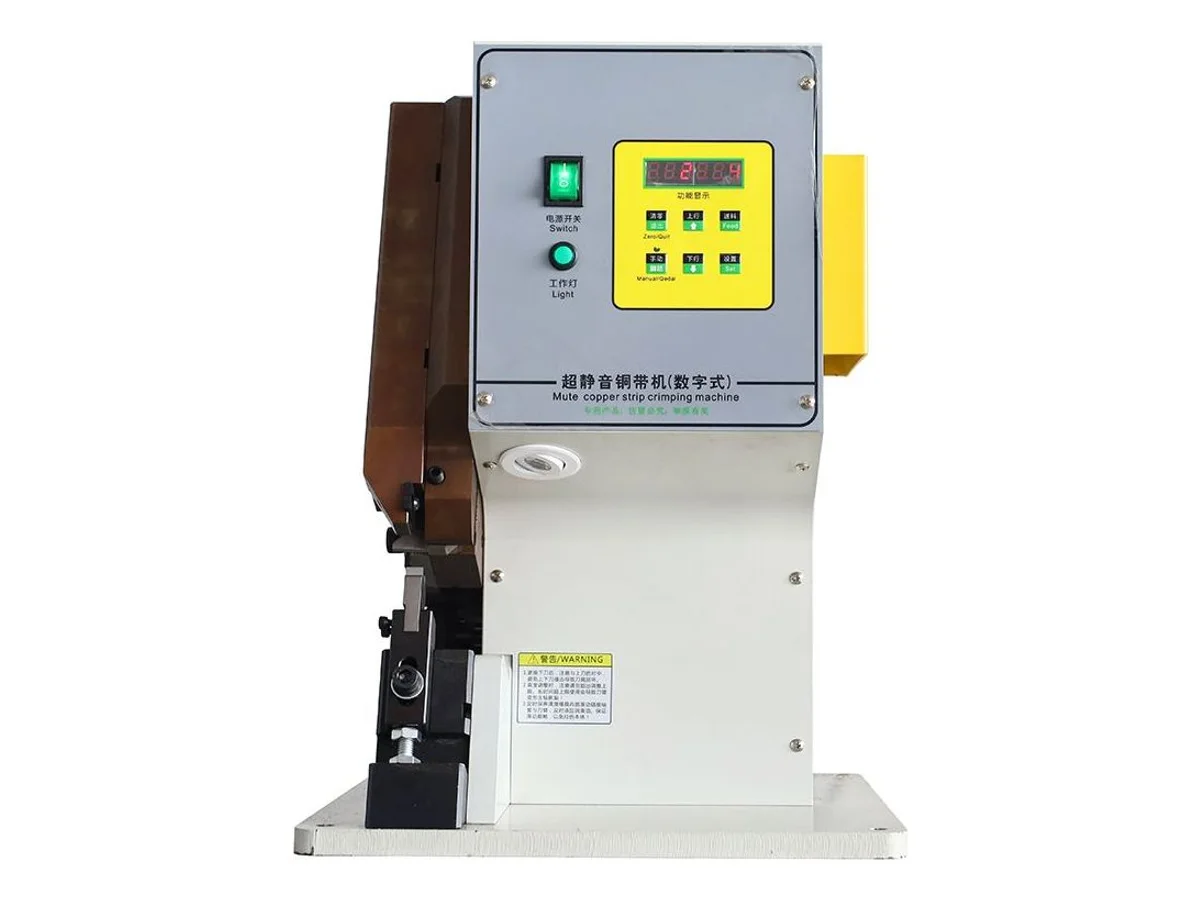
WM-715 and WM-716 feed, form and crimp copper band around the wires. Select this group for a mechanical splice; use soldering and welding equipment when the joint drawing calls for those processes.
| Machine | Segment | Range | Output / force | Pick it for |
|---|---|---|---|---|
| WM-3102T | Bench press | Interchangeable applicators | 2 T, low noise | The standard press most shops start with |
| WM-3120BT | Bench press + stripping | AWG 32–20 | 2 T | Strip and crimp at one station |
| WM-3210 | Automatic double-end line | AWG 30–14 | 4,000–4,800 pcs/h | The fast servo line |
| WM-392 | Five-wire double-end | AWG 18–32 × 5 | ≈5,000 pcs/h | Parallel wires, parallel output |
| WM-3215 | Ribbon-cable crimping | 3–20 pin flat ribbon | 15,000 terminals/h | The highest terminal count here |
| WM-3225 | Double-end + sleeve insert | AWG 12–32 | 3,000 pcs/h | Crimp plus soft sleeve in one line |
| WM-377 | Seal insertion + crimp | AWG 28–16 | 3,000 pcs/h | Waterproof connectors at volume |
| WM-3222 | Strip + seal + crimp, semi-auto | Wire OD 1.0–4.0 mm | 1,200–1,500 pcs/h | Seals without a full line |
| WM-362S | Crimp + housing insertion | AWG 28–20 | 2,200 pcs/h | From wire to filled connector |
| WM-366 | Housing insertion | AWG 30–18 | ≤6,000 holes/h | Filling cavities at line speed |
| WM-3232 | Multi-core semi-auto | 2–14 cores, AWG 22–30 | 1,000–1,300 pcs/h | Sheathed cable to crimped cores |
| WM-3103 | Ferrule crimping | 0.35–4 mm² loose ferrules | 2.5 s/pc | Bootlace ends for control cabinets |
| WM-3116 | Ferrule, wide range | 0.3–16 mm² | ≈4 s/pc | The big-ferrule bench machine |
| WM-3238 | Portable, pneumatic | 0.25–6.0 mm² | 1.3 T, 2 kg | Crimping that travels to the harness |
| WM-3239 | Portable, electric | 0.25–10 mm² | 12.7 kN, mains only | No compressor needed |
| WM-3218 | Hydraulic lug crimping | Lugs 0–75 mm² | 13 T | Power lugs, guided dies |
| WM-3234 | EV cable lug crimping | 1–70 / 6–120 mm² | 10 T / 20 T | Charging-gun cable terminations |
| WM-3240 | Servo hexagonal lug | 10–120 mm² | 20 T class, servo | Hex crimps with programmed force |
| WM-361C | Power cord line | 2-pin plugs | 800–1,200 pcs/h | Cord sets end to end |
Compare the full batch: wire preparation, loading, setup, terminal replenishment, inspection and accepted output. A short machine cycle is not the same as sustained production. Use your recurring part numbers and changeover frequency to compare configurations in our automatic vs semi-automatic selection guide, then confirm performance with a sample run.
Ordinary open-barrel terminals on wire to about 6 mm² crimp comfortably at 2 tons — the standard bench class. Force requirements jump with lugs: published pairings here are 13 T for lugs to 75 mm² (WM-3218), 10–20 T for EV cable to 120 mm² (WM-3234), servo-controlled hex crimping on 10–120 mm² (WM-3240), and 35 T at the top (WM-3135T). Buying force you do not need buys you nothing — the terminal and wire decide.
No — ferrule (bootlace) tooling forms a square or trapezoid gas-tight sleeve rather than an open-barrel wrap, so the machines are separate: the WM-3103 crimps loose ferrules of 0.35–4 mm² in 2.5 seconds, the WM-3116 spans 0.3–16 mm², and the WM-397 feeds e-tube ferrules at 1,000–1,300 pcs/h.
Yes, at two levels. In-line: the WM-377 threads the seal and crimps both ends at 3,000 pcs/h; the WM-3225 adds soft-sleeve insertion. Semi-automatic: the WM-3222 strips, seats the seal and crimps; the WM-3231 places seals to 13 × 14 mm at 60 cycles/min; and for housings, the WM-362S and WM-366 insert crimped wires into cavities at up to 6,000 holes per hour.
The terminal drawing or 20–30 cm of the reel strip, the wire specification, whether seals or housings are part of the operation, and target pieces per hour. Applicator standard matters for presses — say what press you run, or read the applicator guide on our parts page. Then courier terminal and wire samples: we crimp them on the actual machine and send the video with crimp-height measurements before you order.
The quotation depends on the operations required, wire and terminal combination, matched applicator or dies, feeding arrangement, detection and sample-validation requirements. Send your terminal drawing, wire specification and email address. Our engineering team and business specialists will contact you within 12 hours with a quotation proposal. Every quote lists wear parts with unit price and the location they ship from.
Engineering guidance for choosing this process and correcting the defects that affect finished-wire quality.
Selection guide
Plan wire harness production from the drawing: cutting, stripping, seals, crimping, housing insertion, taping and final electrical checks.
Read engineering guide →Troubleshooting guide
Diagnose rolled, torn, missing or misplaced wire seals by separating part fit, feeding, insertion and crimping checks.
Read engineering guide →Troubleshooting guide
Find why a crimped terminal backs out of its connector housing. Check part matching, orientation, crimp shape, primary retention and secondary locks.
Read engineering guide →Selection guide
Build a crimp quality plan that combines force monitoring, pull testing, crimp-height measurement and cross-section analysis without confusing their limits.
Read engineering guide →Selection guide
Prepare wire samples, drawings and acceptance criteria for a useful machine trial. Record quality, accepted output and changeover without relying on a demo clip.
Read engineering guide →Selection guide
Choose a terminal crimping machine by terminal presentation, wire range, applicator standard, required process steps, inspection method and production mix.
Read engineering guide →Selection guide
Compare automatic lines and semi-automatic wire-processing cells using batch size, changeover, process integration, inspection and labor content.
Read engineering guide →Troubleshooting guide
Troubleshoot low pull force, incorrect crimp height, strand loss, bellmouth defects, insulation support problems and inconsistent terminal feeding.
Read engineering guide →Troubleshooting guide
How to specify minimum strip length, distinguish a programmable setting from an achieved result, and verify the required preparation against the terminal drawing.
Read engineering guide →Troubleshooting guide
Two bags of terminals marked 22 AWG can need different dies. What decides the match — barrel shape, insulation crimp, tab geometry — how to send terminals for a die fit, and how many crimps a year justify a press instead of a hand tool.
Read engineering guide →Troubleshooting guide
Compare chain-fed and loose-ferrule crimping machines by wire preparation, changeover, terminal fit and batch output. Check WM-3243 and WM-3246 specifications.
Read engineering guide →Troubleshooting guide
Delivery checks cover the supply voltage, interface language, transport condition, operating manual and replacement wear parts. What we set before shipment, and what to check in the first hour.
Read engineering guide →