Heat Shrink Tube Inserting, Marking and Shrinking Machine with 2.5-Second Cycle WM-669
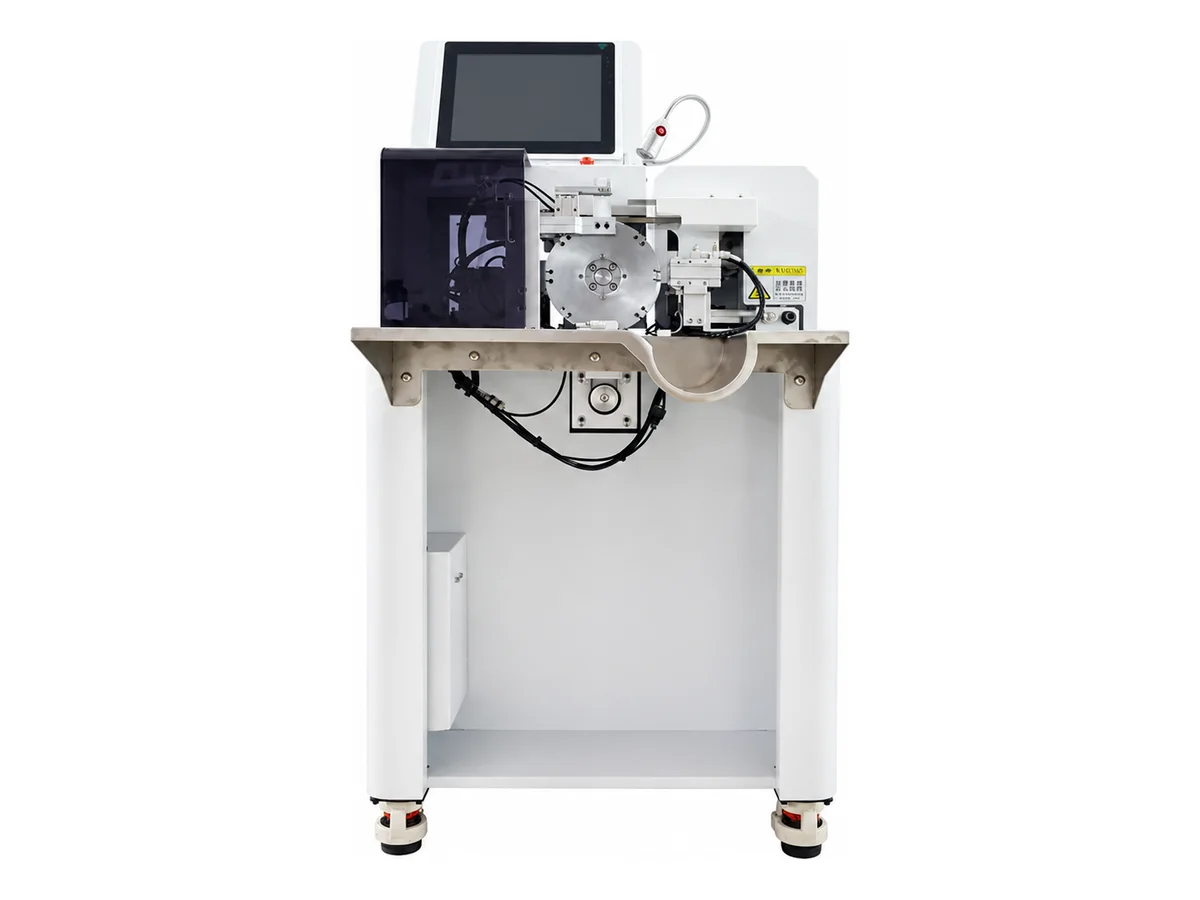
The WM-669 slides a cut shrink tube onto the wire, prints the legend on it and shrinks it in place — inserting, marking and heating combined into a 2.5-second cycle. It takes tube of Φ2.0 mm/Φ6.0 mm diameter, heats a 6 – 35 mm zone selected by fixture, and holds any shrink temperature from 0 to 380 °C under thermostat control. A built-in printing unit marks the sleeve before it shrinks, the 12-inch multi-point capacitive screen runs an English-language interface, and PLC plus IPC control sequence the cell with forced air cooling for continuous duty.
Specifications
| Model | WM-669 |
|---|---|
| Tube diameter | Φ2.0 mm/Φ6.0 mm |
| Heating length | 6 – 35 mm (optional fixture) |
| Heating temperature | 0 – 380 °C (adjusted by thermostat) |
| Operating cycle | 2.5 seconds |
| Display | 12-inch multi-point capacitive screen |
| System control method | PLC and IPC |
| Input voltage | 220 V AC |
| Frequency | 50/60 Hz |
| Rated power | 1,450 W |
| Air pressure | 5.5/6.5 KPa (listed entry; pressure and unit must be confirmed before installation) |
| Cooling method | Forced air cooling |
| Operating temperature | 0 – 50 °C |
| Storage temperature | -20 – 60 °C |
| Operating humidity | 10% – 90% RH (non-condensing) |
| Anti-interference ability | Interference voltage 1500 Vp-p, pulse period 1 us |
| Duration | 1 minute |
| Dimensions | 740 × 640 × 1,270 mm (L × W × H) |
| Weight | 82 kg |
| HS Code | 8419.89 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Inserting, marking and shrinking collapse three hand operations into one 2.5-second machine cycle
- The legend prints before shrinking; verify the legibility and durability of markings such as 220V-AC on your actual sleeve after the shrink cycle
- Thermostat control from 0 to 380 °C lets you dial heat to the tube material instead of guessing at a fixed nozzle
- 12-inch multi-point capacitive screen with an English-language interface keeps counts, cycle data and settings at the front panel
What it processes
- Voltage and circuit identification sleeves on appliance and power-supply leads
- Wire ends that need an insulated, labeled shrink joint straight off the cutting line
- Panel and switchgear wiring where every conductor carries a printed sleeve marker
Suited for: printed identification sleeves shrunk onto wire ends — tube in the Φ2.0/Φ6.0 mm class, 6–35 mm shrink zones, one marked and shrunk piece every 2.5 seconds. Not suited for: tube above the Φ6.0 mm class, or laser marking with no ink/ribbon — laser mark–insert–shrink on Φ2.0/Φ10 tube (8–45 mm) is the WM-673 (or WM-673B as an alternate build); the Φ2.0/Φ6.5, 8–40 mm laser sibling is the WM-671JG. Insert-and-heat without marking, Φ2.0 to Φ8.0 mm, is the WM-663 heat shrink tube inserting and heating machine, 800–2,500 pcs/h. For shrinking whole harness sections rather than wire ends, the WM-664 infrared harness heat shrink oven takes sections up to Ø100 mm.
Marking layout, sleeve length and shrink finish are easiest to judge on your own parts: send 2–3 meters of your wire with your tube size and legend text, and we run the job on this machine on video before you commit.
The listed air pressure is 5.5/6.5 KPa; confirm the required pressure and unit on the quote before installation. The 2.5-second machine cycle is distinct from sustained accepted output including loading and handling.
Engineering knowledge
Choose and troubleshoot this process
- Heat Shrink Defects: Causes and Corrective ActionsTroubleshoot incomplete recovery, wrinkles, splits, scorching, sleeve movement, trapped air, uneven adhesive flow and heat damage.
- How to Choose Heat Shrink Processing EquipmentChoose heat shrink equipment by sleeve material, recovered dimensions, adhesive requirement, harness geometry, heating method, takt time and validation plan.
WM-669 — common questions
Which tube sizes and shrink zones does the WM-669 cover?
The specification lists tube diameter as Φ2.0 mm/Φ6.0 mm, with a heated zone of 6 – 35 mm chosen through optional fixtures. If your sleeve sits at the edge of that window, send samples and we confirm fit on the actual machine.
How fast is it in production?
The operating cycle is 2.5 seconds per piece — insertion, printing and shrinking included — with forced air cooling keeping the head stable through continuous runs, and PLC plus IPC control sequencing each station.
What can it not do?
It is built for marked sleeves on wire ends — it does not shrink tube above the specified Φ6.0 mm class, and it is not an oven for whole harness bundles or long continuous sleeves. Those jobs live elsewhere in our heat shrink processing range.
How is the WM-669 different from the WM-673?
Marking method, tube class and utilities. This machine ink/print-marks Φ2.0/Φ6.0 mm tube, heats 6–35 mm at 0–380 °C, uses forced air cooling, draws 1,450 W and weighs 82 kg. The WM-673 laser-marks Φ2.0/Φ10 tube (8–45 mm shrink, 0–400 °C), uses forced water cooling, draws 2,500 W and weighs 165 kg. Same 2.5-second cycle; choose this page for ink marking on the smaller class, the WM-673 (or WM-673B) for laser marking without ink or ribbon on the Φ10 class. The WM-671JG is the laser sibling at Φ2.0/Φ6.5 and 8–40 mm.
Related machines in Heat Shrink & Tube Insertion
Bench-Mount Hot Air Heat Shrink Machine with Through-Table Air Outlet
Model WM-667ZM
Crawler Belt Heat Shrink Tunnel Oven for Continuous Wire Sleeve Shrinking
Model WM-666
Double-Sided Far-Infrared Heat Shrink Conveyor Oven with Teflon Mesh Belt
Model WM-670PH