Hot Bar Soldering Machine for FFC, FPC and Connectors, 50–600 °C Pulse Heat WM-721
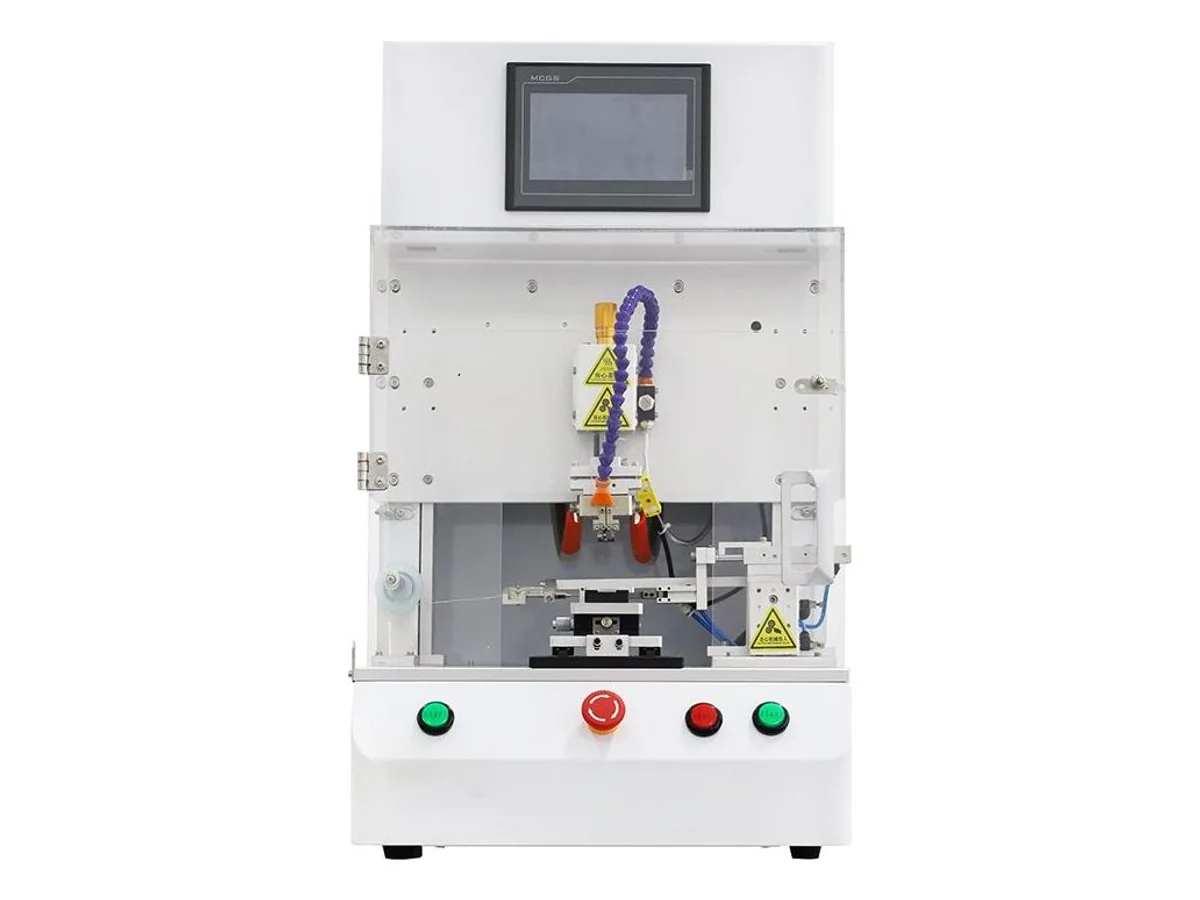
The WM-721 is a hot bar soldering machine — pulse heat, not an iron. A titanium or molybdenum alloy indenter comes down on a screw-driven Z axis, presses the joint against the fixture and heats it through a programmed curve from 50 to 600 °C in up to four stages, holding ±5 °C while the solder wets. Because the heat arrives through pressure, it lands on joints an iron tip cannot reach evenly: FFC and FPC ribbon onto PCB pads, LVDS and ultra-fine coax, and multi-pin connector rows soldered a whole row at a time. ACF and TAB applications require confirmation of the bonding material, thermal profile and tooling on your sample. A cylinder-driven drawing-type feeder delivers the solder wire, the hot head is air cooled between cycles, and the temperature curve, cycle time and piece count run live on an English touch screen. Indenter accuracy is ±0.03 mm over a 50 mm stroke; the machine is 450 × 560 × 850 mm and 80 kg.
Specifications
| Function | Hot bar (pulse heat) soldering — heated indenter presses the joint while it reflows |
|---|---|
| Rated voltage | 220 V, 50 Hz |
| Heating power | 2,000 W |
| Temperature setting range | 50 – 600 °C |
| Temperature accuracy | ±5 °C |
| Heating stage | 1 – 4 stages |
| Hot head cooling method | Air cooling |
| Indenter accuracy | ±0.03 mm |
| Z-axis motion | Screw drive |
| Z-axis travel | 50 mm |
| Automatic solder feed | Drawing type, cylinder driven |
| Dimensions | 450 × 560 × 850 mm (width × length × height) |
| Weight | 80 kg |
| HS Code | 8515.19 (common reference — final classification confirmed by your customs broker) |
| Certification | CE (certificate provided with shipment) |
Key features
- Pulse heat, not a soldering iron — the alloy indenter is cold when it lands, applies pressure first, then heats through the profile and cools before it lifts, so the joint is held flat and aligned the entire time it is molten
- Programmed thermal profile up to 4 heating stages, 50–600 °C at ±5 °C — preheat, reflow and cool-down are separate segments instead of one fixed tip temperature
- Titanium or molybdenum alloy indenters, shaped to your pad row; a wider bar solders every pin of a connector in one press rather than pin by pin
- Live temperature curve on the English touch screen — the plotted profile, cycle time, program name and piece counter are all on one Running Monitor screen, so a drifting joint is visible before it becomes a batch of rejects
- Screw-driven Z axis with ±0.03 mm indenter accuracy and 50 mm travel, motor pressurised — bond force and landing position repeat cycle to cycle instead of depending on the operator's hand
- Forced-air cooling on the hot head brings the indenter back down between cycles, which is what makes a repeatable curve possible at all
- Cylinder-driven drawing-type solder wire feed with a Send solder command on the screen — solder is delivered and withdrawn per cycle, not left sitting on the tip
- Power adaptive adjustment and whole-machine leakage protection; the work area sits behind a clear guard with the loading platform in front
- Free sample test — send us your ribbon, connector or lead assembly, we run it on this machine and send you the video with the actual curve before you order
What it processes
- FFC and FPC ribbon soldered onto PCB pads, and flex-to-board joints in display and camera modules
- LVDS harnesses and ultra-fine coaxial cable terminated onto boards and connectors
- ACF and TAB bonding on high-density interconnects, with the material, process and tooling confirmed by a sample trial
- Multi-pin connector rows where every pin is soldered in a single press
- Discrete wire leads onto PCB pads where flatness and alignment matter more than speed
Suited for: joints that have to be held flat and aligned while the solder is molten — FFC and FPC ribbon onto PCB pads, LVDS and micro-coax terminations, and multi-pin connector rows soldered a whole row per press, on a programmed 50–600 °C profile. ACF and TAB work requires a material-specific bonding process and tooling confirmed on a sample; ACF adhesive bonding is separate from solder reflow.
For solder-free metal joining: choose a welding process matched to the joint rather than this soldering configuration. For stranded copper splices from 0.75 to 20 mm², use the WM-711 ultrasonic wire welding machine; for wire onto terminals up to 30 mm², the WM-713 ultrasonic terminal welding machine does it in 0.5–2 s per weld with no solder at all. If the job is a cable assembly soldered with an iron tip and automatic feed rather than a pressed bar — USB and similar leads, with stripping on the same machine — the WM-712 semi-automatic USB cable soldering machine runs 300–600 pieces per hour. If what you actually want is stripped wire ends dipped and pre-tinned in bulk rather than a part bonded to a board, that is a different machine class — see the wire twisting and tinning machines. If the connection design permits crimping, compare the tooling, cycle and joint requirements using our terminal crimping machines.
Indenters and part nests are made to order for each job. If your part is unusual — a very long pad row, a stacked flex, or a board that needs preheat from below — describe it in your inquiry and we will confirm what this platform can be tooled for before quoting.
Engineering knowledge
Choose and troubleshoot this process
- Wire Soldering Defects: Causes and Corrective ActionsTroubleshoot non-wetting, excessive solder wicking, bridging, burnt insulation, unstable tinning depth, residue and contaminated wire solder joints.
- How to Choose an Ultrasonic Wire Welding MachineChoose ultrasonic wire welding equipment by conductor material, gathered cross-section, splice geometry, weld power, tooling, recipe control and acceptance testing.
- How to Choose a Wire Twisting and Tinning MachineChoose wire twisting and tinning equipment by conductor construction, strip condition, tinning specification, flux control, finished-end geometry and automation level.
WM-721 — common questions
How is hot bar soldering different from iron soldering or ultrasonic welding?
These are different joining processes. Iron soldering applies heat locally with an iron tip and solder; fixtures can hold the workpiece. Ultrasonic metal welding uses vibration, including 20 kHz systems, to join suitable metal interfaces without solder, with application-specific tooling. Hot bar soldering holds the parts under pressure while the thermode follows a heating and cooling profile so pre-applied solder reflows and solidifies before release. This supports alignment of FFC ribbon and fine-pitch pads; the actual joint quality is verified on your sample.
What does the machine need on the parts — solder paste, or does it feed solder wire?
For soldered flex-to-board joints, pre-tinned pads or solder paste can be prepared before loading and reflowed under the heated indenter. For suitable wire-to-pad and connector jobs, the cylinder-driven drawing-type feeder supplies solder wire. ACF uses conductive adhesive film and a material-specific bonding profile; it must not be treated as solder reflow. For ACF or TAB work, send the material and joint drawing so we can confirm the process, tooling and machine configuration on a sample.
How much bond force does the indenter apply, and how many pieces per hour will it do?
Bond force and throughput are confirmed on the quote after a trial. Both depend on the part and configured process — force is set by pad count and how much the flex can take, and cycle time is set by the profile your solder alloy needs plus operator load and unload. Send us a sample; we will run it, record the curve and the measured cycle time, and send you the video.
Do I need custom tooling for my part?
Yes, two pieces. The indenter is ground to the width and profile of your pad row, and the nest that holds the part is built to your connector or board. Both are made to your drawing or to a physical sample. Send us the part and the pad layout with your inquiry and we will quote the machine and the tooling together.
What temperature should I run?
The setting range is 50–600 °C in 1–4 stages, held to ±5 °C, so the curve is set by your solder alloy rather than by the machine's limits — a lead-free SAC profile and a low-temperature bismuth profile are both inside the range. The screen plots the actual curve against the setpoint every cycle, so the profile you validate on a sample is the one you can prove you are running in production.
What supply does it need?
220 V, 50 Hz single phase, with the heater rated 2,000 W. Compressed air is required for the solder feed cylinder and the hot head air cooling; the required air pressure is confirmed on the quote against your site supply before shipping.
Related machines in Tinning, Soldering & Welding
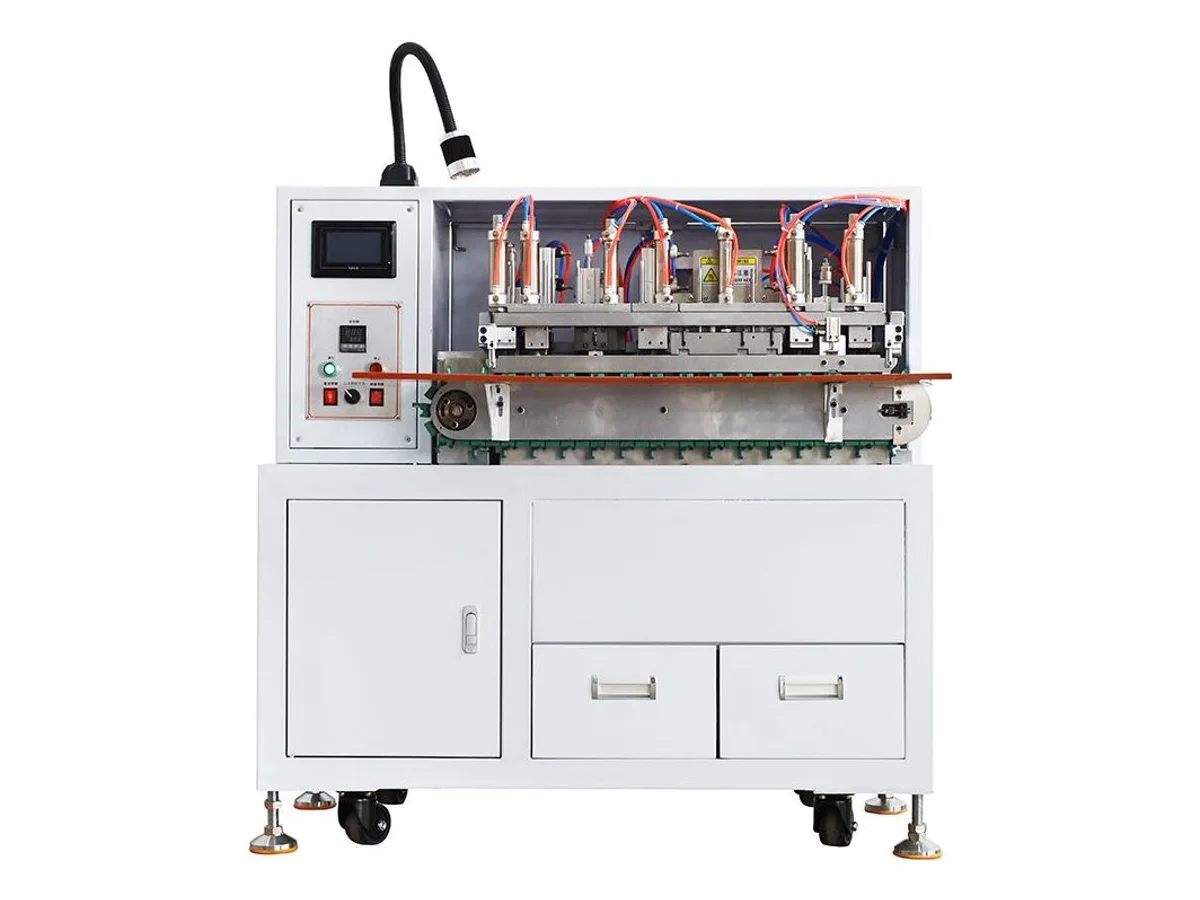
Automatic 3-Core Cable Cutting Stripping Twisting and Tinning Machine
Model WM-4710T
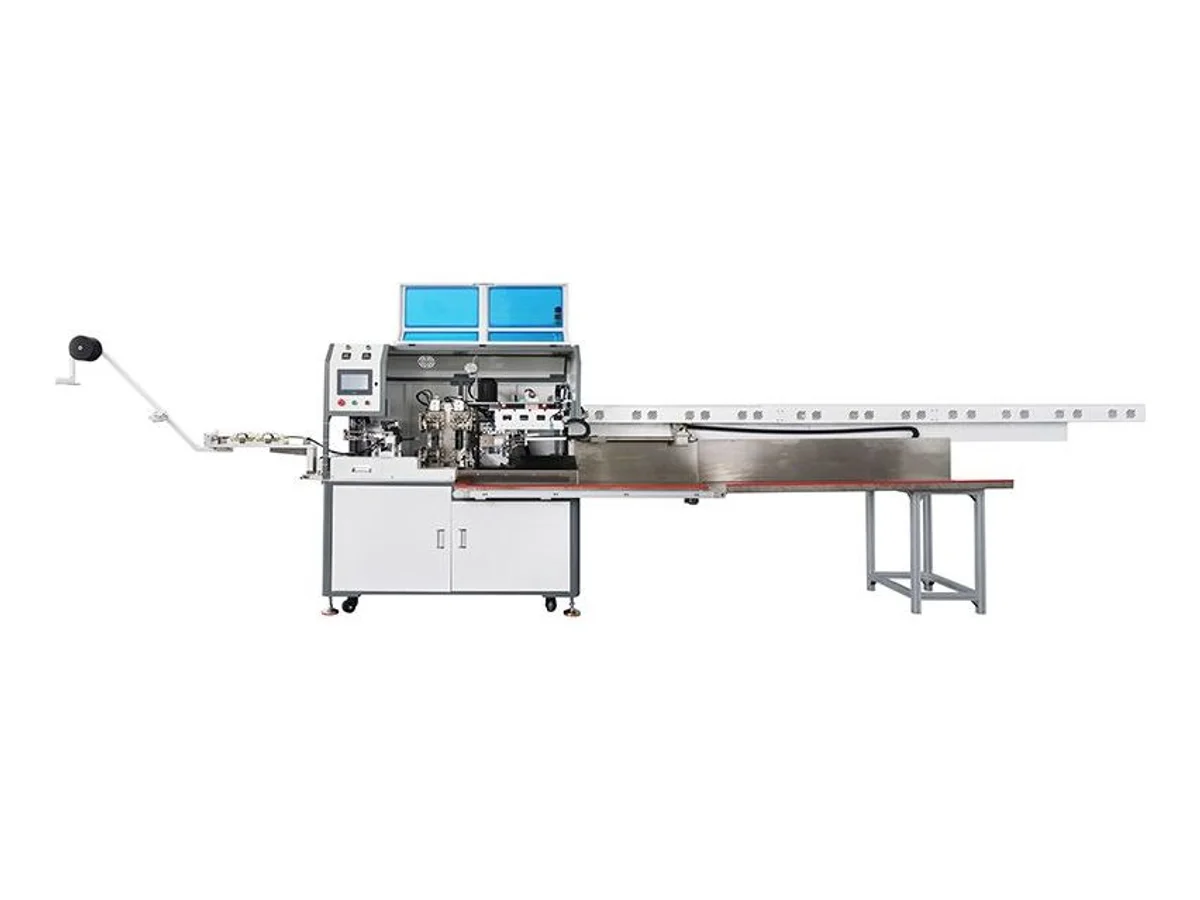
Automatic Multicore Cable Cutting Stripping and Two-End Tinning Machine
Model WM-4706S
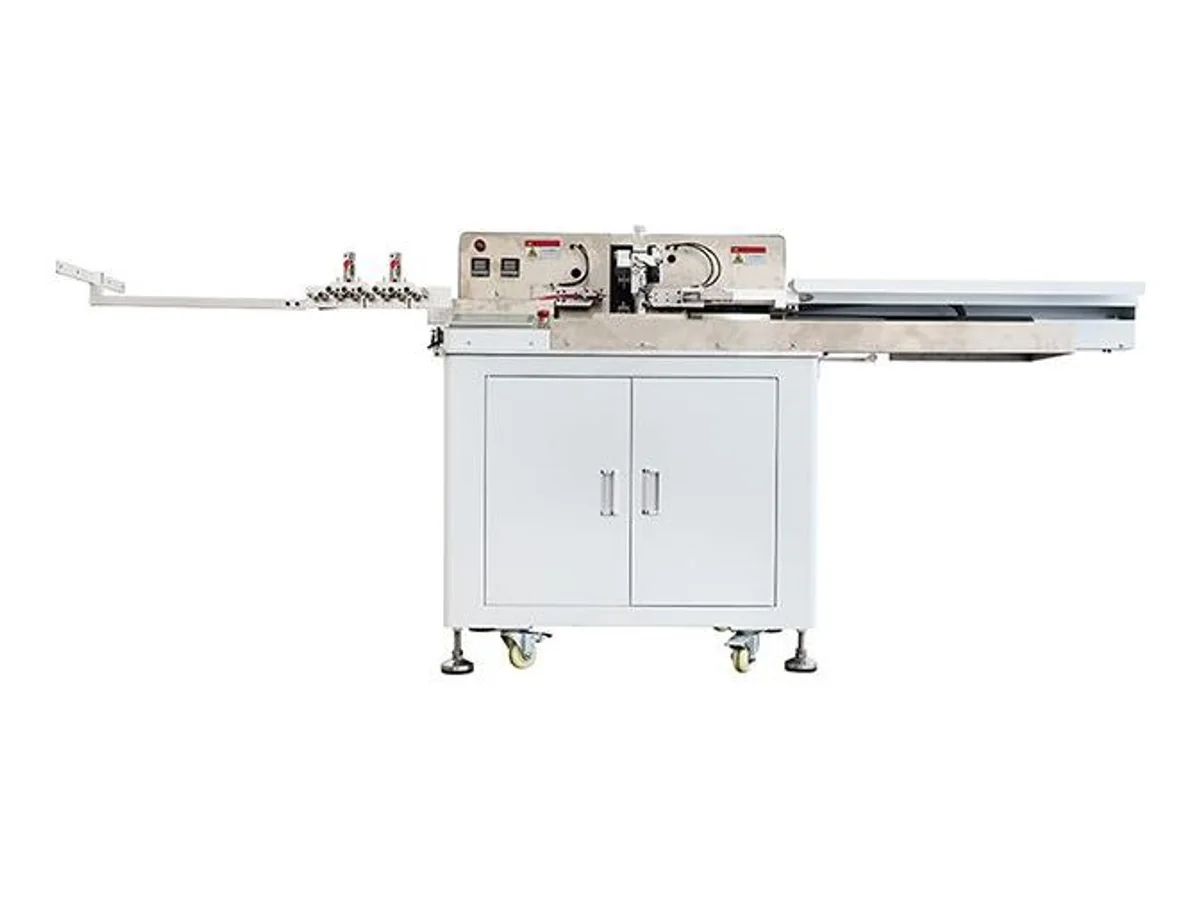
Automatic Multiple-Wire Stripping Twisting and Tinning Machine for 18–28 AWG
Model WM-4706W